Featured CE Certified Titanium Fasteners & Hardware
Precision engineered Ti-6Al-4V Grade 5 titanium bolts, caliper studs, and specialty motorcycle components manufactured under ISO 9001 and CE directives. Fully customizable dimensions, threads, and surface anodizing options.
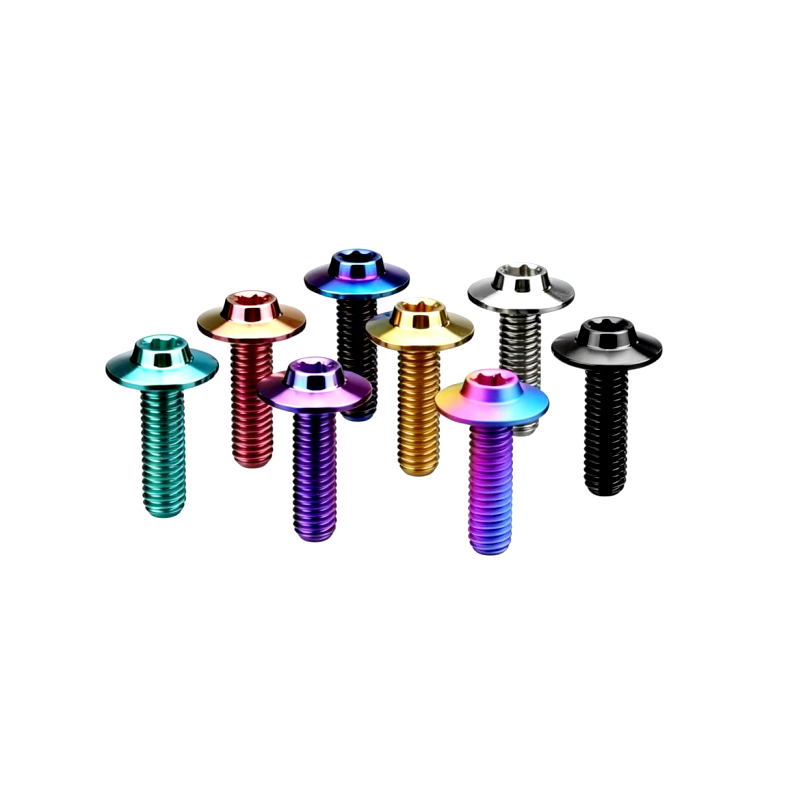
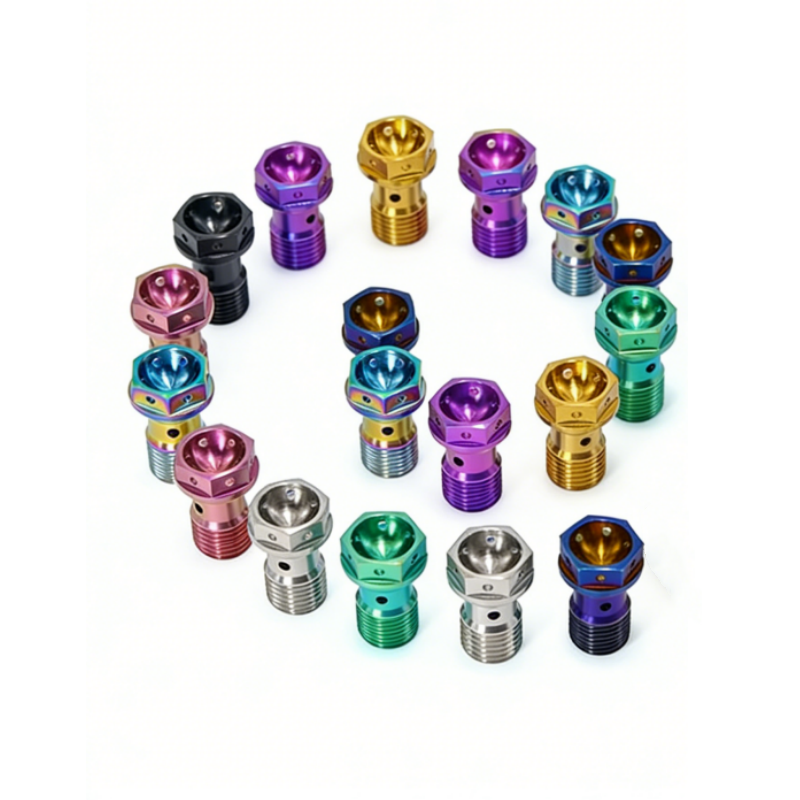
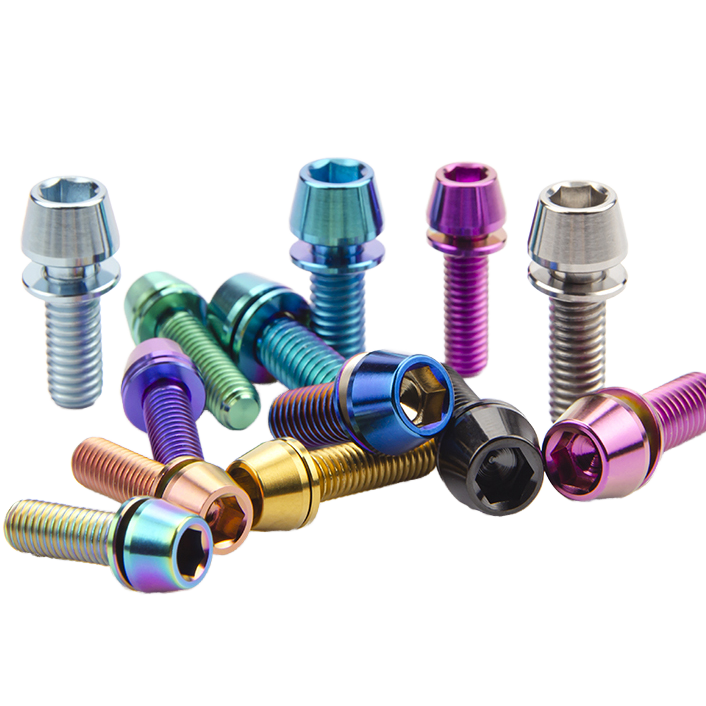
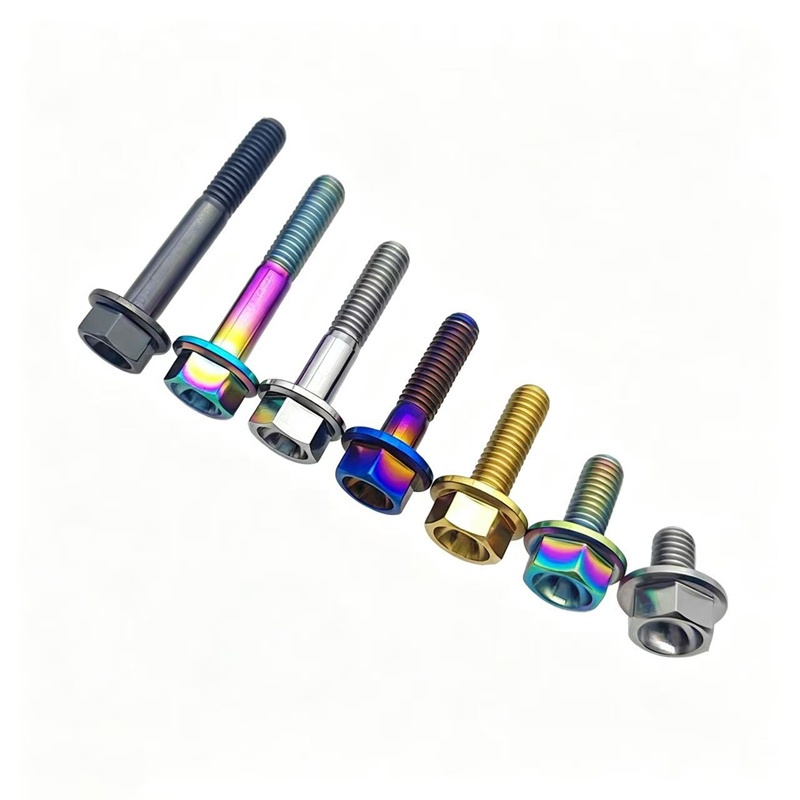
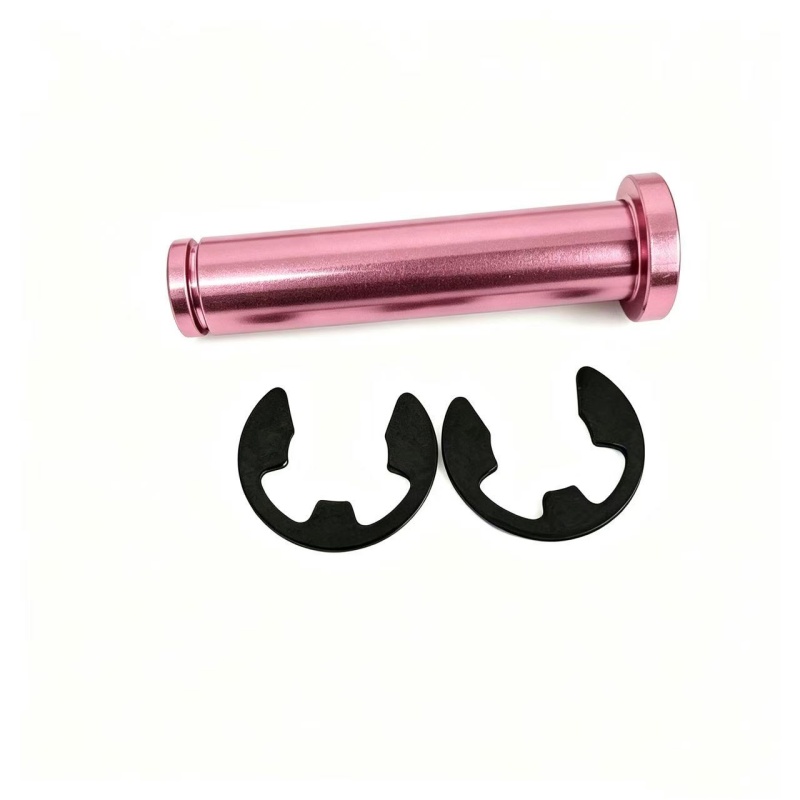
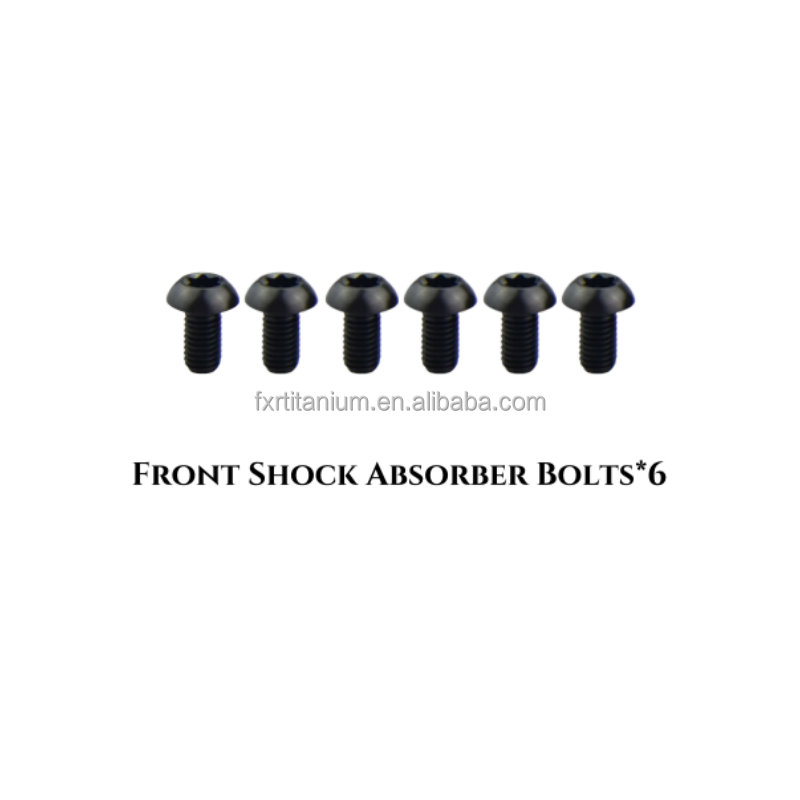
Metallurgical Properties & CE Compliance for Industrial Titanium Fastener Assortments
A comprehensive analysis of Ti-6Al-4V structural mechanics, thread-rolling grain alignment, fatigue behavior, and conformity verification under EU Machinery Directive 2006/42/EC and EN 10204 3.1 certification.
In high-stress mechanical assemblies, replacing carbon steel or austenitic stainless steel fasteners with titanium assortments requires strict adherence to international metallurgical standards. Our manufacturing infrastructure leverages aerospace-grade Ti-6Al-4V Grade 5 (UNS R56400 / Werkstoff 3.7165), delivering a specific strength (strength-to-density ratio) far exceeding conventional structural metals. Unlike Commercially Pure (CP) titanium grades (Grades 1 to 4) which offer excellent chemical passivity but lack sufficient tensile performance for critical torque-bearing interfaces, Grade 5 delivers a nominal yield strength exceeding 828 MPa and an ultimate tensile threshold reaching up to 1,000 MPa after specialized cold-working and stabilization treatment.
A primary failure mode in substandard commercial titanium fasteners is fatigue-induced shear cracking at the head-to-shank fillet radius and along the thread runout. Under CE compliance mandates (EN 14399 for high-strength structural bolting and EN 15048 for non-preloaded assemblies), our precision forging line applies CNC cold-heading followed by thread-rolling technology rather than chip-removing machining. Thread rolling preserves continuous metallurgical grain flow along the pitch flanks, generating beneficial compressive residual stresses on the roots that increase cyclic fatigue life by more than 300% to 450% compared to cut threads.
| Material Designation | Yield Strength (Rp0.2 MPa) | Tensile Strength (Rm MPa) | Density (g/cm³) | Modulus of Elasticity (GPa) | Corrosion Resistance (C1 to CX) |
|---|---|---|---|---|---|
| Ti-6Al-4V Grade 5 (Our Standard) | ≥ 828 – 910 | ≥ 895 – 1050 | 4.43 | 114 | Immune in Salt Spray (CX/Industrial Marine) |
| Commercial Pure Ti Grade 2 | ≥ 275 – 350 | ≥ 345 – 480 | 4.51 | 103 | Excellent Atmospheric Passivation |
| High-Tensile Alloy Steel 10.9 | ≥ 940 | 1000 – 1200 | 7.85 | 210 | Susceptible to Rust; Requires Electroplate |
| Alloy Steel 12.9 | ≥ 1100 | 1220 – 1400 | 7.85 | 210 | High Risk of Hydrogen Embrittlement |
| Austenitic Stainless Steel A2-70 (304) | ≥ 450 | 700 – 850 | 7.90 | 193 | Chloride Pitting Susceptible (Pitting >50°C) |
Furthermore, CE certification for fasteners demands absolute verification of raw materials and test regimens. Each procurement batch shipped from our Baoji facility is accompanied by an EN 10204 Type 3.1 Inspection Certificate derived from inductive optical spectrometry, direct wet chemical assays, and optical eddy-current flaw detection. Microstructural evaluations ensure an equiaxed alpha-beta microstructure without brittle interstitial contamination (oxygen < 0.20%, hydrogen < 0.015%, nitrogen < 0.05%, carbon < 0.08%, iron < 0.40%). This metallurgical purity eliminates the risk of sub-surface micro-void propagation under dynamic vibrational frequencies common in high-performance motorsports, maritime propulsion, and robotic arm drive linkages.
Future Sourcing & Procurement Trends for Titanium Screws Assortments
Critical strategic shifts influencing global supply chain managers, defense contractors, and aftermarket racing teams sourcing CE-certified titanium hardware over the next five years.
Kit Modularization & Direct-to-Cell Delivery
OEM procurement is shifting from bulk commodity part-numbers toward specialized, pre-packaged modular assortments tailored to specific assemblies (e.g., complete front-fork hardware kits, brake caliper service modules, or engine bay dress-up packs). This drastically shortens factory assembly times, lowers stock handling costs, and eliminates line-side fastener misplacement.
Digital Passports & Laser Part Serialization
With escalating regulatory audits under European and North American machinery safety frameworks, Tier-1 buyers demand direct-part laser engraving featuring micro-DataMatrix codes. These codes link directly to batch-specific melt records, dimensional CMM inspection reports, and CE Declaration of Conformity documents stored within cloud-accessible supplier databases.
Electric Powertrain Weight Criticality
As battery pack weights continue to compromise the handling dynamics of electric motorcycles, hypercars, and eVTOL urban air mobility craft, rotating and unsprung hardware is under aggressive scrutiny. Swapping out Grade 10.9 steel wheel studs, rotor bolts, and suspension pins for Grade 5 titanium assortments removes critical rotational inertia without sacrificing joint clamp pre-load.
Lifecycle TCO Supplanting Initial Purchase Price
Procurement directors are calculating Total Cost of Ownership (TCO) across harsh operating environments. In maritime, subsea drilling, and aggressive chemical processing plants, stainless steel and plated fasteners suffer galvanic and crevice corrosion requiring premature replacement. Titanium hardware assortments offer non-degrading lifespans, eliminating recurrent maintenance turnarounds.
Elimination of Toxic Cadmium & Chrome Treatments
Stricter enforcement of EU RoHS, REACH, and environmental ESG metrics has accelerated the obsolescence of electroplated hexavalent chromium and cadmium coatings on steel hardware. Titanium naturally creates an adherent, self-healing oxide passivation layer (TiO₂), achieving unmatched durability through completely non-toxic electrochemical anodizing or vacuum PVD sputtering.
Direct Procurement from Certified Regional Hubs
To bypass multi-tier broker markups and mitigate logistics bottlenecks, tier-one purchasing officers are partnering directly with integrated manufacturing centers situated in high-density titanium clusters like Baoji, China ("Titanium Valley"). This ensures stable titanium sponge feedstock allocations, competitive raw material costs, and rapid sample turnaround times.
Technological & Development Trends in Titanium Fastener Engineering
Discover how innovations in multi-axis Swiss CNC turning, high-velocity warm heading, and micro-arc oxidation are revolutionizing titanium fastener mechanical integrity.
Warm Heading & Net-Shape Forging
Traditional cold-heading of titanium alloy is constrained by rapid work hardening and head shearing. Modern production utilizes induction-assisted precision warm-heading (650°C–750°C) to reform hexagonal flange, umbrella torx, and socket-cap heads without fracturing, optimizing structural grain density.
Sub-Micron Thread Profile Grinding
To support ISO metric Class 4h/6h and aerospace UNJ/UNJF tight thread specifications, high-precision automated cylindrical CNC thread roll-die systems eliminate thread pitch runout, providing smooth engagement without binding or micro-jamming upon repetitive field installation.
Tribological PVD Hard Coatings
Physical Vapor Deposition (PVD) has revolutionized surface engineering. Nano-structured coatings such as Diamond-Like Carbon (DLC), Titanium Nitride (TiN), and AlTiN generate Vickers micro-hardness exceeding 2,500 HV, drastically cutting friction coefficients ($\mu \approx 0.10$) and eliminating mechanical thread galling.
Laser-Guided Optical Sorting
Quality assurance on CE certified assortment boxes has migrated away from manual go/no-go gauges toward multi-camera 360-degree glass plate automated optical sorting machines. Fasteners are measured across 18 critical points in under 40 milliseconds, reaching zero-defect PPM benchmarks.
Direct Production from China's "Titanium Valley"
Headquartered in Baoji, Shaanxi Province, our manufacturing operation brings together localized raw billet procurement, precision CNC Swiss-lathe processing, and specialized surface finishing under an integrated ISO 9001 certified roof.
Since 2015, we have provided Tier-1 OEM/ODM export solutions across North America, Europe, Southeast Asia, and Oceania. From miniature M2 fasteners for competitive RC engineering to robust M26 magnetic oil drain plugs and customized motocross suspension linkage hardware, we guarantee full chemical, dimensional, and metallurgical compliance with international standards.
10+ Years of Focused OEM/ODM Expertise
Specialized R&D team turning complex 2D/3D customer engineering prints (STEP, IGES, DXF) into finished Grade 5 titanium fasteners within 10 to 15 days.
Comprehensive Thread Sizing Spectrum: M2 to M26
High-volume manufacturing of standard coarse, metric fine (M10×1.25, M12×1.25, M14×1.5), and unified imperial threads (UNC, UNF) in exact adherence to DIN, ISO, and ASTM norms.
Factory-Direct Quality Verification & Traceability
Equipped with Mitutoyo CMM, optical optical comparator projectors, salt-spray testing chambers, and Rockwell hardness testers with real-time EN 10204 3.1 documentation.
Flexible Ordering MOQs & Rapid Dispatch
From prototype pilot runs of 10 to 50 pieces for race teams to container shipments of 500,000 pieces for automotive distributors. Average inquiry response within 2 hours.
Frequently Asked Questions by Industrial Sourcing Directors
Everything you need to know regarding metallurgy, CE compliance, thread galling mitigation, surface finish durability, and custom packaging logistics.
Request Engineering Pricing & CE Documentation Today
Whether you require standard race-spec hardware assortments, private-label packaging boxes, or specialized CNC components manufactured to custom CAD drawings, our technical engineers provide full quotations and feasibility feedback within 2 hours.