Precision Titanium Hardware & Valve Components
Explore our industrial-grade, CNC-machined Grade 5 titanium fasteners, engine valve accessories, and custom automotive hardware built for extreme thermal and mechanical environments.
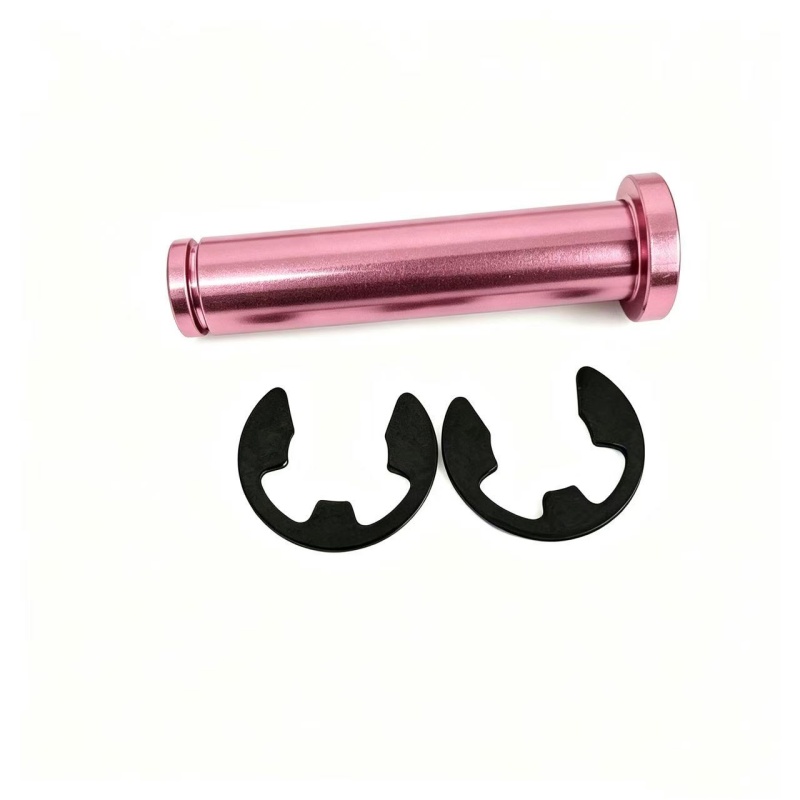
Factory Customized Grade5 Colorful M10*40mm Titanium Pin Bolt
High-tensile Grade 5 titanium pin bolt tailored for motocross, Honda, Yamaha, Talaria, and Segway applications.
View Details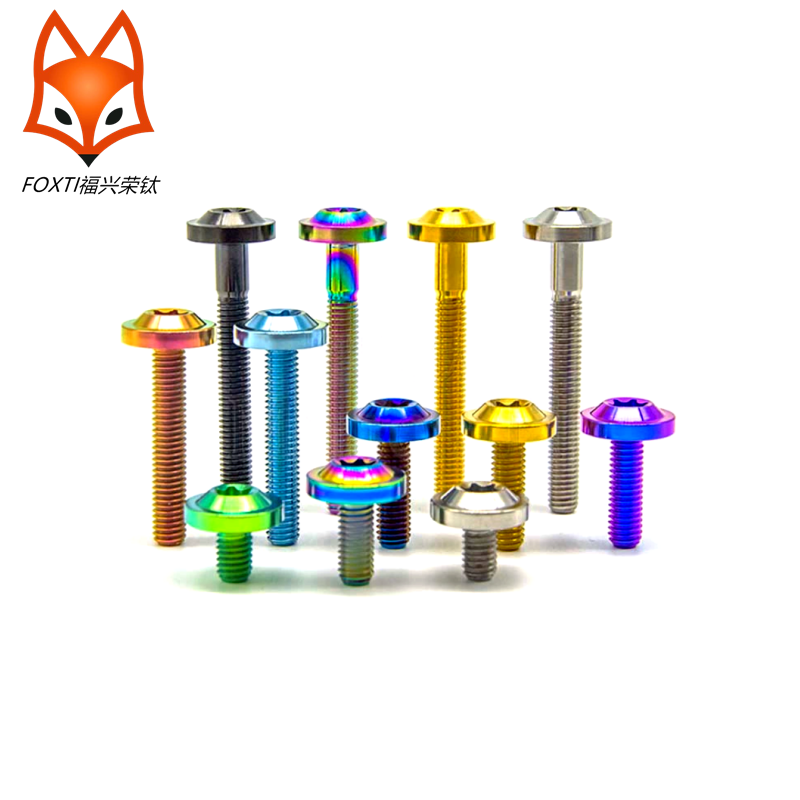
Grade 5 Titanium Alloy Disc Torx Head Anodized PVD Full Set
Complete M8/M6/M10 Torx head bolt sets featuring anti-corrosive PVD and anodized surface treatments.
View Details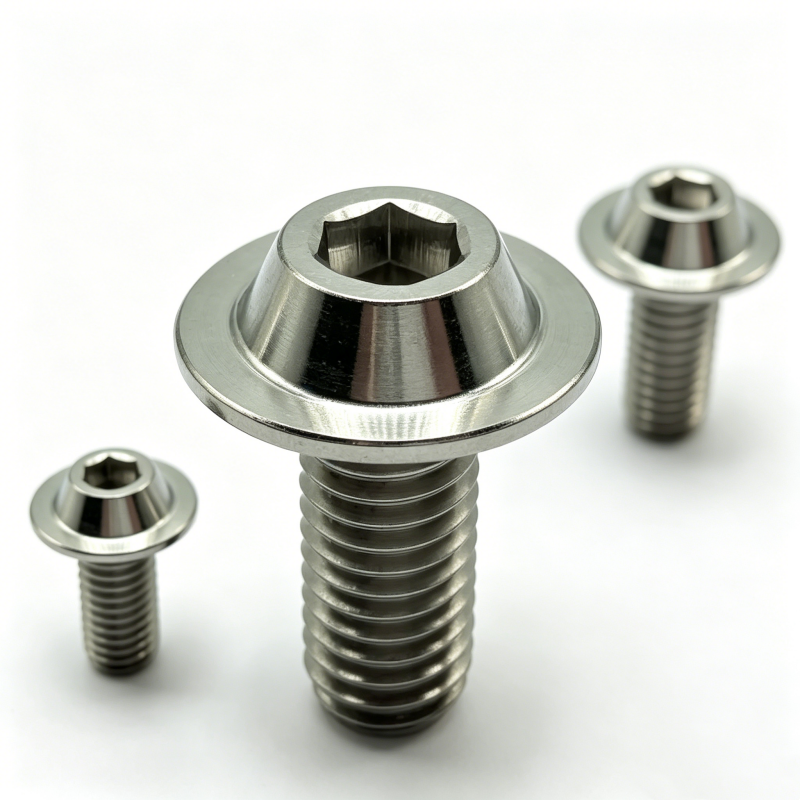
Wholesale GR5 Titanium Alloy Screws M4-M10 UFO Head
Ultra-lightweight UFO head design with precision CNC hex socket, engineered for racing and aerospace assemblies.
View Details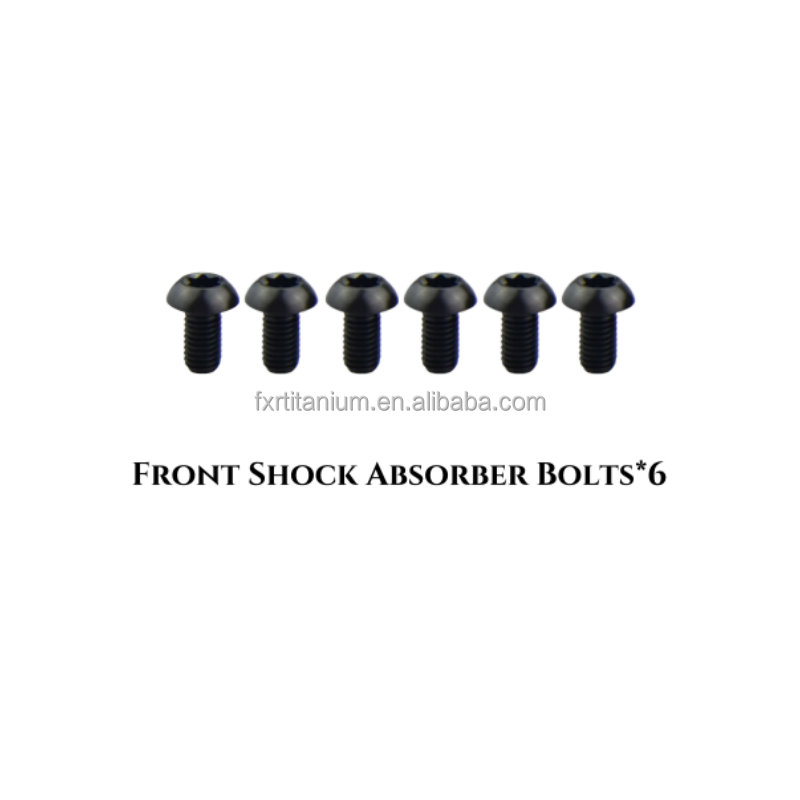
Titanium Alloy Colorful Front Shock Absorber Bolts 6PCS
Class 10.9 & 12.9 strength-equivalent titanium shock absorber bolts custom processed for Surron Ultra Bee.
View Details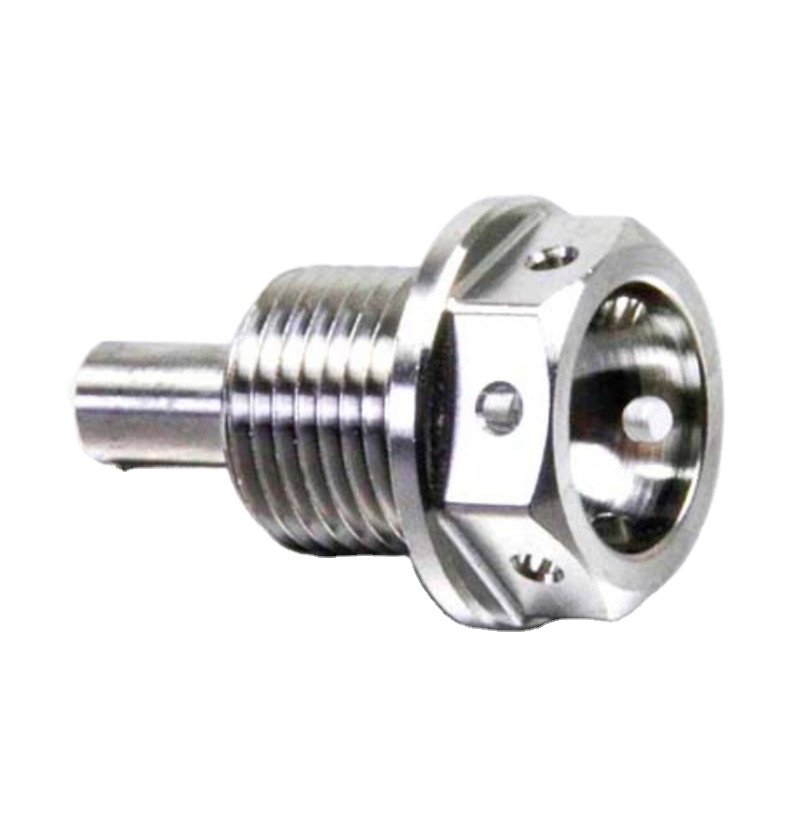
Custom M12-M26 Automotive Magnetic Titanium Drain Plug Bolt
High-nd magnetic titanium sump plugs engineered to capture ferrous particles and withstand thermal cycle fatigue.
View Details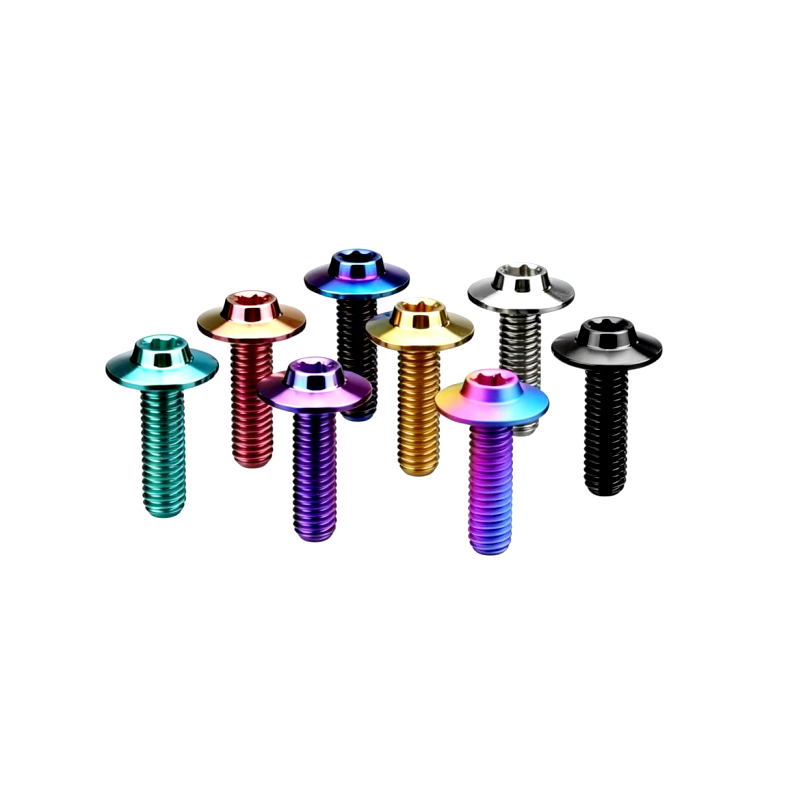
Grade 5 Colorful M6 Titanium Umbrella Torx Head Bolts
Available in lengths from 6mm to 50mm, delivering superior clamping force and vibrant color durability.
View Details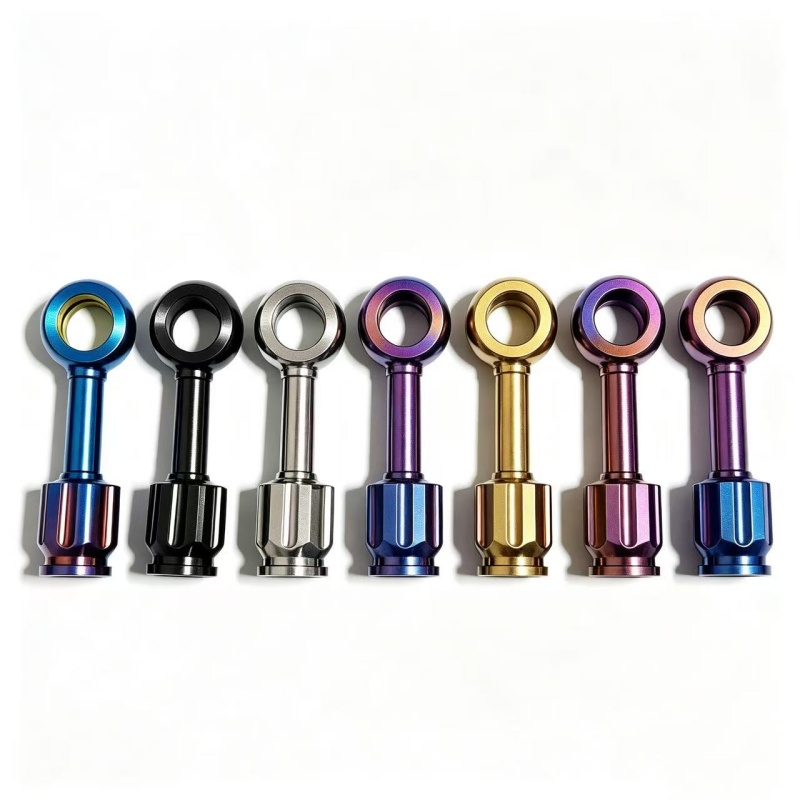
Titanium Alloy Crimp Connector AN3 Brake Hose Line
Race-grade AN3 titanium crimp connector for high-pressure hydraulic lines and brake fluid management.
View Details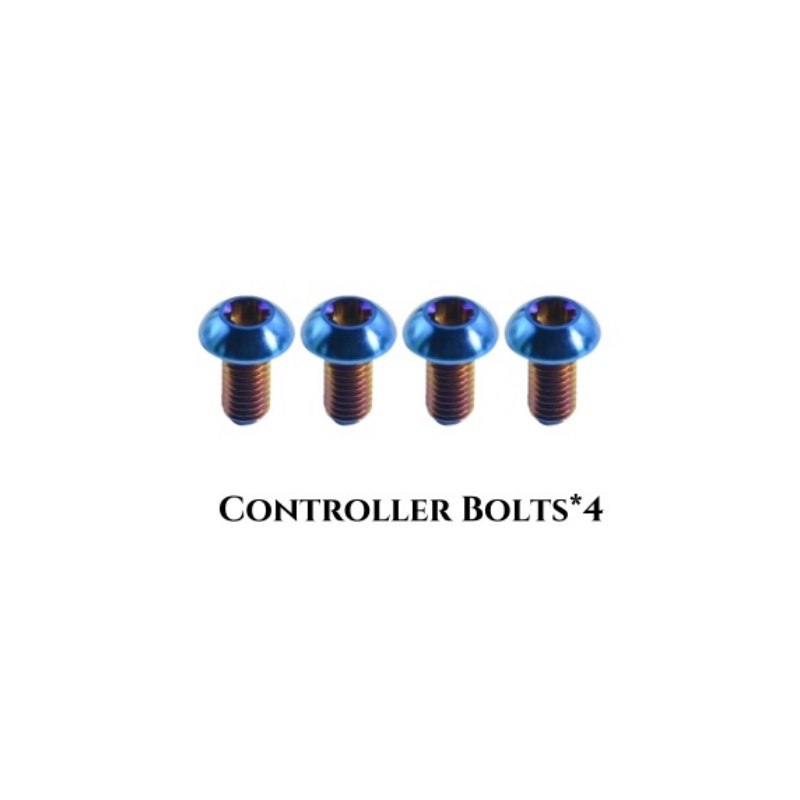
Vacuum Coated Titanium Controller & Hardware Bolts
High-durability PVD vacuum coated GR5 titanium hardware featuring precision-cut threads and zero rust properties.
View DetailsWhite Paper: Engineering Standards & Metallurgy of Titanium Valve Stems
In modern high-rpm internal combustion engines, high-performance motorsport powerplants, and lightweight wheel valve system architectures, the mechanical load placed upon valve stems and associated fluid control hardware demands materials that surpass traditional stainless steels and brass. Titanium valve stems—specifically those fabricated from Grade 5 Titanium Alloy (Ti-6Al-4V)—represent the pinnacle of strength-to-weight optimization, thermal endurance, and dynamic sealing integrity.
As engine speeds increase beyond 9,000 RPM, reciprocating mass within the valve train becomes the primary bottleneck to power efficiency and valve float prevention. By transitioning from conventional Inconel 751 or 21-4N austenitic steel to Grade 5 titanium, automotive and motorsport engineers achieve an immediate 40% to 45% reduction in valve train inertial weight. This reduction permits stiffer valve springs with lower spring rates, mitigating parasitic friction loss and extending component fatigue life across millions of stress cycles.
Comparative Metallurgy & Material Mechanics Table
To assist procurement managers, mechanical engineers, and quality assurance directors in making informed sourcing decisions, the following data matrix highlights the physical and mechanical properties of raw materials used in valve stems and performance hardware manufacturing:
| Material Grade | Density (g/cm³) | Tensile Strength (MPa) | Yield Strength (MPa) | Max Temp Limit (°C) | Corrosion Resistance |
|---|---|---|---|---|---|
| GR5 Ti-6Al-4V (Annealed) | 4.43 | 895 - 1000 | 828 - 910 | 400°C | Outstanding (Passivated Oxide) |
| GR23 Ti-6Al-4V ELI | 4.43 | 860 - 930 | 795 - 875 | 420°C | Superior (Low Interstitial) |
| Stainless Steel 316L | 8.00 | 485 - 620 | 170 - 290 | 300°C | Moderate to High |
| Inconel 751 (Exhaust Valve) | 8.22 | 1100 - 1200 | 750 - 850 | 815°C | High Thermal Resistance |
| C36000 Brass (Legacy Stems) | 8.50 | 380 - 450 | 150 - 230 | 150°C | Poor in Acidic/Saline Air |
Future Sourcing Trends for Titanium Valve Stems & Fasteners (2025–2030)
Global automotive original equipment manufacturers (OEMs) and tier-1 aftermarket distributors are undergoing structural shifts in how titanium components are specified, manufactured, and procured. Understanding these macro trends is vital for procurement executives seeking sustainable cost structures and technical compliance:
- Transition to Physical Vapor Deposition (PVD) Hard Coatings: While traditional anodizing provides aesthetic color variations, future high-performance engine applications require specialized thin-film coatings such as Diamond-Like Carbon (DLC), Titanium Nitride (TiN), and Titanium Aluminum Nitride (TiAlN). These coatings reduce stem friction coefficients down to μ = 0.1, eliminating wear against valve guides without compromising dimensional runout tolerances (< 0.005mm).
- Near-Net-Shape Hot Forging & Multi-Axis Swiss CNC Lathe Integration: To counteract raw material cost fluctuations in titanium sponge, leading Chinese factories are moving away from solid bar stock subtractive machining alone. Instead, micro-grain hot upset forging combined with 5-axis precision CNC finishing maximizes raw material utilization, drastically lowering unit production costs while aligning structural grain lines along the valve stem axis.
- Automated 100% Optical & Eddy Current Flaw Inspection: Quality protocols are moving from sample batch testing to fully automated inline optical sorting and ultrasonic flaw detection. This ensures zero micro-porosity, zero thread pitch deformation, and zero axial runout in critical aerospace and racing applications.
- Supply Chain Consolidation in Baoji ("Titanium Valley"): Global buyers are increasingly bypassing third-party trading intermediaries in favor of direct factory partnerships located in primary industrial clusters like Baoji, Shaanxi. Direct factory engagement grants buyers end-to-end material certification (DIN EN 10204 3.1) and lower minimum order quantities (MOQs).
Key Technological Innovations Shaping Titanium Hardware Manufacturing
The manufacture of high-reliability titanium valve stems and threaded fasteners requires strict process control to overcome titanium’s natural propensity toward work hardening and galling. At Verqo Titanium Products Co., Ltd., state-of-the-art production methods solve these historic engineering challenges:
1. Thread Rolling vs. Thread Cutting
Cut threads act as notch stress concentrators, severing the natural longitudinal grain flow of titanium bar stock and diminishing fatigue resistance under high vibration. Verqo utilizes high-precision cold and warm thread rolling machinery. Thread rolling burnishes the root profile, induces compressive residual surface stresses, and increases thread fatigue strength by up to 300% compared to cut threads.
2. Centerless Super-Finishing Grinding
For engine valve stems and airtight tire valve interfaces, surface roughness directly dictates dynamic seal longevity. Utilizing multi-pass centerless grinding machines, stem outer diameters are held within micro-tolerances (+0 / -0.005mm) with surface finish parameters reaching Ra 0.2μm, preventing blow-by and oil leakage into combustion chambers.
Why Partner with Verqo Titanium Products Co., Ltd.?
Headquartered in Baoji, China—the world-renowned hub of titanium metallurgy—Verqo integrates raw material procurement, precision CNC machining, custom surface finishing, and international logistics under one stringent quality management system.
100% Certified GR5 Titanium
We source certified titanium sponge and forged bars tested for chemical composition, tensile yield strength, and micro-structure density. MTRs (Mill Test Reports per DIN EN 10204 3.1) accompany every shipment.
Full OEM/ODM Capabilities
From CAD drawing review and rapid prototyping (sample lead times within 7-10 days) to mass CNC production from M2 up to M26 thread sizes, we customize head shapes, thread pitches, and specialized valve profiles.
Advanced Surface Finishes
Choose from polished raw metallic finish, anodic oxidation (Gold, Blue, Purple, Green, Rainbow), and PVD Vacuum Coating (DLC, Burnt Blue, Titanium Black) with exceptional adhesion and anti-scratch properties.
Strict Quality Control System
Our workshop is equipped with 2D optical projectors, Rockwell hardness testers, spectral material analyzers, thread ring/plug gauges, and dynamic balancing equipment to maintain 100% zero-defect shipments.
Flexible MOQs & Fast Shipping
We support growing brands and custom tuning shops with flexible minimum order quantities starting from 10 to 100 pieces for standard stock items, backed by express air and ocean freight logistics.
Dedicated Engineering Support
Our bilingual sales engineering team responds within 2 hours, offering expert technical consultation on thread pitch selections, torque specifications, galling prevention, and assembly lubricants.
Frequently Asked Questions (B2B Procurement FAQ)
Find authoritative answers regarding material selection, custom manufacturing, surface finishes, quality control, and commercial purchasing terms.