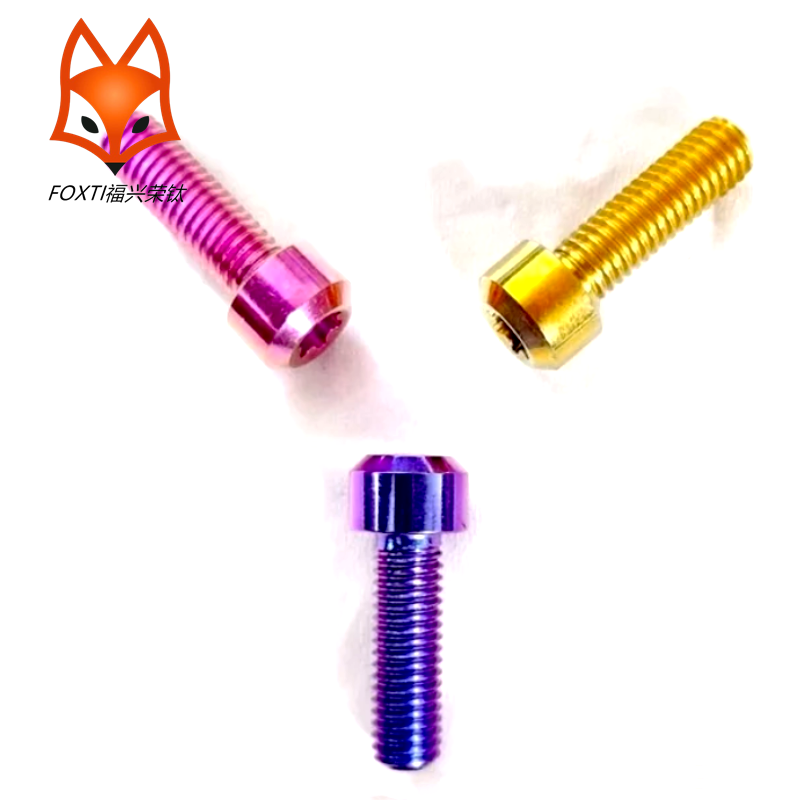
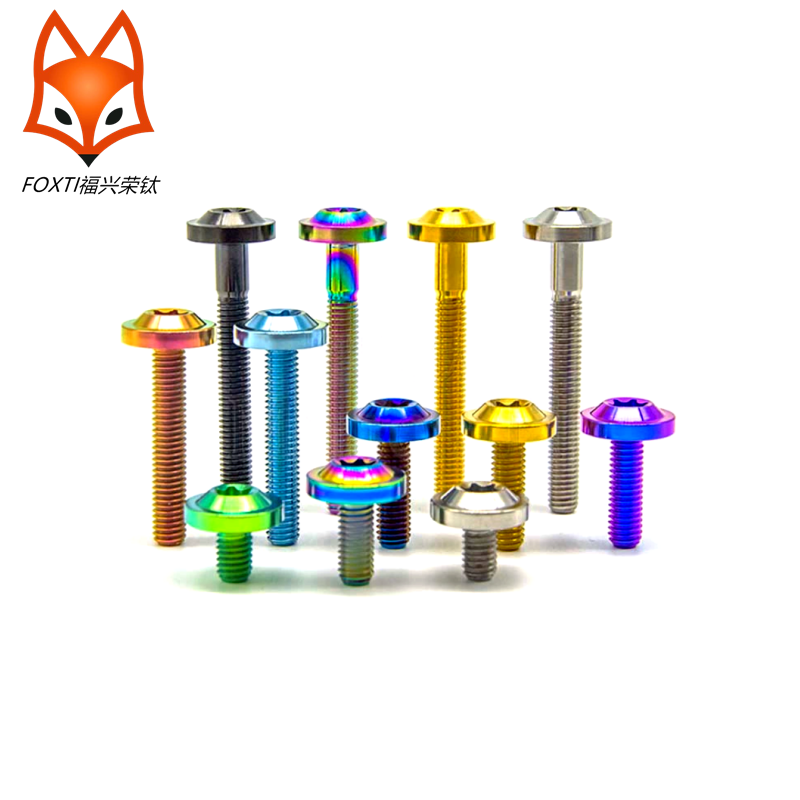
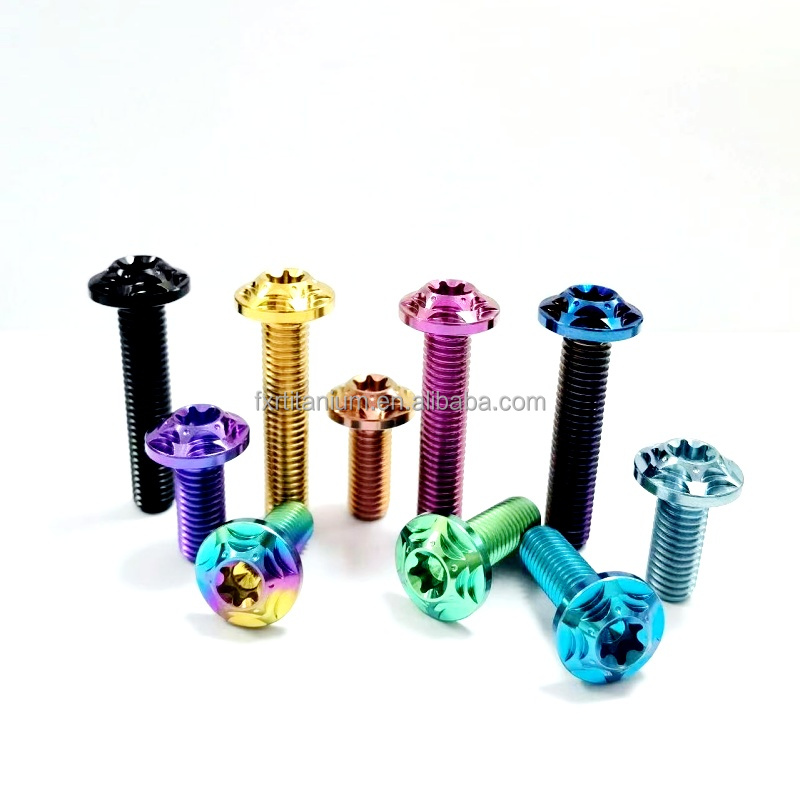
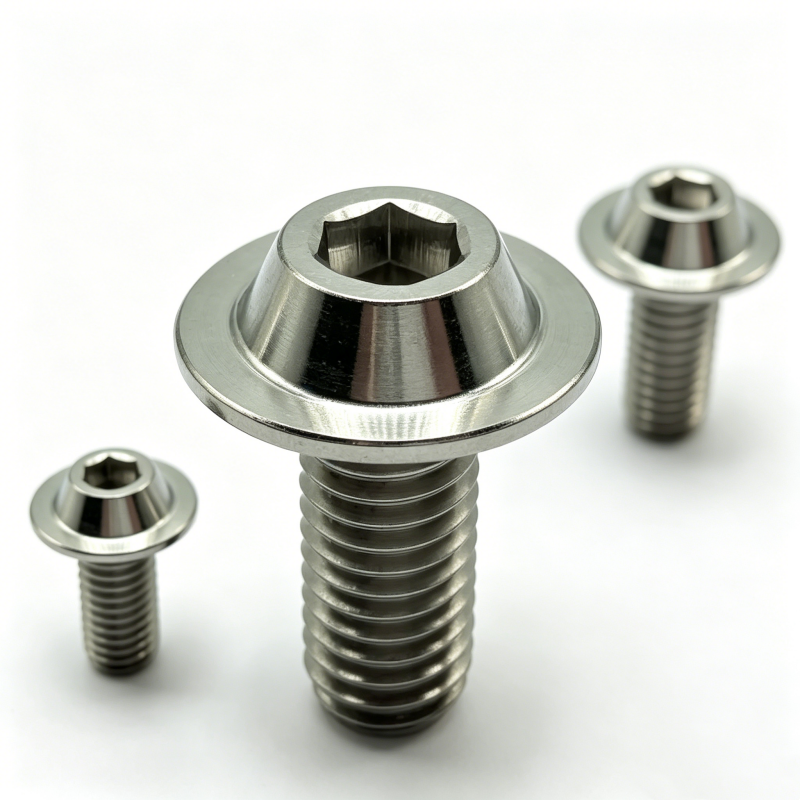
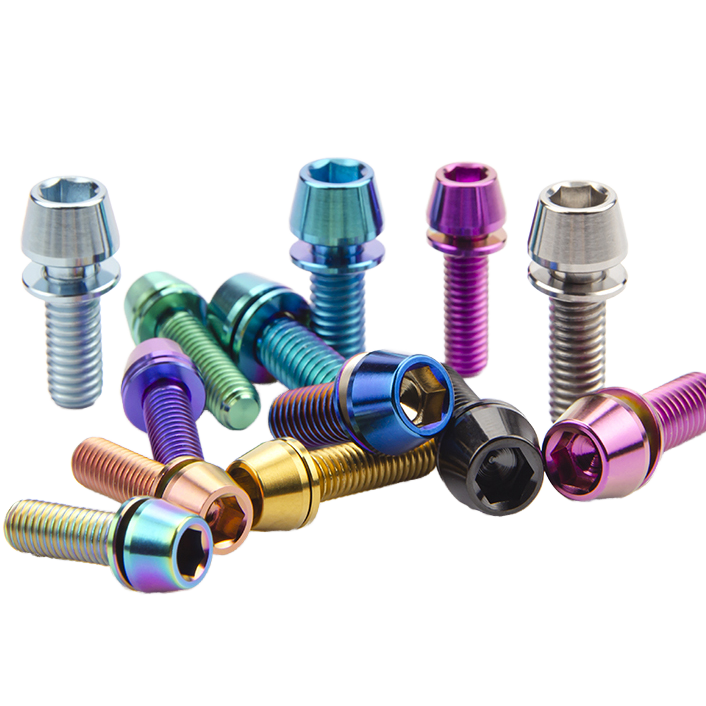
Our precision CNC multi-axis machined Grade 5 (Ti-6Al-4V) tapered socket and cone-head screws achieve exceptional clamp-load consistency, 895+ MPa tensile strength, and zero galvanic corrosion in aggressive working environments.
Why Tier-1 racing teams, aerospace engineers, and performance bicycle manufacturers substitute conventional socket cap screws with precision-turned tapered cone bolts.
Traditional flat 90-degree socket cap heads concentrate shear and tensile loads sharply at the 90-degree transition junction between shank and head. Tapered (cone/countersunk) profiles distribute dynamic cyclic stresses down an angled vector (commonly 45°, 60°, or 90° countersink), substantially alleviating notch sensitivity and extending mechanical fatigue life under heavy harmonic vibration.
At Verqo Titanium, our external threads are formed through severe plastic deformation using precision hydraulic thread-rolling dies rather than single-point CNC cutting. Cold thread rolling preserves the longitudinal metallurgical grain flow of the Ti-6Al-4V alloy, inducing beneficial surface compressive residual stresses and boosting fatigue endurance limits by over 35% compared to thread-turned alternatives.
With a specific density of 4.43 g/cm³ compared to 7.85 g/cm³ for Class 10.9/12.9 alloy steel, Grade 5 titanium delivers a direct 43.5% mass reduction. Replacing rotational and unsprung hardware—such as brake disc rotor bolts, caliper hanger pins, and sprocket fixings—measurably decreases rotational inertia, sharpens suspension responsiveness, and delivers tangible handling advantages.
| Mechanical / Chemical Property | Verqo GR5 (Ti-6Al-4V) | Commercial Pure GR2 Ti | Class 10.9 Alloy Steel | 316 Marine Stainless |
|---|---|---|---|---|
| Ultimate Tensile Strength (Rm) | ≥ 895 – 1000 MPa | ≥ 345 MPa | 1000 – 1040 MPa | 500 – 700 MPa |
| Yield Strength (Rp 0.2) | ≥ 828 MPa | ≥ 275 MPa | ≥ 900 MPa | ≥ 220 MPa |
| Material Density (g/cm³) | 4.43 g/cm³ (-43.5%) | 4.51 g/cm³ | 7.85 g/cm³ | 8.00 g/cm³ |
| Strength-to-Weight Ratio | 202 kNm/kg (Superior) | 76 kNm/kg | 127 kNm/kg | 75 kNm/kg |
| Chloride Pitting Resistance (PREN) | Virtually Immune (Oxide Film) | Immune | Prone to Severe Rust | Moderate (PREN 23–25) |
| Magnetic Permeability (μ) | 1.00005 (Non-Magnetic) | 1.00005 (Non-Magnetic) | Ferromagnetic (> 100) | Slightly Magnetic After Work |
| Thermal Expansion (10−6/K) | 8.6 (Close to Ceramics) | 8.9 | 11.7 | 16.0 |
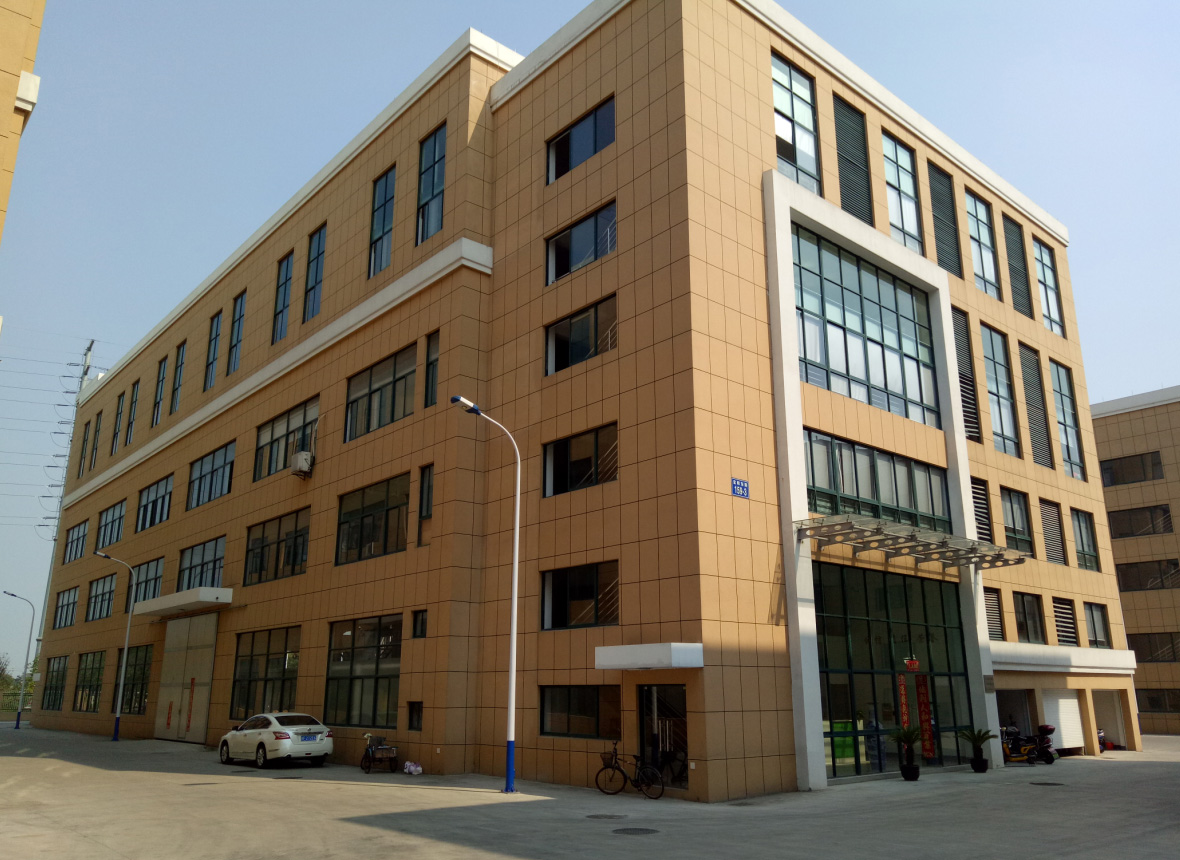
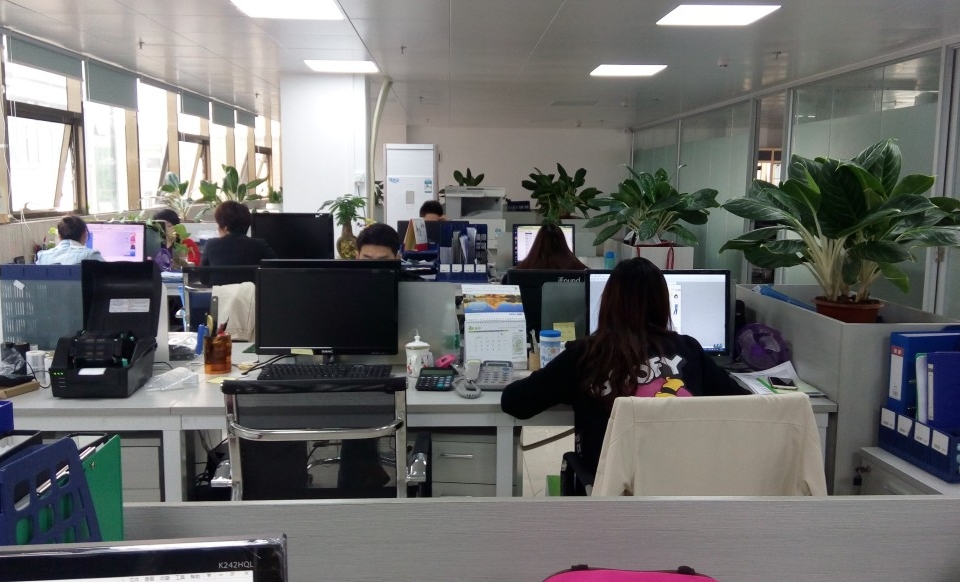
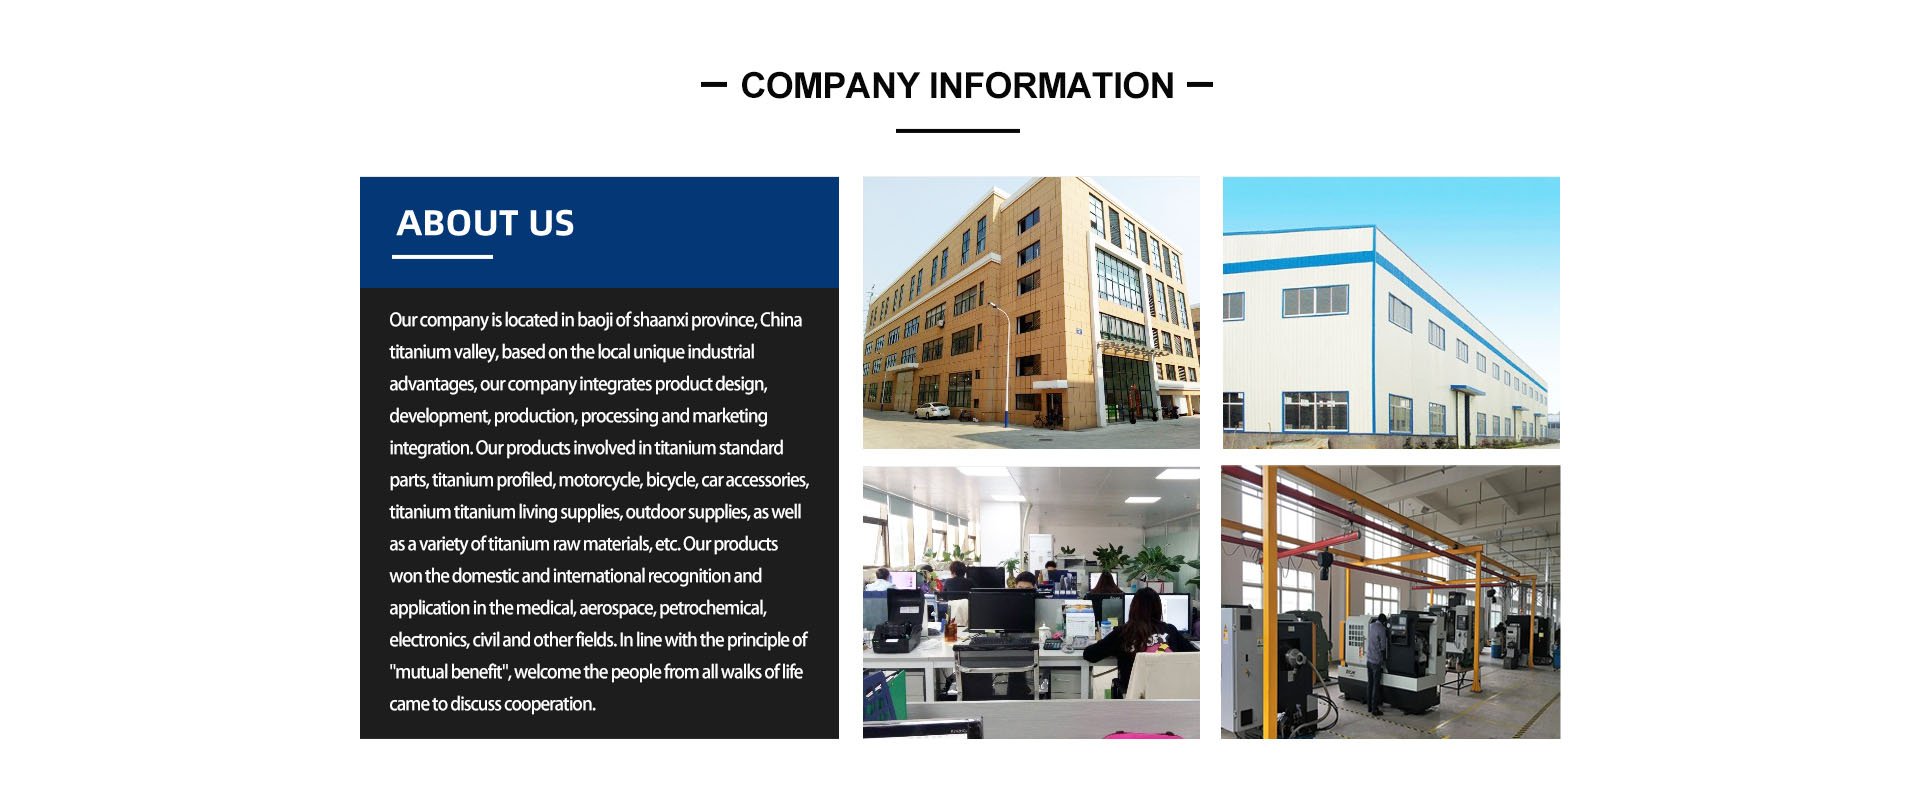
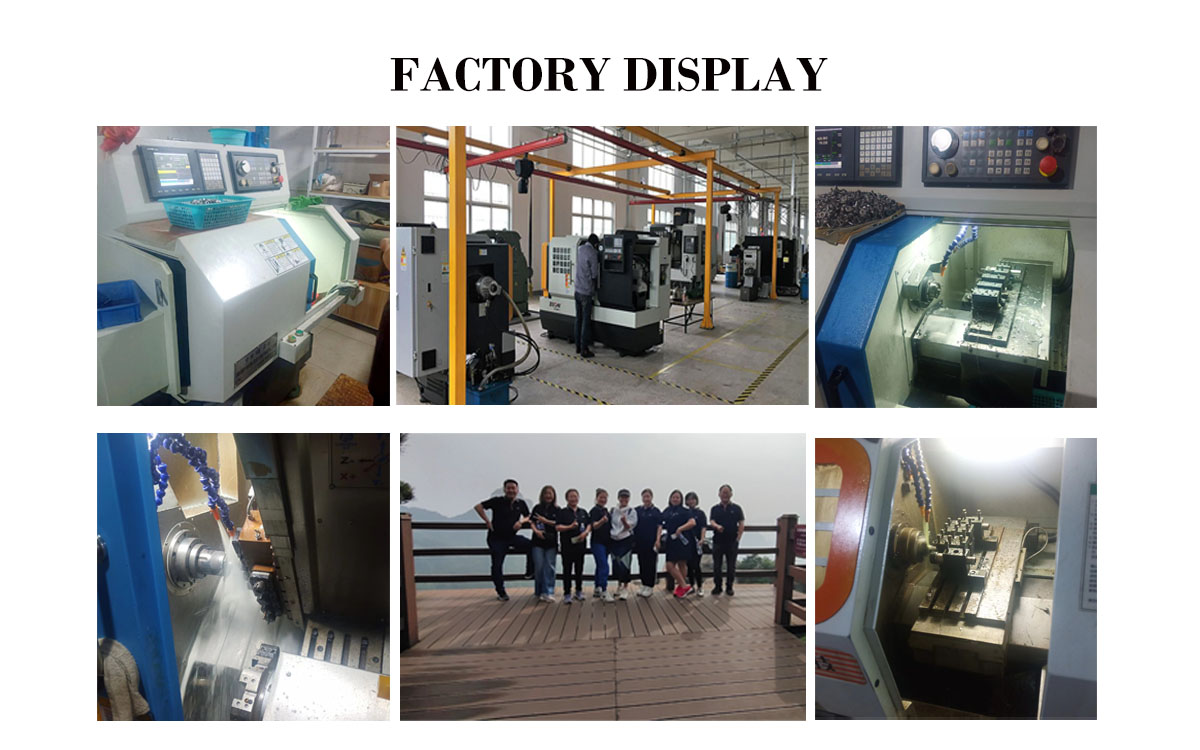
Headquartered in Baoji, Shaanxi—internationally renowned as "China's Titanium Valley"—Verqo Titanium Products Co., Ltd. operates integrated vacuum melting raw stock sourcing, 5-axis CNC machining, cold-forming, and surface conversion under one audited facility.
1,001–2,000 m² production footprint housing ultra-precision 5-axis Swiss lathes.
High-speed turning and micro-drilling maintaining tolerances within ±0.01 mm.
100% thread ring gauging and profile projection for defect-free assembly.
Turned tapered screws, flange bolts, lug nuts, and specialized shaped parts.
Positive Material Identification (PMI) by handheld XRF spectrometer.
Custom laser branding, anti-scuff division packaging, and worldwide logistics.
Located at the epicenter of China's titanium supply chain, we procure certified Grade 5 titanium ingots produced from triple-melt vacuum arc remelting (VAR). Every single batch is backed by comprehensive EN 10204 3.1 Mill Inspection Certificates.
With 10+ years of dedicated engineering expertise, we translate complex 2D blueprints, 3D STEP models, or physical samples into precision production runs. We tailor custom head heights, taper angles, micro-drilled lock-wire ports, and internal socket profiles.
Engineering inquiries receive formal technical evaluation within an average of ≤2 hours. Our responsive operations team maintains a 98.62% historical communication fulfillment rating, drastically compressing sourcing lead times for overseas distributors.
Avoid onerous supplier minimums. Standard catalog sizes ship from inventory with MOQs as low as 10 to 20 units. Bespoke custom CNC turned tapered bolts start at just 50 to 100 units, supported by secure B2B payment terms including T/T, L/C, and PayPal.
Global fastener sourcing is undergoing a structural transition toward lightweighting, extreme duty cycles, and automated assembly. Here is how international engineering and procurement directors are adapting their purchasing roadmaps.
The rapid rise of electric motorcycles (such as Surron Ultra Bee, Talaria Sting), high-performance e-bikes, and hybrid automotive powerplants has made gram-counting mission-critical. In battery-dense vehicles, saving unsprung mass on wheel hubs, suspension linkages, and brake calipers directly extends vehicle operating range and mitigates battery pack weight penalties. Titanium tapered bolts are now specified at OEM drawing stages rather than purely as aftermarket upgrades.
While traditional anodizing continues to provide vibrant cosmetic aesthetics for bicycle and consumer hardware, high-tier racing and industrial buyers are transitioning to Physical Vapor Deposition (PVD) vacuum sputtering. Thin-film coatings such as Diamond-Like Carbon (DLC), Titanium Nitride (TiN), and Titanium Aluminum Nitride (TiAlN) deliver surface micro-hardnesses exceeding 2,500 HV, drastically cutting friction coefficients and solving thread galling issues under dry assembly.
Hexagonal sockets (Allen keys) exhibit higher corner wall deformation risks under high-torque pneumatic tooling. Procurements across European and North American distributors increasingly dictate ISO 14581 style Torx (Hexalobular) recess drives or proprietary dual-drive configurations (external drilled hex with internal Torx). This enables mechanics to quickly torque taper bolts with safety wire drillings for FIA/FIM motorsport homologation compliance.
Supply chain volatility has penalized Western buyers working with intermediary trading houses. The procurement trend strongly favors direct contracts with vertically integrated manufacturers physically rooted in China's raw titanium clusters (Baoji). Direct access guarantees batch raw-material metallurgical consistency, shortens custom prototyping cycles from months to days, and captures 20–35% cost margins.
Verqo engineers are continuously advancing cold-forging, metallurgical heat treatments, and micro-machining capabilities. Here is how modern titanium fasteners are evolving.
Historically, Ti-6Al-4V has been considered virtually un-forgeable cold due to high strain hardening and narrow room-temperature plasticity. Verqo is adopting specialized warm-forging and multi-station progressive header machines to cold-form taper head preforms at rapid cycle rates, reducing machining swarf waste and slashing high-volume unit costs.
To eliminate the requirement for manual application of copper or nickel anti-seize paste on assembly lines, next-generation tapered bolts feature micro-encapsulated dry-film lubricants (such as molybdenum disulfide MoS&sub2; and micro-fluoropolymer sealants) factory-applied to threads, guaranteeing uniform clamp-torque tension relationships across 50+ re-torquing cycles.
By leveraging advanced gun-drilling Swiss lathes, Verqo engineers drill internal axial blind bores through the core of M8–M16 tapered bolts. Removing non-load-bearing core material drops fastener weight an additional 15–22% with zero reduction in allowable shear or tensile yield capabilities across critical engine-bay and chassis locations.
Clear, direct metallurgical and commercial answers to the most common inquiries raised by international B2B fastener purchasers and product design teams.
Verqo strictly utilizes certified Grade 5 (Ti-6Al-4V, Werkstoff 3.7165) for all load-bearing, automotive, motorcycle, and disc-brake tapered bolts. Grade 2 (Commercial Pure Titanium) has a tensile yield of only ~275 MPa, compared to Grade 5's ≥828 MPa yield. Substituting Grade 2 into high-stress or conical clamping locations risks catastrophic shear failure under service load. Grade 2 is only suitable for non-structural cosmetic covers or chemical fluid exposure where maximum ductility is demanded.
Conical taper head geometries (standard 45°, 60°, or 90° countersunk seats) self-center the fastener precisely within the mating counterbore. The 3D angled mating surface distributes clamping force across a continuous conical area rather than along a single sharp 90-degree step. This reduces point stresses, maintains clamp tension under harmonic vibrations, and provides flush or semi-flush profiles that improve aerodynamic laminar flow in motorsport and cycling.
Titanium alloys naturally produce a thin, self-healing oxide film (TiO&sub2;) that can create microscopic friction micro-welding when torqued dry into aluminum, stainless steel, or titanium female threads. Verqo counters this by offering rolled thread micro-finishes (Ra ≤ 0.4 μm), physical vapor deposition (PVD) anti-wear coatings (DLC or TiN), and issuing recommended installation torque tables with titanium-specific anti-seize paste specifications for every production run.
Wherever technically feasible from M2 through M26, Verqo utilizes hydraulic cold thread-rolling machines. Machining (cutting) threads with a CNC lathe cuts through the metal's internal grain boundary structure, introducing micro-notches where fatigue cracks can initiate under cyclic load. Rolled threads compress the grains along the profile, work-harden the root radius, and boost fatigue life by 30% to 50%—a mandatory requirement for brake rotors, engine internals, and steering components.
We machine to ISO metric standard coarse and fine pitches (e.g., M6×1.0, M8×1.25, M10×1.0/1.25, M12×1.25/1.5, M14×1.5) as well as UNC/UNF imperial specifications. Standard machining tolerance achieves ISO 965-2 6g for external threads and ±0.02 mm across head diameter and taper angles. Precision aerospace-grade 4h tolerances are available upon custom engineering request.
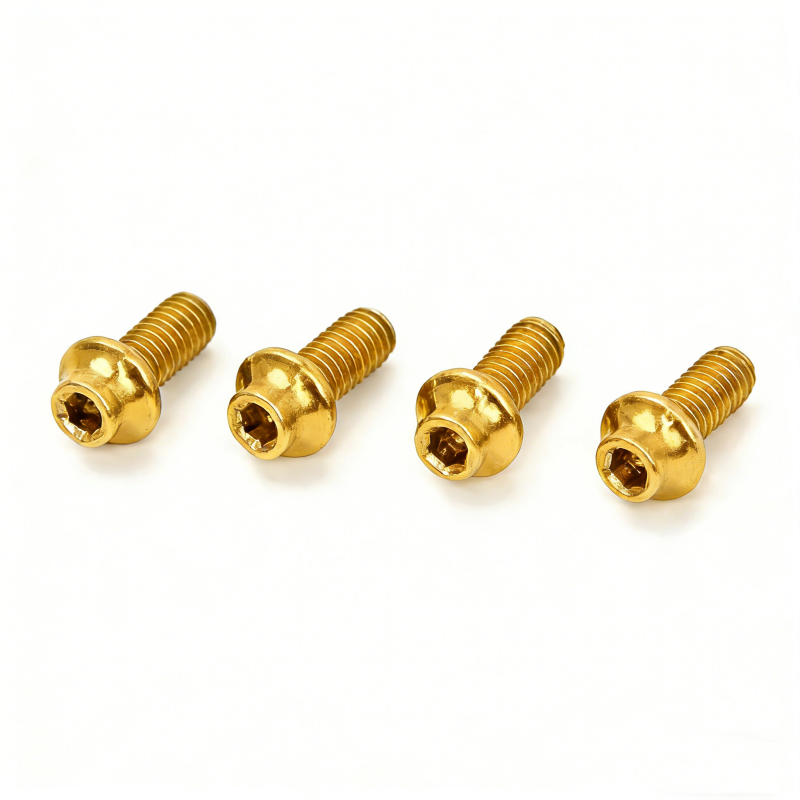
Electrolytic Anodizing alters the thickness of the natural titanium oxide layer, refracting ambient light into brilliant colors (gold, blue, purple, burnt blue, rainbow) without adding pigments or weight. However, anodized layers are thin (~100–300 nm) and can scuff under metal-to-metal tool contact. PVD (Physical Vapor Deposition) deposits a hard ceramic film (such as DLC or TiAlN) 1–3 μm thick under high vacuum, delivering exceptional scratch resistance, UV stability, and reduced sliding friction.
Yes. Over 60% of our production volume represents custom OEM/ODM configurations. Our engineering office works seamlessly with PDF drawings, STEP (.stp), IGES, DWG, and SolidWorks CAD files. We conduct a Design-for-Manufacturability (DFM) review within 2 hours, confirming raw bar stock diameter, optimal tooling paths, socket recess broaching methods, and finish specifications.
Every bulk export shipment from our Baoji facility can be accompanied by a standard EN 10204 3.1 Mill Test Certificate detailing heat number, chemical composition analysis (Ti, Al, V, Fe, C, N, H, O content per ASTM B348), ultimate tensile strength, yield strength, and elongation percentage. Full dimensional inspection reports (CMM / optical comparator) are archived and provided upon request.
For items carried in our regular production inventory (e.g., M5/M6 bicycle bottle cage bolts, standard M8/M10 brake disc bolts), MOQs start at just 10 to 20 pieces. For custom CNC-turned parts requiring unique tooling setups, MOQs typically range from 50 to 100 units. Prototyping samples are completed within 5 to 7 working days; bulk mass production cycles average 15 to 25 days depending on PVD coating batch requirements.
Grade 5 titanium's coefficient of thermal expansion is 8.6 × 10⁻⁶ / K, significantly lower than aluminum (approx. 23 × 10−6 / K) and stainless steel (approx. 16 × 10−6 / K). When titanium tapered bolts are threaded into aluminum housings (such as motorcycle crankcases or wheel hubs) subject to thermal cycling, the differential thermal expansion actually increases clamp preload as temperatures rise. Our engineering team calculates and provides cold-torque recommendations to ensure fasteners remain well within their elastic limit under peak engine and braking thermal cycles.
Whether you require high-volume catalog tapered screws from stock or a high-precision custom OEM production batch manufactured to strict CAD tolerances, Verqo Titanium's Baoji engineering facility delivers unmatched reliability, certified metallurgical traceability, and rapid factory-direct pricing.