Average response ≤ 2 hours
Baoji, Shaanxi – China's Titanium Valley

China Wholesale Titanium Flange Bolts Suppliers & Exporter

Precision-Engineered Grade 5 (Ti-6Al-4V) Hex & 12-Point Flange Fasteners Direct from Baoji's Titanium Manufacturing Hub. Custom OEM/ODM Solutions from M2 to M26.

ASTM B348 / AMS 4928 Certified 100% Ultrasonic & Optical Thread Inspection Factory Response ≤ 2 Hours
10+ Years OEM/ODM Mastery
M2–M26 CNC Thread Scope
≈43% Mass Saving vs Steel
98.62% Fast Response Rate
900+ MPa Min. Tensile Strength (Gr5)
Engineered Fasteners Matrix

High-Performance Titanium Flange Bolts & Hardware Series

Engineered for high-stress automotive, motorsport racing, e-mobility, and high-spec industrial platforms requiring zero corrosion and an exceptional strength-to-weight ratio.

Engineering Whitepaper

Structural Mechanics of Titanium Flange Bolts in Critical Joints

A metallurgical analysis on why aerospace-grade Ti-6Al-4V flange fasteners outperform conventional separate bolt-and-washer configurations under high cyclical vibration and corrosive service.

1. The Integral Flange Advantage: Eliminating Galling & Stress Concentration

In high-torque mechanical assemblies, conventional socket and hex bolts rely on separate split washers or flat washers to distribute compressive loads. In harsh vibration environments—such as motorcycle crankcases, performance automotive exhaust headers, and unsprung suspension hubs—individual washers generate micro-slip interfaces. This micro-movement accelerates fretting wear, strips protective anodized coatings, and introduces unpredictable pretension losses.

An integrated flange head bolt engineered according to DIN 6921 or ISO 4144 eliminates this failure mode entirely. By uniting the bolt head and distribution skirt into a continuous, hot-forged or precision-machined grain flow, the contact surface area is expanded by up to 45% to 60% compared to standard cap heads. This prevents bolt embedding into softer substrate materials like billet 6061-T6 aluminum, magnesium alloy swingarms, and carbon fiber laminates.

Key Engineering Finding: Flange bolts eliminate frictional interface creep between washer and bolt under shear excitation. In comparative cyclic strain testing under ISO 3800 protocols, Grade 5 Ti-6Al-4V integral flange bolts retained 94.2% of initial clamping preload after 100,000 harmonic cycles, versus 78.6% for standard socket bolts assembled with independent flat washers.

2. Cold-Rolled vs. Machine-Cut Threads: Grain Flow Integrity

A vital metric in B2B procurement of titanium flange hardware is the thread production methodology. Low-cost manufacturers often machine threads via single-point CNC lathe turning. While dimensionally compliant, cut threading slices directly through the metal grain matrix, producing microscopic notch stress points along the thread roots where micro-cracks propagate during cyclic fatigue loading.

At our Baoji manufacturing plant, all Grade 5 titanium flange bolts undergo precision cold thread rolling between circular carbide dies under intense hydraulic pressure. Thread rolling plastically deforms the Ti-6Al-4V crystal structure without cutting fibers, causing the metallurgical grain flow to follow the continuous contour of the crests and roots. This cold-working burnishing effect imparts compressive residual stress at the critical root radius, boosting endurance limit and cyclic fatigue life by more than 300%.

Mechanical / Physical Property Verqo GR5 (Ti-6Al-4V) Commercial Pure Ti (GR2) Alloy Steel 10.9 Stainless Steel (316/A4-80)
Nominal Chemical Composition Ti-6Al-4V (Grade 5) Unalloyed Titanium 40CrMo / 42CrMo4 Fe-18Cr-12Ni-2.5Mo
Mass Density (g/cm³) 4.43 g/cm³ (≈43% Lighter) 4.51 g/cm³ 7.85 g/cm³ (Baseline) 8.00 g/cm³
Tensile Strength, Rm (MPa) ≥ 895 – 1,050 MPa ≥ 345 MPa ≥ 1,040 MPa ≥ 800 MPa
Yield Strength, Rp0.2 (MPa) ≥ 828 – 940 MPa ≥ 275 MPa ≥ 940 MPa ≥ 600 MPa
Modulus of Elasticity (GPa) 114 GPa (Shock Absorbing) 105 GPa 210 GPa (Stiff) 193 GPa
Chloride Pitting Resistance (PREN) Immune (Passive TiO&sub2; layer) Immune Extremely Poor (Rusta) Moderate (PREN ≈ 25)
Magnetic Permeability (μ) Non-magnetic (1.00005) Non-magnetic Ferromagnetic Slightly Paramagnetic
Typical Engineering Role Chassis, Brake Rotors, Turbos Non-structural Trim Standard High-Load Mach. Marine Non-Critical Trim
Market Intelligence

Future Procurement Trends in Titanium Hardware (2025–2030)

Global supply chain analysis for B2B procurement managers, technical directors, and high-volume fastener distributors preparing for next-generation performance requirements.

1. E-Mobility Light-Weighting

As electric motorcycles and performance EVs seek greater range and battery capacity, reducing unsprung mass at brake calipers, suspension knuckles, and motor casing joints via Grade 5 titanium is shifting from luxury motorsport into tier-1 serial production.

2. Direct Baoji Mill Sourcing

Procurement directors are actively bypassing multiple intermediary trading hubs in favor of direct manufacturer engagement in Baoji (“China Titanium Valley”). This direct supply model delivers 15-25% landed cost reductions and transparent EN 10204 3.1 mill material certifications.

3. PVD over Wet Chemical Finishes

Strict Western environmental directives (REACH, RoHS) are spurring widespread replacement of conventional wet anodizing with Physical Vapor Deposition (PVD). PVD coatings yield diamond-like hardness (Hv ≥ 2500) and friction coefficients below 0.15 without hazardous chemical runoff.

4. Multi-Drive & Safety Wire Specs

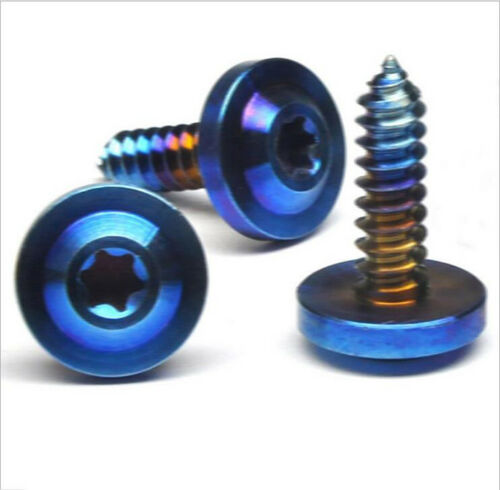
High-end motorsport racing leagues (MotoGP, Isle of Man TT, WEC) now require dual-drive heads—combining an external hex with an internal Torx or drilled flange holes for safety locking wire. Sourcing suppliers with flexible multi-axis tooling prevents expensive secondary machining.

Advanced Manufacturing

Technological Evolutions in Titanium Hardware Fabrication

How 5-axis Swiss screw turning, precision hot head forging, and computerized surface functionalization are defining modern fastener reliability.

Precision Hot Forging vs CNC

While small batches rely on 5-axis Swiss CNC turning from certified titanium bar stock, high-volume flange bolts (M6 to M16) are increasingly formed via multi-station warm heading. Heating the Ti-6Al-4V stock to the alpha-beta transition phase (approx. 850°C–920°C) ensures unbroken internal metal fiber alignment across the flange perimeter, doubling tensile shear strength.

Anti-Galling Micro-Geometry

Titanium naturally forms an instantaneous, passive titanium dioxide (TiO&sub2;) layer. However, severe friction under heavy torque can shear this oxide film, resulting in metal-on-metal galling or thread seizure. Modern fabrication employs engineered thread relief grooves, controlled micro-radius root rounding, and proprietary anti-friction PVD coatings that eliminate thread locking.

Automated Optical Laser Sorting

Automotive assembly lines require sub-10 PPM (parts per million) defect rates. Modern export-oriented production lines integrate 360-degree high-speed optical camera sorting systems that verify thread pitch, shank straightness, head concentricity, and flange planar perpendicularity at speeds over 400 pieces per minute.

Factory Advantage

Why International Buyers Partner with Verqo Titanium

Combining the metallurgical wealth of China's Titanium Valley with precision German and Japanese CNC capabilities to power your fastener supply chain.

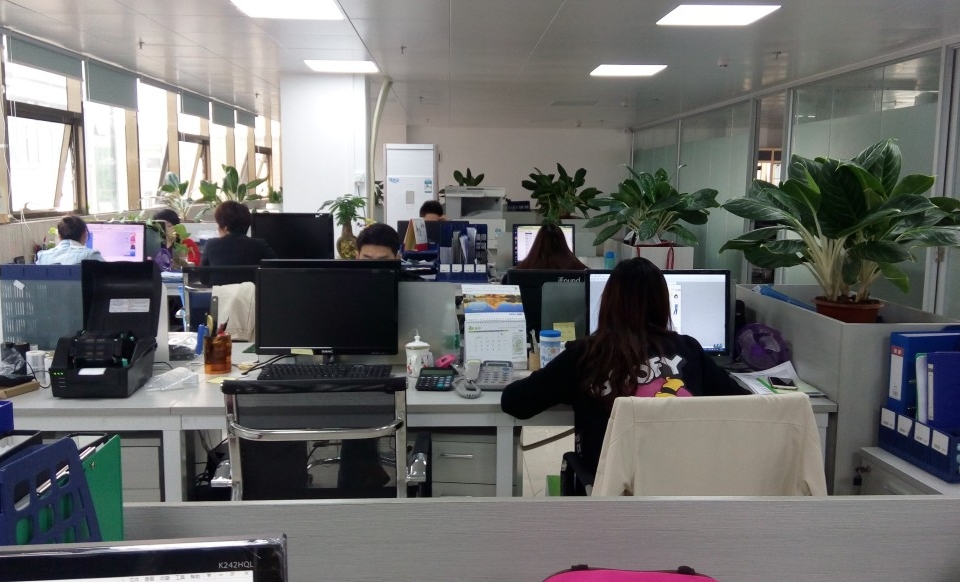
Verqo titanium production workshop

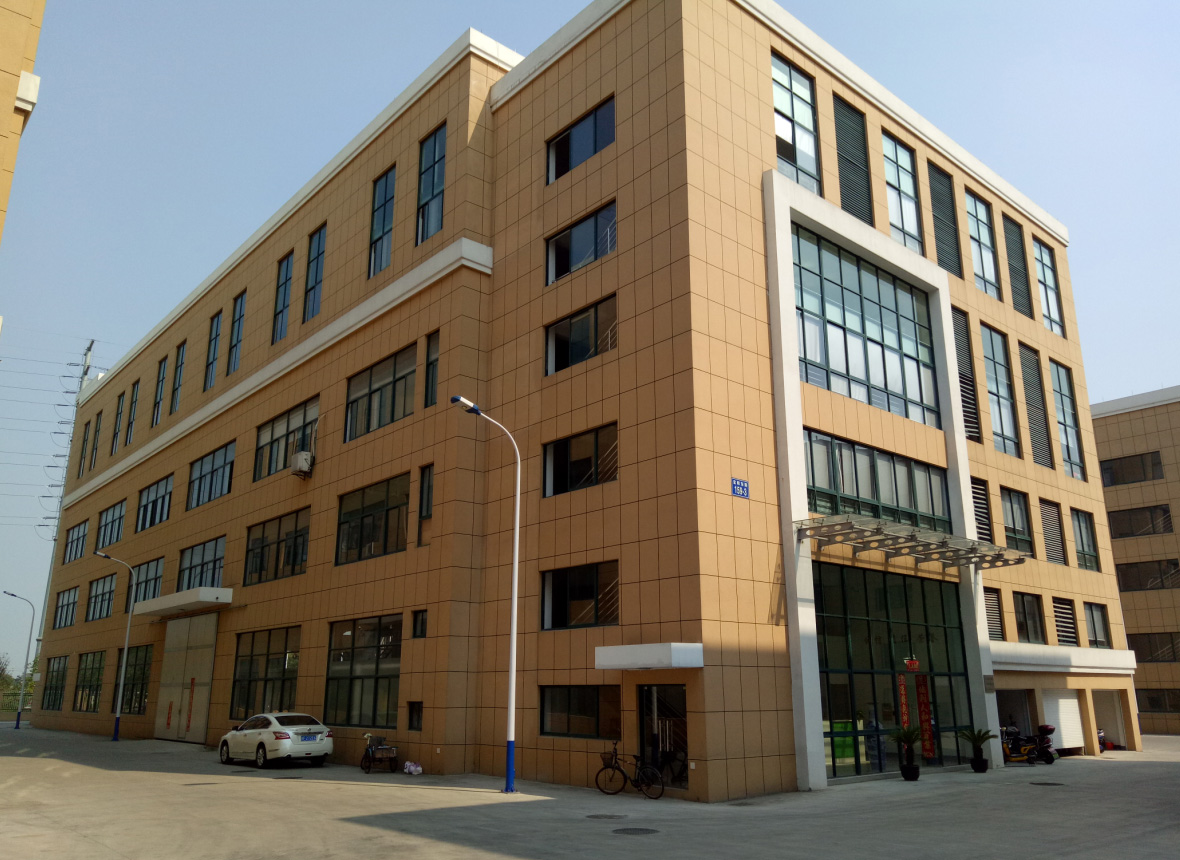
Baoji Titanium Valley Production Base

Direct supply contracts with national titanium sponge smelters ensure 100% genuine aerospace-grade Ti-6Al-4V material with complete ingot tracing and zero secondary scrap blending.

CNC Machining of Titanium Components

Multi-Axis High-Precision Machining

Equipped with 3-axis, 4-axis, and 5-axis CNC multi-spindle automatic screw machines maintaining tight dimensional tolerances within ±0.01 mm from miniature M2 fasteners up to M26 industrial bolts.

Inspection and Quality Control

Rigorous In-House QC Protocols

Every single batch undergoes spectral chemical composition assays, Rockwell hardness testing, optical thread gauge verification, and tensile proof loading before export clearance.

Rapid Quote ≤ 2 Hours

Our bilingual mechanical sales engineering team provides full drawing feasibility reviews, quote estimates, and DFM recommendations within an average turnaround time under 2 hours.

Flexible Minimum Order Quantities

Eliminate inventory pressure. We support flexible MOQs from small prototype evaluations (10–20 pieces) to containerized high-volume scheduled releases for regional wholesalers.

Anodizing & PVD In-House

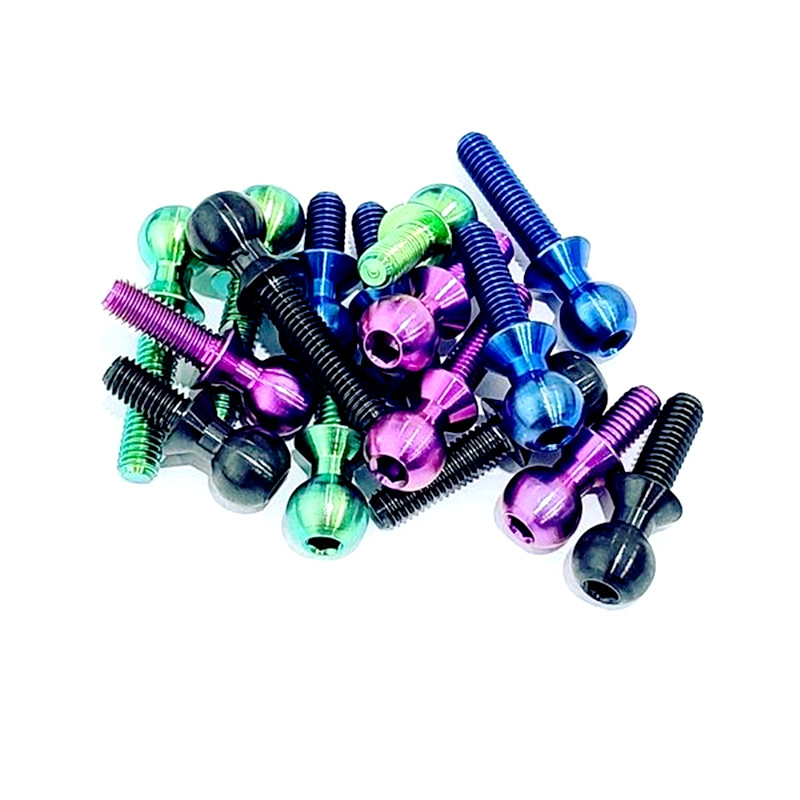
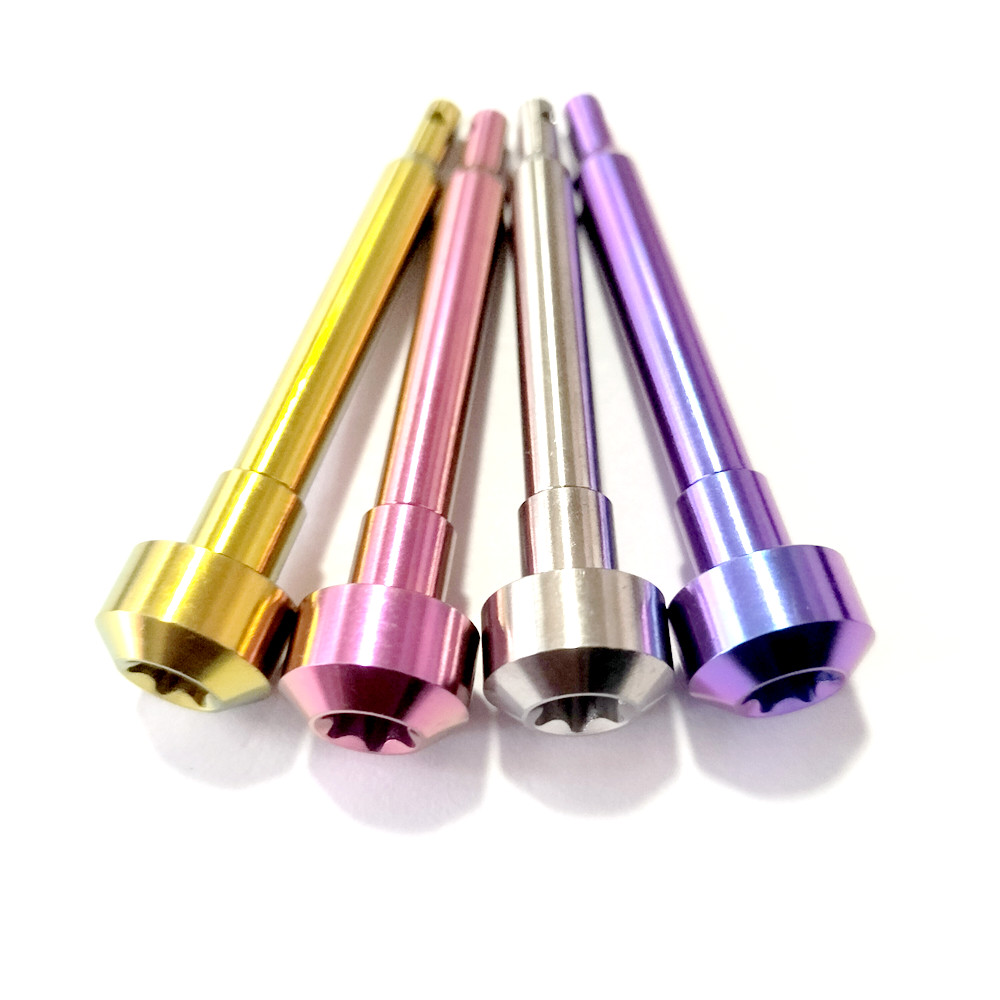
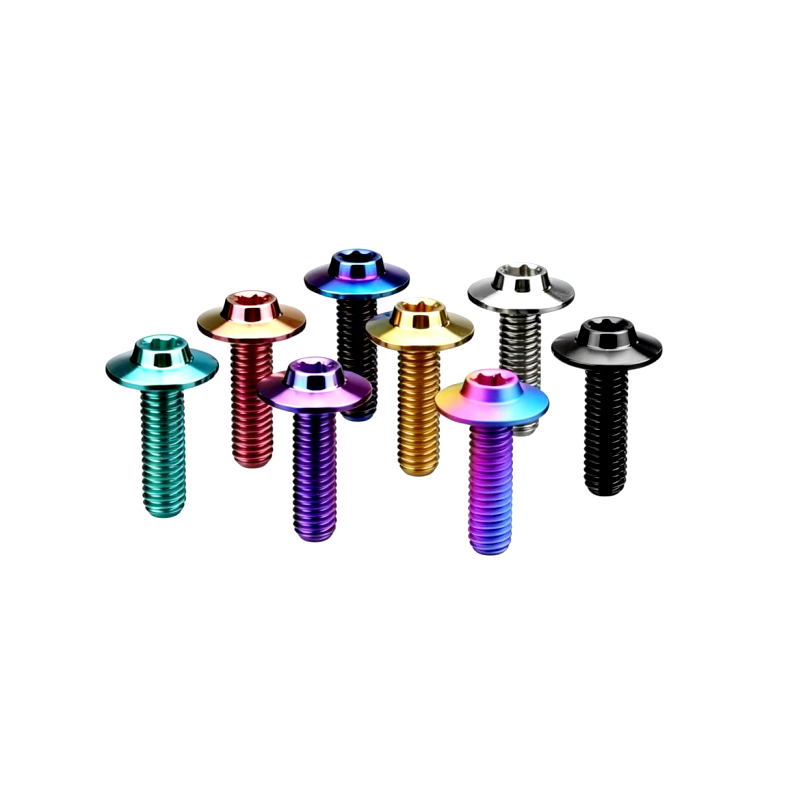
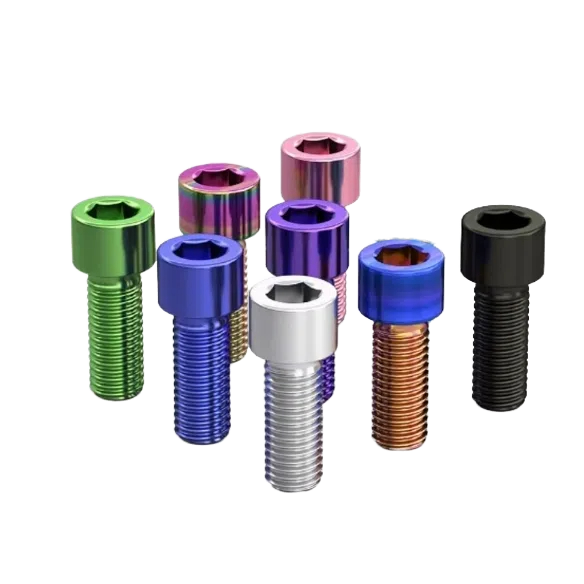
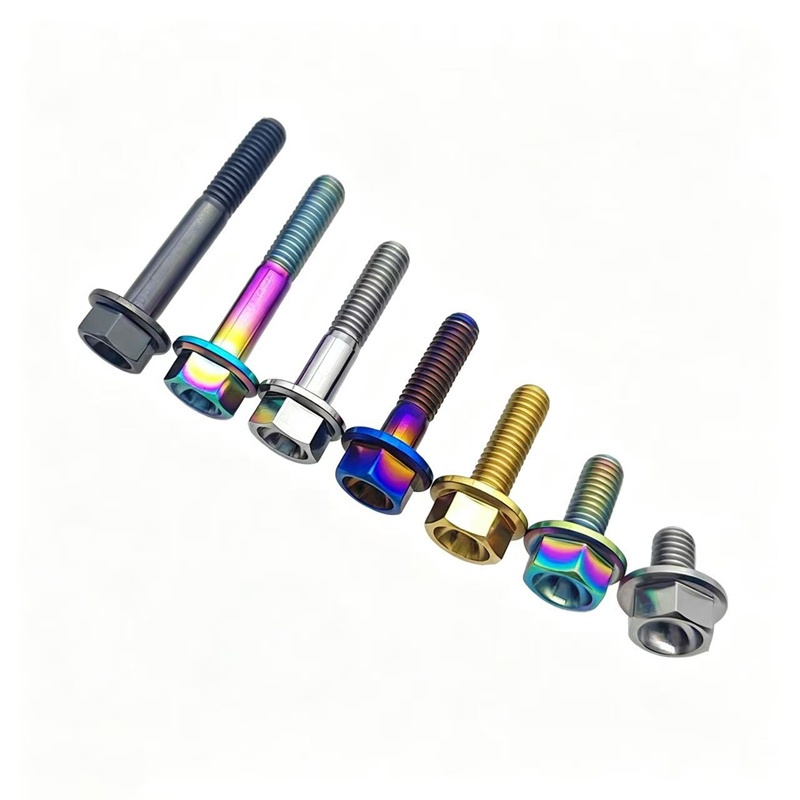
Get custom vibrant finishes: raw polished, royal gold, cobalt blue, deep purple, burnt blue flame-treatment, and abrasion-resistant oil-slick rainbow or stealth matte black PVD.

Comprehensive OEM Customization

From CAD step files or physical samples, our tooling division manufactures custom head styles (umbrella, 12-point, drilled race flange) and specialized pitch threads (e.g. M10x1.25, M12x1.25).

B2B Knowledge Hub

Frequently Asked Questions on Titanium Flange Bolts Sourcing

Direct technical answers addressing mechanical properties, surface treatment specs, torque management, and international trade compliance.

Q Why choose Ti-6Al-4V Grade 5 over Commercial Pure Grade 2 for flange bolts?

Commercial Pure Titanium (Grade 2) possesses a yield strength of approximately 275 MPa, which is only suitable for non-structural body panels or decorative trim. Grade 5 (Ti-6Al-4V) is an alpha-beta alloy with a yield strength exceeding 828 MPa and tensile strength over 895–1050 MPa. In load-critical joints such as engine mounts, brake calipers, and wheel assemblies, Grade 5 is essential to prevent plastic deformation and joint separation under dynamic load spikes.

Q How does an integral flange eliminate the need for standard washers?

The integrated flange acts as an immovable, perfectly centered washer that increases the bearing surface area beneath the fastener head. This design lowers the surface contact pressure on the clamped components, avoids surface scuffing during torquing, prevents fastener embedding into soft alloys (like aluminum or magnesium), and reduces preload loss caused by cyclic mechanical vibration.

Q What thread pitch standards are available for wholesale export?

We manufacture full metric standard coarse threads (DIN 6921, ISO 4144, JIS B1189) from M2 to M26, as well as metric fine-pitch variants widely required in automotive and motorsport hubs (e.g., M10×1.25, M12×1.25, M12×1.5, M14×1.5). UNC and UNF imperial standard pitch fasteners are also fully supported for sprint car and North American motorsport platforms.

Q How do you prevent thread galling (seizure) during installation?

Titanium threads have a higher friction coefficient than zinc-plated steel. To ensure repeatable torque-tension relationships and prevent cold welding or galling, we recommend applying a molybdenum disulfide (MoS&sub2;) or copper-based anti-seize paste during installation. Alternatively, our factory offers dry-film lubricant or PVD coatings that significantly lower friction coefficients for dry installations.

Q What is the difference between Anodized colors and PVD vacuum coating?

Anodizing is an electrochemical process that grows the natural titanium oxide (TiO&sub2;) layer to specific optical thicknesses, generating bright interference colors (gold, blue, purple, bronze). PVD (Physical Vapor Deposition) is a high-vacuum plasma deposition process that bonds an ultra-hard ceramic compound (like TiN or TiCN) to the metal surface. PVD provides significantly higher scratch resistance, chemical barrier protection, and enables rich dark tones like deep metallic black and oil-slick rainbow.

Q Can you manufacture custom flange heads from 2D/3D customer drawings?

Yes. With our in-house tooling and 5-axis CNC turning centers, we routinely produce OEM/ODM parts from STEP, IGES, DWG, and DXF files. We can integrate custom flange diameters, scallops for weight saving, internal Torx/Hex sockets, drilled hex heads for lock-wire routing, and laser-etched batch codes or private customer logos.

Q What quality certificates accompany international shipments?

Every commercial export order includes an EN 10204 Type 3.1 Mill Test Certificate detailing the exact chemical composition (aluminum, vanadium, iron, oxygen, hydrogen, and carbon contents) and mechanical tensile testing results. Upon request, we provide third-party SGS/TÜV test reports, optical coordinate measuring machine (CMM) dimensional reports, and salt-spray test certifications.

Q What are the standard lead times and export payment terms?

Stock sizes (such as standard M6, M8, and M10 hex flange bolts in raw or anodized finishes) ship within 3 to 7 working days. Custom CNC or warm-headed production typically requires 15 to 25 working days depending on quantity and coating choice. We accept T/T bank wire, L/C at sight, and PayPal for prototype orders, with global express courier (DHL, FedEx, UPS) and door-to-door DDP air/sea freight available.
Accelerate Your Supply Chain with Factory-Direct Pricing

Contact our engineering sales team in Baoji today for instant technical guidance, free CAD drawings review, and our complete wholesale B2B titanium fastener catalog.