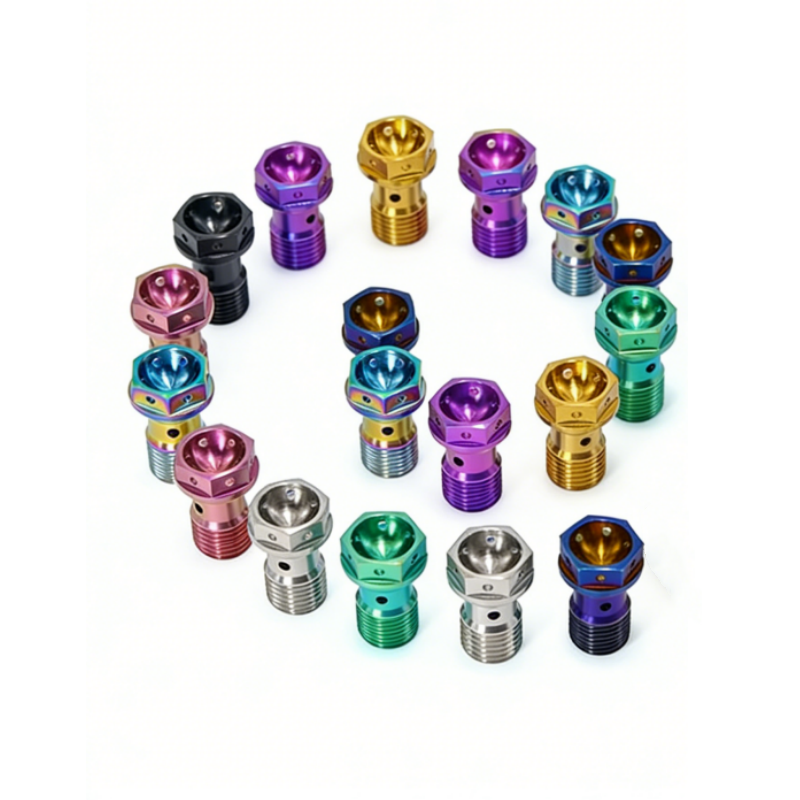
Brake Caliper Line
Direct factory production with micron-level CNC tolerances, cold/hot forged heads, rolled threads, and proprietary anti-galling PVD coatings.
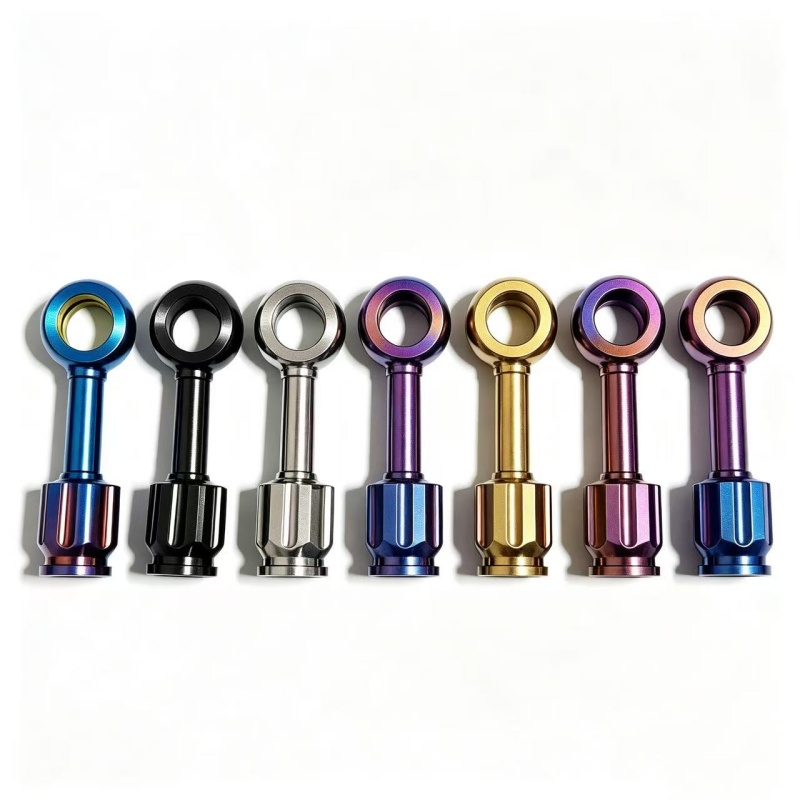
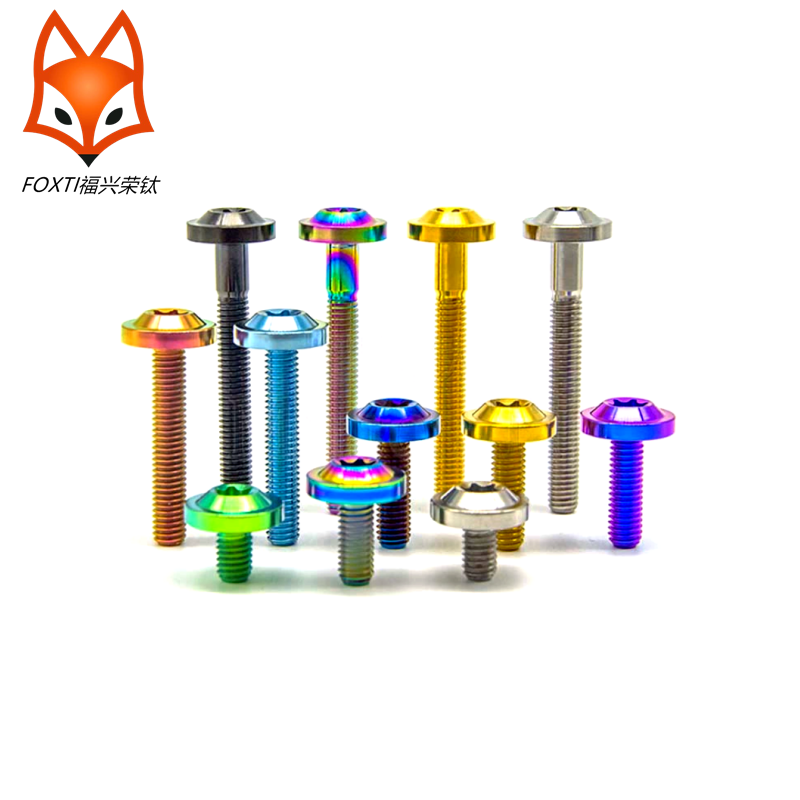
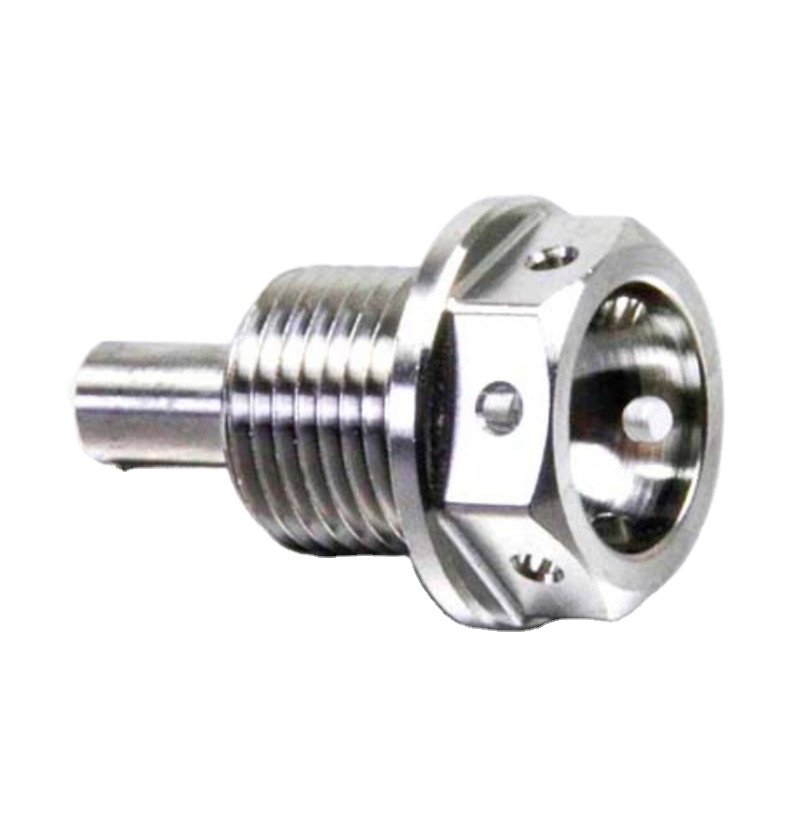
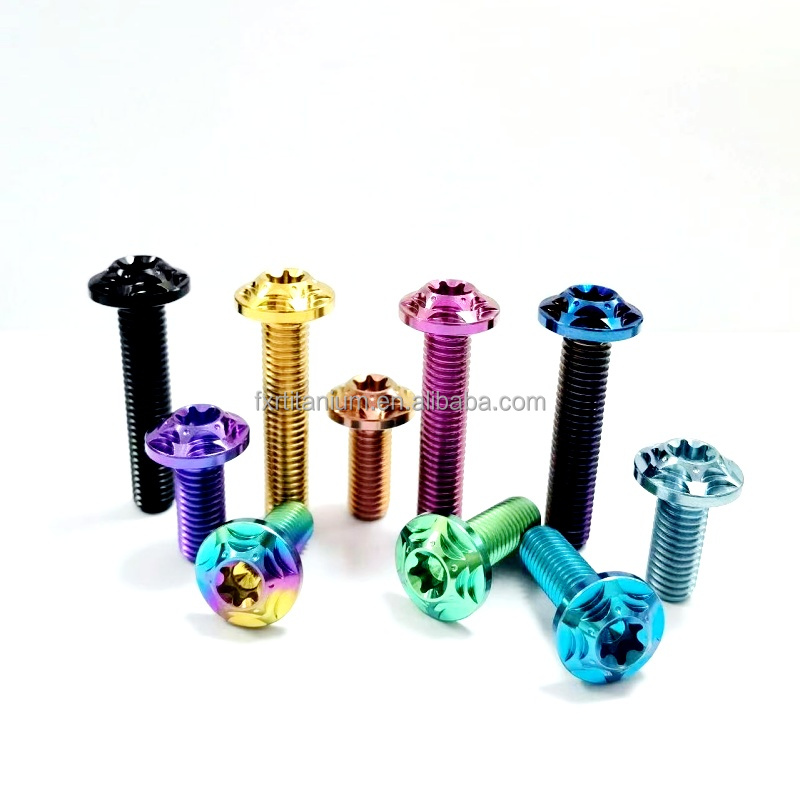
When engineering high-integrity bolted joints in motorsport, aviation, and subsea robotics, substituting Grade 8.8 or Grade 10.9 alloy steel with titanium alloys requires comprehensive understanding of material physics. Fasteners do not simply experience uniaxial tension; they operate under dynamic combinations of cyclic fatigue, transverse shear, torsional installation stress, and galvanic electrochemistry. At Verqo (FOXTI Titanium), all OEM fastener programs are built on rigorous metallurgical validation under ISO 9001:2015 and aerospace standard AMS 4928.
The vast majority of commercial commercial-off-the-shelf (COTS) fasteners fail because manufacturers substitute ductile Grade 2 commercially pure (CP) titanium into structural applications that mandate alpha-beta titanium alloys. Commercially pure Grade 2 exhibits a minimum yield strength of merely 275 MPa, rendering it unsuitable for caliper bolts, lug nuts, or suspension linkages.
In contrast, Grade 5 (Ti-6Al-4V, UNS R56400) provides an exceptional strength-to-density ratio. With an annealed tensile yield exceeding 828 MPa and ultimate tensile strength surpassing 895 MPa (often reaching 950–1050 MPa after controlled work-hardening), Grade 5 approaches Class 10.9 structural steel performance while reducing mass by 43.5% (density of 4.43 g/cm³ compared to 7.85 g/cm³ for alloy steel).
| Alloy Specification | Yield Strength (Rp0.2, MPa) | Tensile Strength (Rm, MPa) | Density (g/cm³) | Modulus of Elasticity (GPa) | Corrosion Rate (Seawater, mm/yr) | Primary Industrial Application |
|---|---|---|---|---|---|---|
| Ti-6Al-4V (Grade 5 / AMS 4928) | 828 – 910 | 895 – 1000 | 4.43 | 110 – 114 | < 0.0001 (Immune) | Brake Calipers, Wheel Lug Nuts, Connecting Rods |
| Ti-6Al-4V ELI (Grade 23 / Medical) | 790 – 830 | 860 – 910 | 4.43 | 110 – 114 | < 0.0001 (Immune) | Surgical Implants, Cryogenic Hardware, Subsea Shells |
| Ti-3Al-2.5V (Grade 9 / Half-Alloy) | 485 – 585 | 620 – 720 | 4.48 | 100 – 105 | < 0.0001 (Immune) | Hydraulic Tubing, Bicycle Frames, Pushrods |
| CP Titanium (Grade 2 / Unalloyed) | 275 – 350 | 345 – 450 | 4.51 | 103 – 107 | < 0.0001 (Immune) | Chemical Tank Fasteners, Non-Structural Trim |
| High-Tensile Steel (Class 10.9) | 940 – 1000 | 1040 – 1100 | 7.85 | 205 – 210 | > 0.15 (Severe Rust) | Automotive Baseline Structural Fasteners |
| A4-80 Stainless Steel (AISI 316) | 600 – 650 | 800 – 850 | 8.00 | 193 – 200 | 0.005 (Pitting Risk) | Marine Architectural Fasteners |
Crucial Engineering Insight: Because titanium's Elastic Modulus (E ≈ 110 GPa) is roughly half that of carbon steel (E ≈ 210 GPa), a titanium bolt undergoes double the elongation of a steel fastener at an identical clamp preload. This compliance provides superior vibration resistance and retention under thermal expansion shocks, effectively mitigating joint relaxation.
A foundational principle in Verqo's factory floor processing is the strict separation between cut threads and cold-rolled threads. While single-point CNC thread cutting is necessary for custom M20+ large-diameter internal oil drain plugs or low-volume prototypes, high-stress cyclic bolts (such as Brembo banjo bolts, cylinder head studs, and disc rotor bolts) must utilize cold thread rolling.
Single-point machining severs the continuous metallic crystalline grain fibers of the Grade 5 bar stock, creating microscopic stress concentrations at the root radii. In contrast, precision thread rolling plastically deforms the workpiece between cylindrical rolling dies under thousands of kilonewtons of hydrostatic pressure. This burnishes the root valley, induces critical compressive residual stresses (-300 to -500 MPa), and refines grain flow along the thread flank profile. The result is a 30% to 42% increase in thread fatigue life under cyclic tensile loading.
Strategic supply chain evolution driving next-generation engineering adoption in high-performance hardware.
As electric motorcycles (such as Sur-Ron, Talaria, and Stark VARG) and commercial battery packs push gross vehicular weights higher, engineers cannot afford parasitic chassis mass. OEM designers are aggressively replacing legacy zinc-plated steel hardware with lightweight titanium bolts, directly recuperating regenerative brake efficiency and suspension responsiveness.
While traditional electrochemical anodizing provides striking decorative tones, high-stress motorsport environments demand superior tribological coatings. Sourcing is shifting toward Physical Vapor Deposition (PVD) applied Titanium Nitride (TiN - Gold), Titanium Carbonitride (TiCN), and Diamond-Like Carbon (DLC), which offer micro-hardness exceeding 2,500 HV to eliminate contact galling.
Global original equipment manufacturers are abandoning fragmented multi-tier brokers in favor of vertically integrated factories situated in Baoji ("China Titanium Valley"). Direct mill access to vacuum arc remelted (VAR) titanium sponge ensures verifiable lot-to-lot traceability and cushions procurement budgets against international raw material market fluctuations.
The manufacturing frontier incorporates laser powder bed fusion (LPBF) to produce topologically optimized, hollow-stem titanium bolts for Formula 1 and hypercars, which are then precision post-machined on multi-axis Swiss CNC lathes. This reduces internal structural mass by an additional 18% compared to solid shank fasteners.
B2B procurement protocols increasingly mandate complete digital material pedigrees. Every shipment must feature EN 10204 3.1 chemical spectrometry and mechanical tensile certifications tracking the ingot melt, preventing counterfeit or contaminated scrap alloys from compromising critical assemblies.
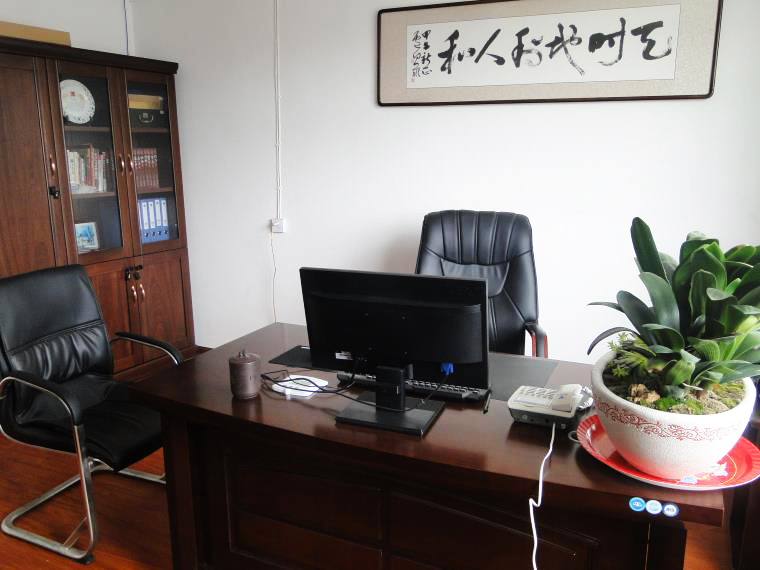
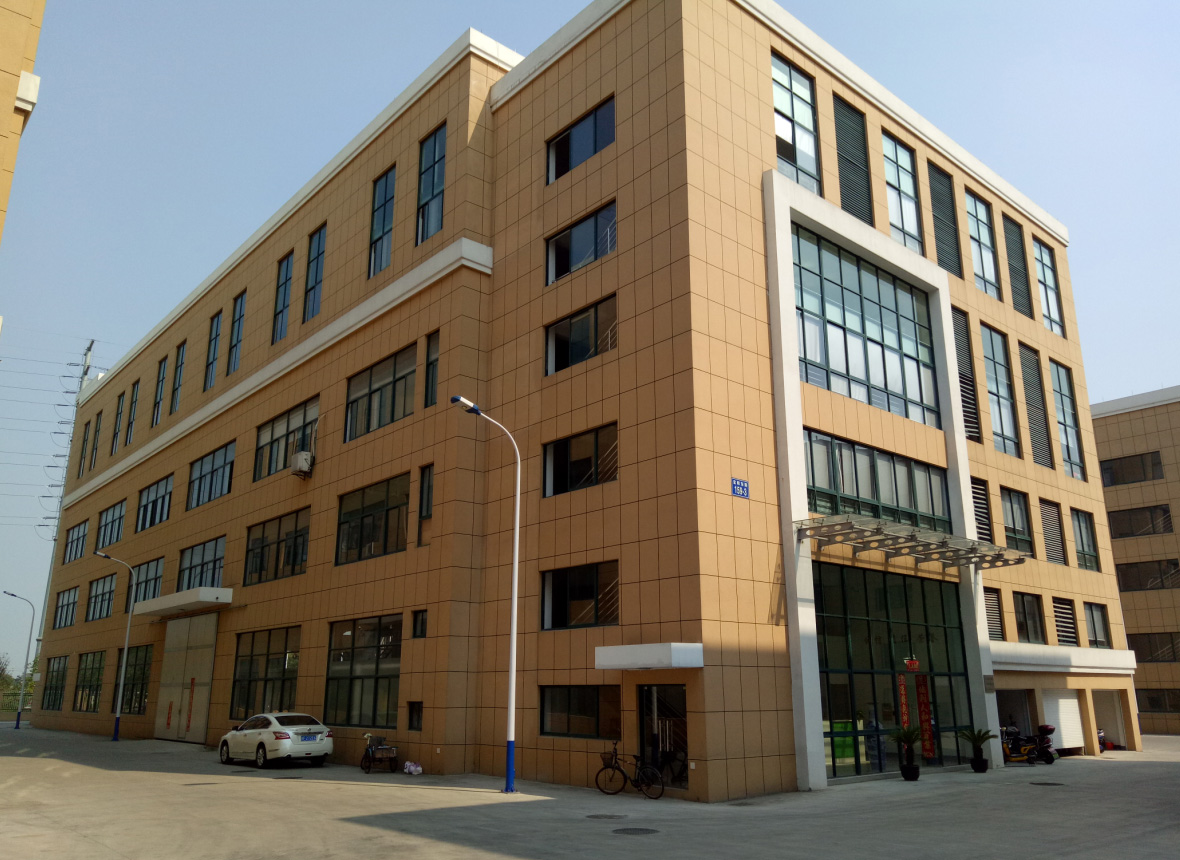
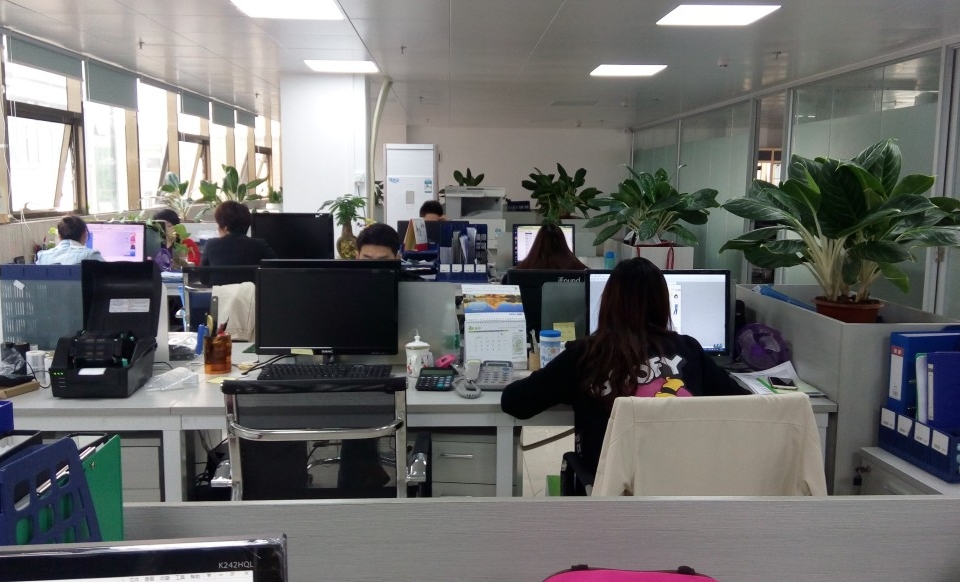
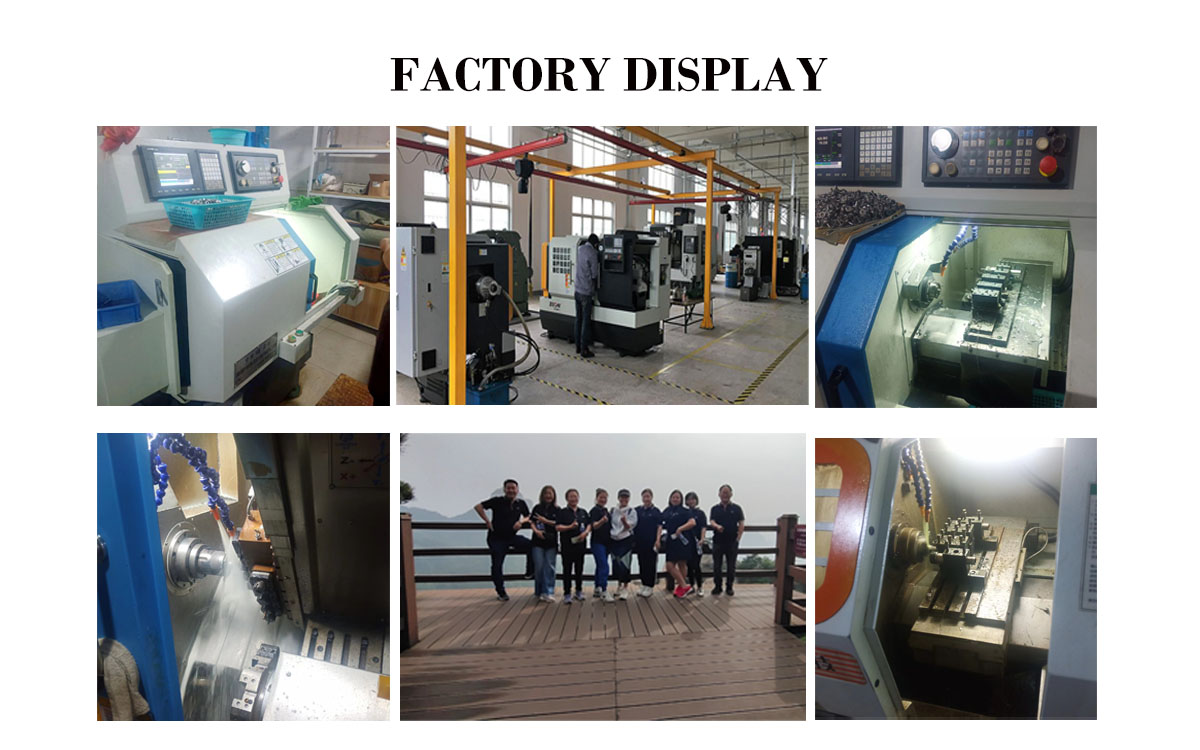
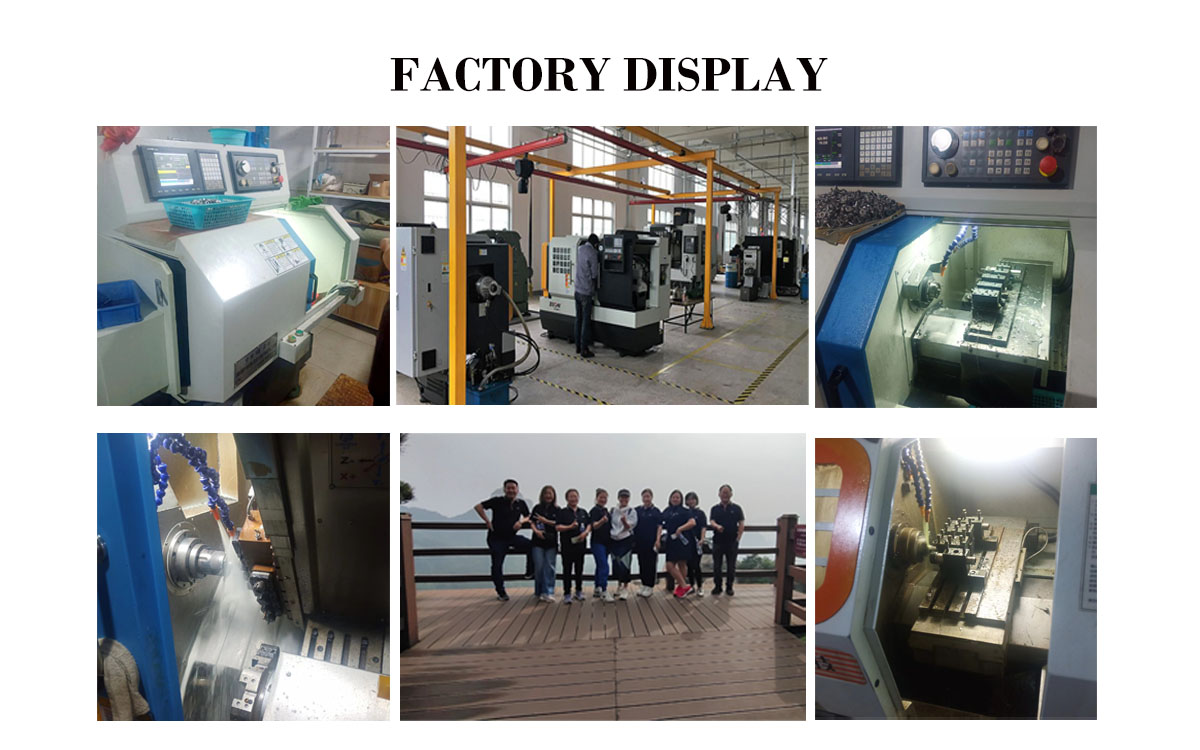
Established in 2015 in Baoji, Shaanxi Province, Verqo Titanium Products Co., Ltd. controls over 2,000 square meters of high-precision CNC multi-axis turning and machining centers. We bridge the critical gap between heavy industrial titanium metallurgy and high-tolerance fastener engineering. Having built a strong international presence across North America, Germany, Japan, Australia, and Southeast Asia, our factory floor pairs rigorous process controls with dynamic OEM/ODM agility.
Direct pipeline sourcing of Grade 5 (Ti-6Al-4V) aerospace bar stock with 100% ultrasonic non-destructive testing for sub-surface voids.
Simultaneous complex geometry machining for eccentric heads, custom cross-drilled lock wire ports, and Torx Plus drive cavities within ±0.005mm.
Dedicated vacuum chamber coating line delivering ultra-consistent Burnt Blue, Oil-Slick Rainbow, Titanium Nitride Gold, and DLC Hard Black.
Bespoke blueprint turnaround with rapid prototype samples delivered within 7 to 10 working days, backed by flexible MOQs starting at 10–50 pieces.
Engineered answers addressing thread engagement, galling mitigation, torque tightening specs, and logistics.
Submit your CAD blueprints, sample components, or OEM bill of materials. Our metallurgy engineering team delivers comprehensive feasibility analyses, tolerance evaluations, and tiered factory-direct price quotations within 2 hours.