Featured Precision Titanium Fastener Series
Manufactured from certified Grade 5 (Ti-6Al-4V) aerospace bar stock with cold-rolled micro-threads, high-torque drive sockets, and wear-resistant PVD or anodized surface finishes.
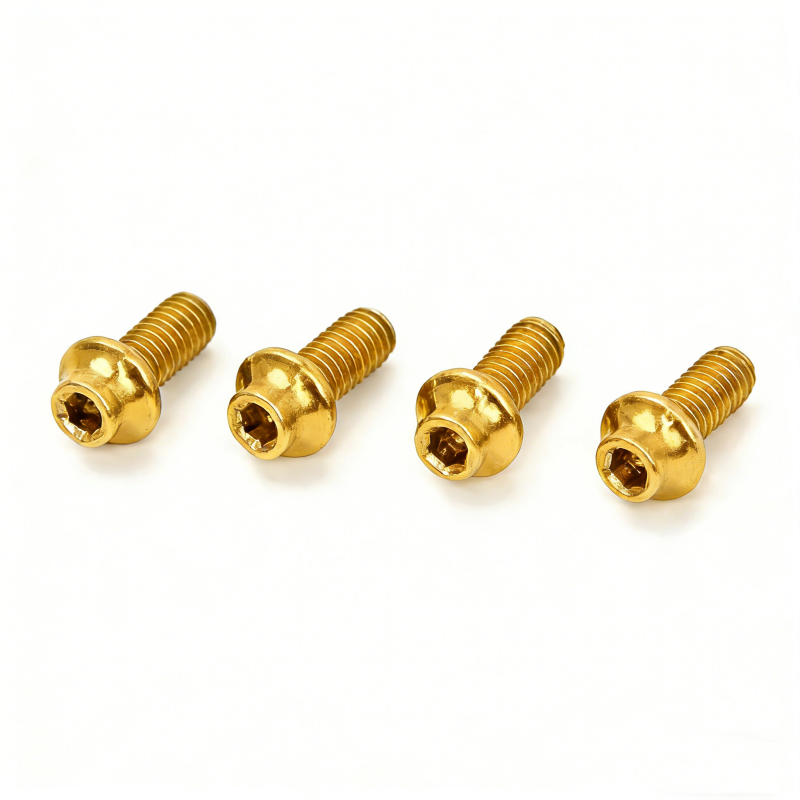
GR5 M2 M3 M4 Anodized Rainbow UFO Cone Head RC Screws
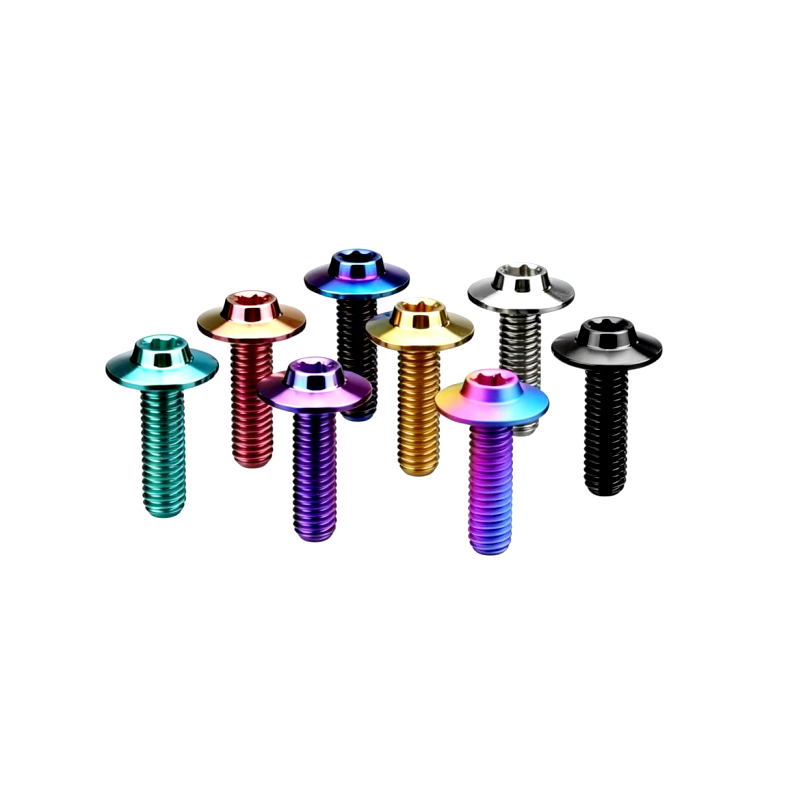
Grade 5 Colorful M6 Umbrella Torx Head Titanium Bolts
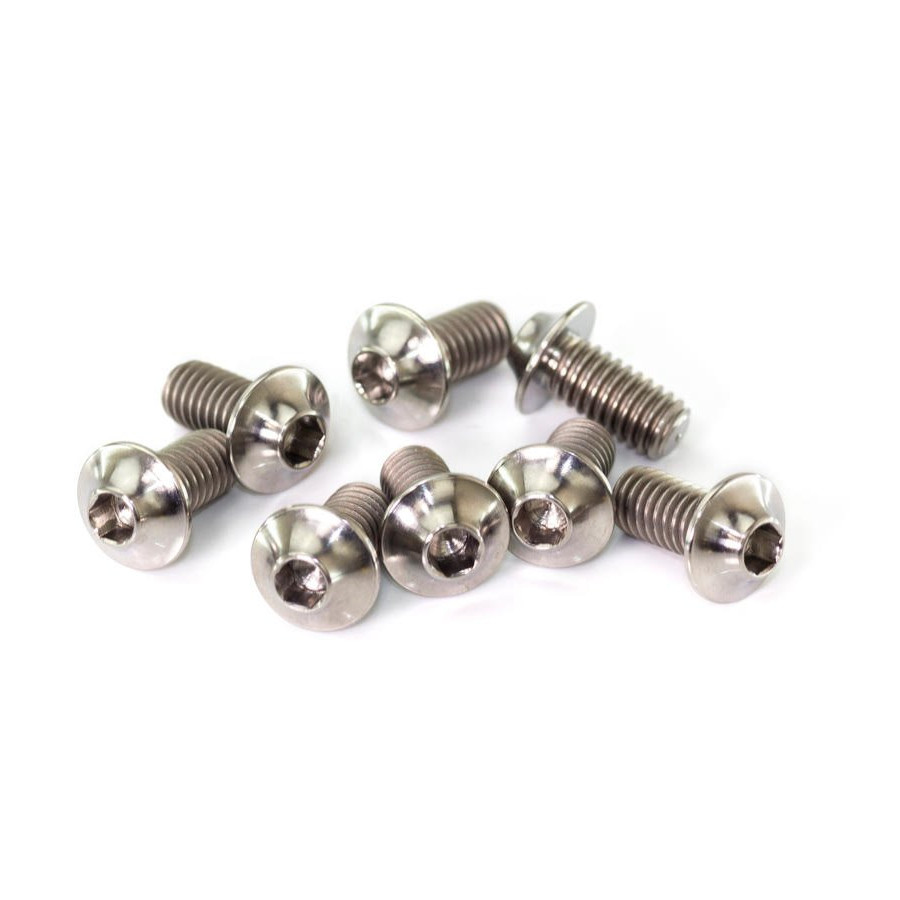
GR5 M3 Metric UFO Cone Head RC & Model Aircraft Screws
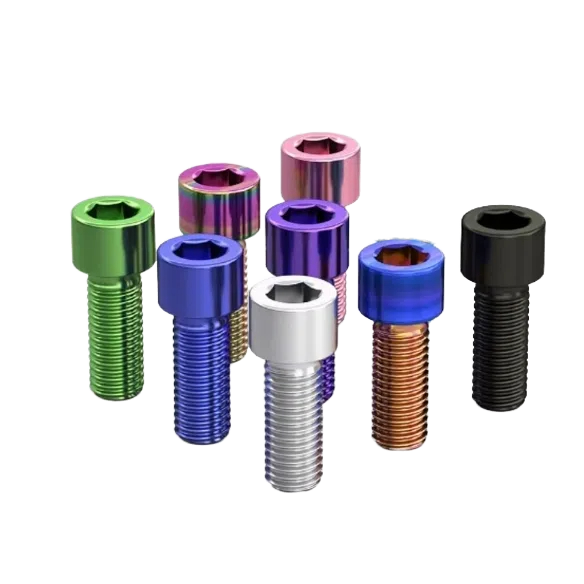
GR5 Anodized M3-M8 Titanium Alloy Socket Cap Bolts
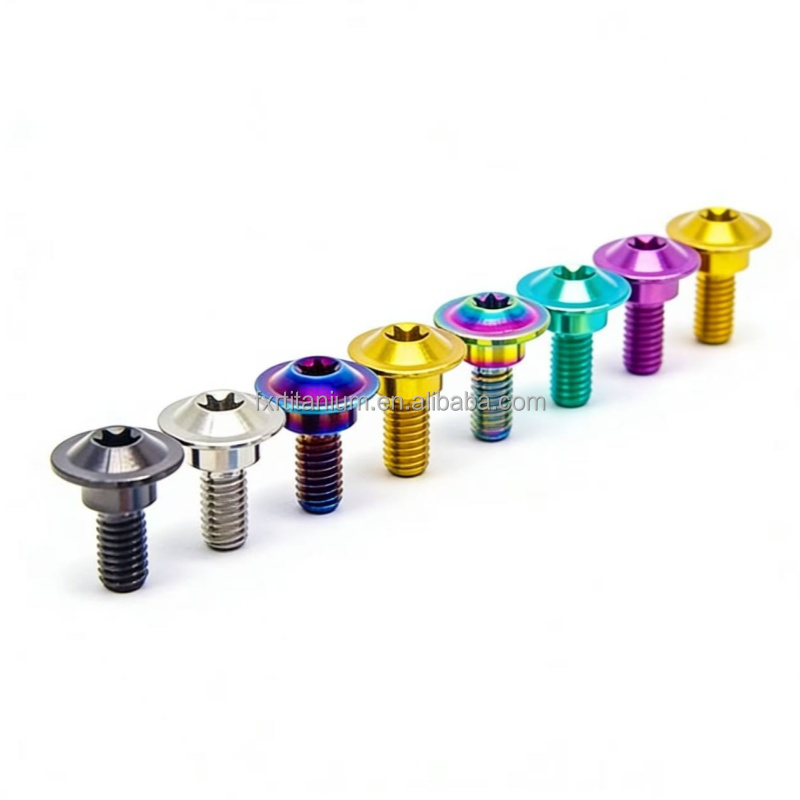
M5 M6 Stepped Disc Head Titanium Fairing Screws
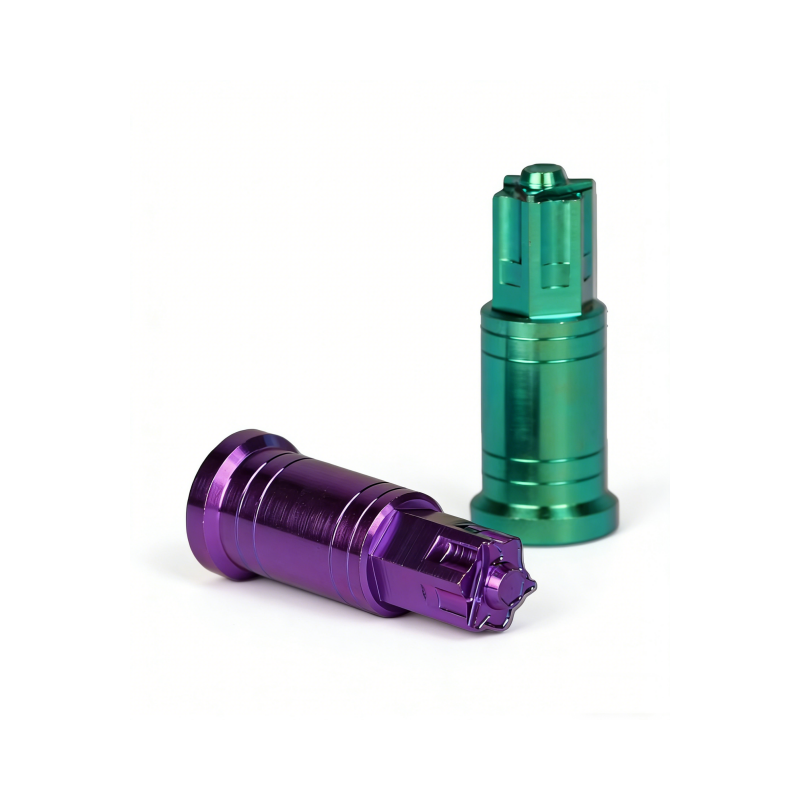
M6 M8 M10 GR5 Titanium Knurled Extended Flange Nuts
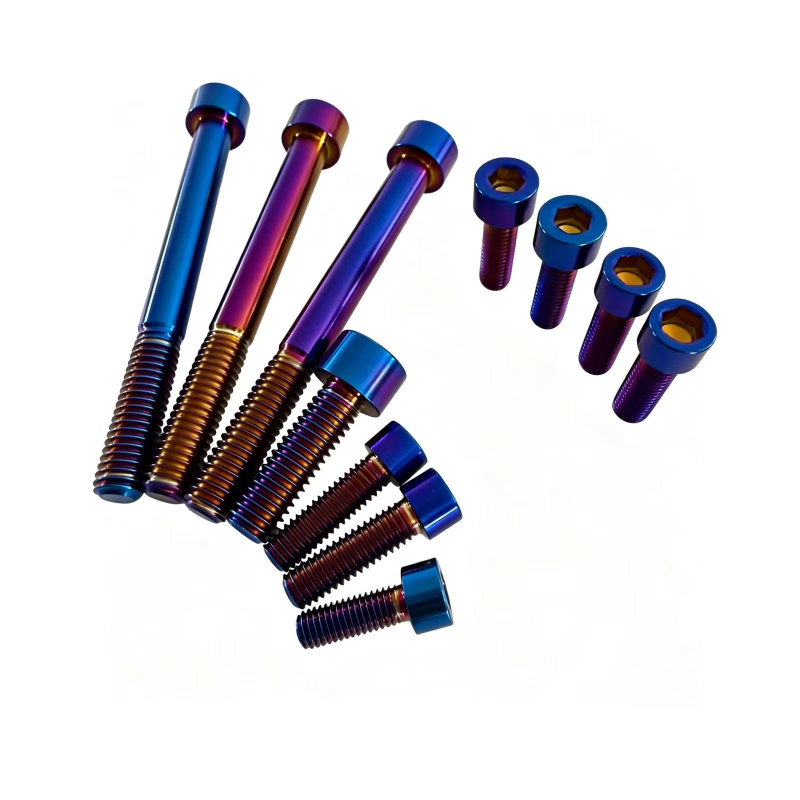
PVD Coated High-Torque Titanium Socket Head Bolts
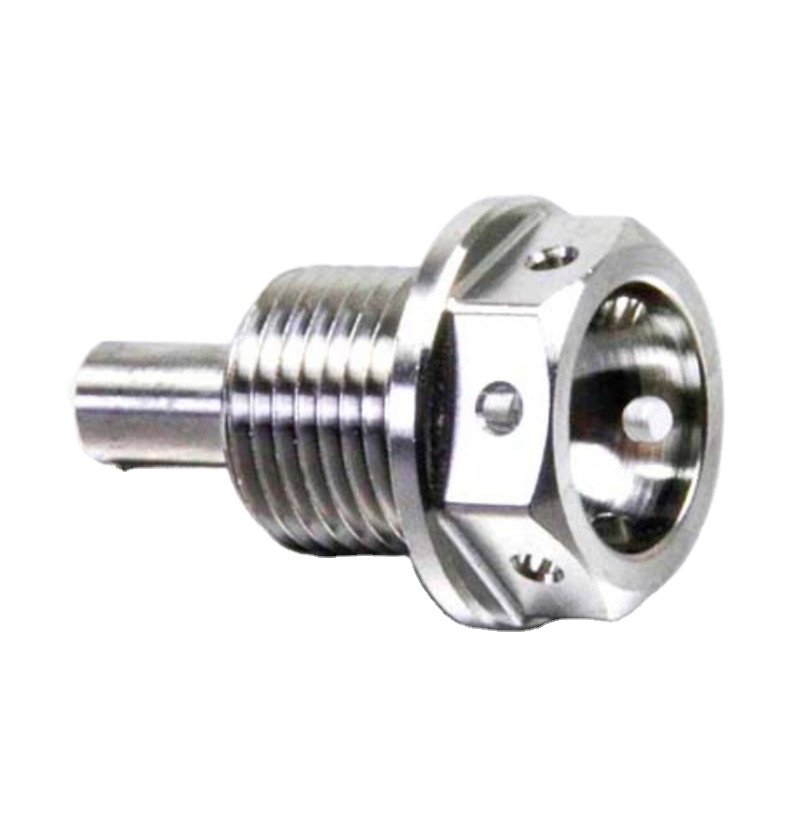
M12–M26 Magnetic Titanium Fluid & Sump Plug Bolts
Physics of Fastener Mass Optimization in Competitive RC Racing
In competitive RC motorsport (encompassing 1/8 nitro off-road buggies, 1/10 electric touring platforms, and multi-rotor high-speed FPV drones), hardware weight is not merely a passive static variable. It fundamentally dictates unsprung rotational inertia, localized center-of-gravity (CoG) coordinate shifts, and high-frequency harmonic vibration dissipation. Standard steel hardware (Classes 8.8, 10.9, and 12.9 carbon/alloy steels) exhibits a mass density of 7.85 g/cm³. While providing high tensile yield, this mass introduces significant parasitic weight at extreme chassis coordinate extremities—specifically shock towers, suspension arms, steering knuckles, and motor mounts.
By transitioning from carbon steel to certified Ti-6Al-4V Grade 5 Titanium (density of 4.43 g/cm³), racing teams achieve an immediate 43.5% reduction in individual screw mass without conceding tensile or shear threshold integrity. When an entire chassis is converted via a full precision-machined titanium hardware kit (typically comprising 120 to 180 fasteners ranging from M2 to M4 in flat head, button head, and UFO configurations), the total dry weight decreases by 45 to 85 grams. Crucially, up to 60% of this saved mass originates above the chassis roll center, drastically mitigating chassis body roll and accelerating suspension rebound frequency over washboard terrain and curbs.
Metallurgical Comparison Matrix: Ti-6Al-4V vs. Alternate Sourcing Alloys
A critical failure mode among inexperienced procurement officers is the conflation of Grade 2 Commercially Pure (CP) Titanium with Grade 5 Ti-6Al-4V Structural Titanium. While Grade 2 titanium offers superior anodizing yield and chemical resistance, its tensile yield point (approx. 275–345 MPa) falls dramatically short of high-speed RC brushless shear loads. Our production strictly utilizes vacuum-arc remelted (VAR) Grade 5 titanium bar stock complying with ASTM B348 and AMS 4928 aerospace criteria.
| Material Specification | Density (g/cm³) | Tensile Strength (MPa) | Yield Strength (MPa) | Shear Strength (MPa) | Dynamic Fatigue Limit |
|---|---|---|---|---|---|
| GR5 Ti-6Al-4V (Verqo Standard) | 4.43 | 895 – 1050 | 828 – 950 | 550 | 510 MPa @ 10⁷ cycles |
| Alloy Steel Grade 10.9 | 7.85 | 1040 | 940 | 620 | 420 MPa @ 10⁷ cycles |
| Grade 2 Commercial Pure (CP) Ti | 4.51 | 345 – 480 | 275 – 350 | 240 | 180 MPa @ 10⁷ cycles |
| 7075-T6 Aircraft Aluminum | 2.81 | 572 | 503 | 331 | 160 MPa @ 10⁷ cycles |
| Stainless Steel A2-70 (AISI 304) | 7.93 | 700 | 450 | 390 | 240 MPa @ 10⁷ cycles |
Fatigue Resistance: Cold-Rolled vs. Machine-Cut Thread Microstructures
The primary vulnerability of small-diameter metric fasteners (M2, M2.5, M3, and M4) subjected to continuous brushless vibrations and high shock loads is shear fatigue at the thread root. Substandard manufacturers utilize single-point cutting or thread chasers on CNC lathes to machine miniature external threads. This practice severs the crystalline grain structure of the titanium alloy, establishing micro-notches that act as primary stress concentrators.
Verqo eliminates this vulnerability by implementing precision cylindrical die cold-thread rolling post-CNC turning. Cold thread rolling does not remove metal; instead, it plastically displaces the titanium grain boundary contours, compressing the material into uninterrupted radial grain flows conforming exactly to the root and crest radii. This cold working process introduces beneficial compressive residual stresses along the thread root, enhancing fatigue resistance by over 300% and virtually eliminating stripping failures under extreme landing stress.
Future Sourcing & Procurement Trends (2025–2030)
How international RC manufacturers, professional racing syndicates, and aerospace robotics integrators are reshaping their fastener supply chain parameters.
Migration to Torx (Hexalobular) Drives
Traditional Hex (Allen) sockets in M2 to M3 screws round out rapidly under repeated track-side servicing with electric screwdrivers. Sourcing trends show an 82% pivot toward Hexalobular (Torx T6, T8, T10) geometries, which provide zero cam-out, higher torque transfer, and extended tool life.
Consolidated Kit-Based Procurement
B2B distributors are moving away from sourcing bulk individual SKU polybags toward model-specific, laser-etched hardware kits tailored for platforms such as Mugen Seiki, Team Associated, XRAY, and Traxxas. Verqo offers automated counting, sorted sorting trays, and custom branding.
Advanced PVD & DLC Vacuum Deposition
While traditional electrochemical anodizing provides aesthetic coloring, racing conditions demand abrasion-proof coatings. Multi-arc vacuum Physical Vapor Deposition (PVD) yields Diamond-Like Carbon (DLC), Titanium Nitride (TiN), and Rainbow finishes with surface hardness surpassing 2,500 HV.
Technological Advancements in RC Fastener Manufacturing
From raw material traceability in China's Titanium Valley to sub-micron optical sorting systems.
High-Speed Swiss CNC Turning
Utilizing high-precision multi-axis Swiss-type automatic lathes enables simultaneous profiling, head shaving, and socket broaching in a single clamping setup, guaranteeing concentricity within 0.005mm.
UFO Low-Profile Aerodynamics
Verqo's proprietary UFO Cone Head designs feature an ultra-thin, radiused flange head that sits flush against carbon fiber shock towers and chassis bottom plates, preventing snagging on track surface borders.
100% Optical Glass Disc Sorting
To support high-volume automated robotic assembly lines, our fasteners undergo automated rotary glass disc inspection machines. Every screw is evaluated by multi-camera vision sensors for pitch, length, and concentricity at 600 ppm.
Anti-Galling Chemical Passivation
Titanium threads have a natural tendency to gall against aluminum bulkheads or titanium lock nuts. We implement specialized vacuum chemical passivation and optional dry-film MoS₂ lubricants to stabilize friction coefficients.
Verqo Titanium: China's "Titanium Valley" Manufacturing Powerhouse
Combining 10+ years of precision export experience, raw material supply security, and state-of-the-art manufacturing facilities.
Cluster Advantage: Baoji, Shaanxi
Located in China's Titanium Valley, Verqo enjoys direct access to over 80% of the nation's premium grade titanium sponge and smelting resources, ensuring unbeatable raw material pricing stability and consistent alloy lot traceability.
1,001–2,000 m² CNC Facility
Equipped with Swiss-type CNC lathes, thread rolling machinery, multi-axis machining centers, and comprehensive in-house anodizing and PVD coating departments, staffed by 11 to 50 dedicated titanium engineering specialists.
≤ 2-Hour Response & 98.6% Rate
Global client projects receive agile turnaround times. Our engineering-led international sales division maintains an average communication response time of ≤ 2 hours with an industry-leading 98.62% response rate.
Flexible OEM MOQ & Traceability
Unlike rigid industrial fastener mills, our MOQ starts at just 10–20 pieces for stock series, and 50–100 pieces for bespoke custom prototype drawings, complete with EN 10204 3.1 chemical and mechanical inspection certificates.
Frequently Asked Questions (FAQ)
Crucial engineering, metallurgical, and international B2B purchasing questions answered by our technical specialists.
Q: Why is Grade 5 (Ti-6Al-4V) mandatory over Grade 2 Titanium for RC chassis screws?
Grade 2 Commercial Pure (CP) titanium has an ultimate tensile strength of only 345–480 MPa and a yield strength under 300 MPa, comparable only to low-grade mild steel. Under the high shock loads of 1/8 nitro buggy jumps, Grade 2 screw heads will shear or shear across their drive sockets. In contrast, Grade 5 (Ti-6Al-4V) is an alpha-beta alloy delivering tensile strengths between 895 and 1050 MPa and yield strengths exceeding 828 MPa, effortlessly handling severe off-road bash landings and high-torque electric motor mounts.
Q: How do you prevent thread galling (cold welding) during assembly into aluminum bulkheads?
Titanium has a very thin, naturally occurring oxide film that can break down under high friction contact with aluminum or stainless steel, causing micro-friction welds known as galling. Verqo prevents this through precise thread flank finishing and dimensional tolerance control. For end-users, we recommend applying a micro-drop of fluoropolymer grease, anti-seize paste, or medium-strength blue threadlocker, which acts as a physical barrier preventing direct metal-on-metal galling while securing the fastener under vibration.
Q: Can you produce custom head dimensions according to 2D/3D CAD drawings (e.g., STEP/DWG)?
Yes. Custom OEM/ODM manufacturing represents over 60% of our production volume. Whether you need ultra-low UFO cone heads, integrated washer flange heads, or hollow-core weight-relieved turnbuckle studs, our Swiss CNC lathes and cold-heading tooling can produce custom geometries from M1.6 up to M26 with tight tolerances held to ±0.005mm.
Q: What is the difference between your Anodized finishes and PVD Vacuum Plated finishes?
Anodizing is an electrochemical process that grows the titanium's natural dioxide (TiO₂) interference layer to create vibrant optical colors (gold, electric blue, purple, green, rose, and rainbow) without adding pigment or dimensional thickness. PVD (Physical Vapor Deposition) is a high-vacuum plasma deposition process that bonds an ultra-hard ceramic compound (like TiN or Diamond-Like Carbon) to the surface. PVD provides superior scratch resistance, high surface hardness (>2500 HV), and deep metallic black or iridescent chameleon tones.
Q: What thread size standards and drive configurations do you manufacture?
Our metric tooling encompasses standard coarse pitches from M1.6, M2, M2.5, M3, M3.5, M4, M5, up to M26. We support Hexagonal socket (Allen), Torx (Hexalobular T6 through T30), Phillips, Slotted, and custom dual-drive configurations (outer hex with inner Torx). For sprint cars and US automotive customers, imperial UNC/UNF threads (such as #4-40, #6-32, 1/4"-20) are readily available.
Q: What documentation and quality inspection reports are included with bulk export shipments?
Every batch includes full traceability documentation: EN 10204 Type 3.1 Material Test Reports (MTR) verifying chemical composition (Ti balance, Al 5.5-6.75%, V 3.5-4.5%, Fe < 0.3%, O < 0.2%) and mechanical tensile test data, Full Dimensional Inspection Reports using optical CMM equipment, and Surface Coating Thickness certificates upon client request.
Q: What are your standard lead times and accepted international B2B payment terms?
In-stock screws ship within 24 to 48 hours. Custom CNC machined orders or custom anodized batches typically require 10 to 18 business days depending on tooling complexity and volume. We support international wire transfer (T/T), Letter of Credit (L/C), PayPal for rapid sampling, and Western Union, with global delivery via FedEx, DHL Express, air cargo, or ocean freight.