Aerospace Gr5
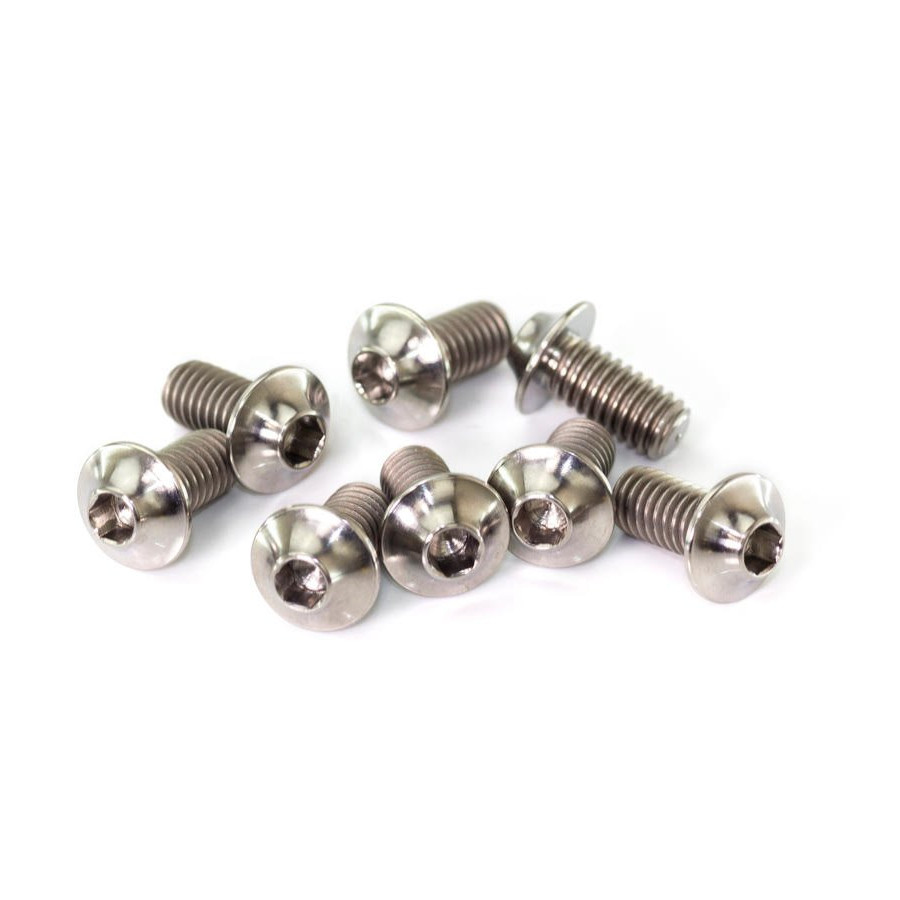
Manufactured directly within our Baoji facility utilizing multi-axis CNC machining, cold rolled threads, and magnetron PVD coating. Designed for critical load retention in high-vibration applications.
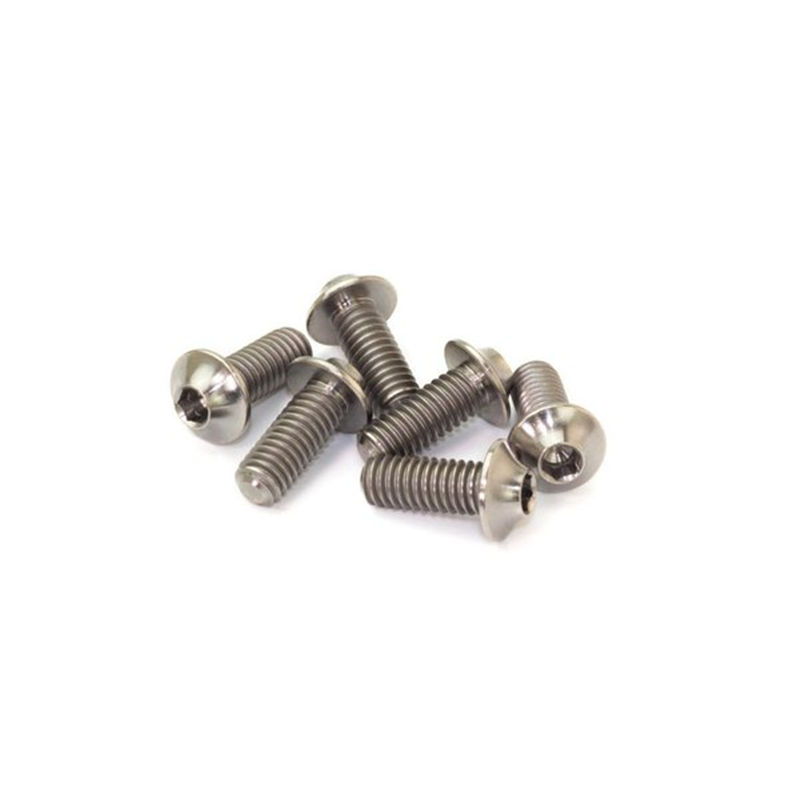
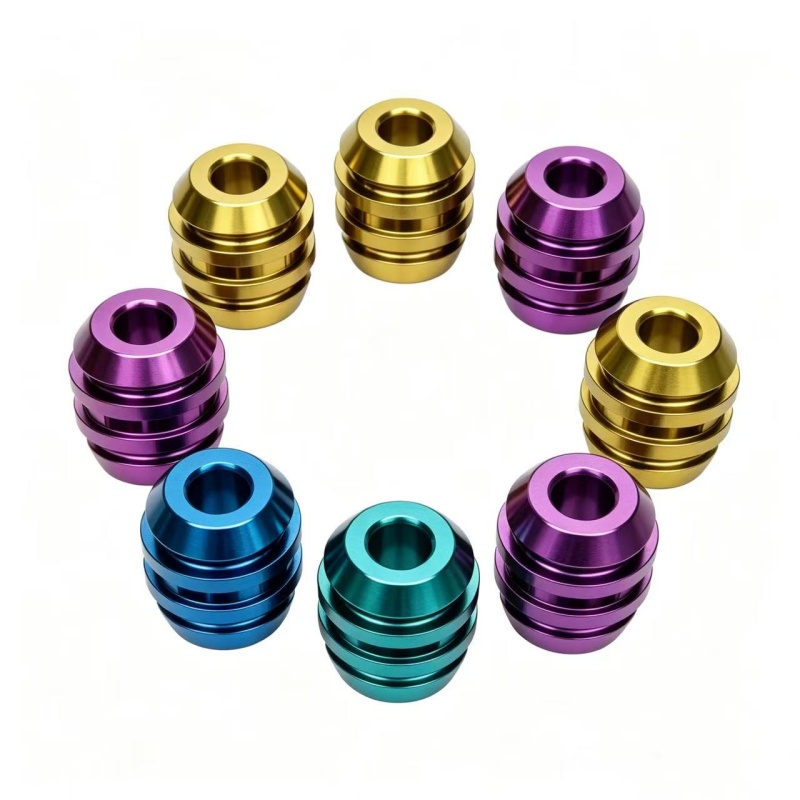
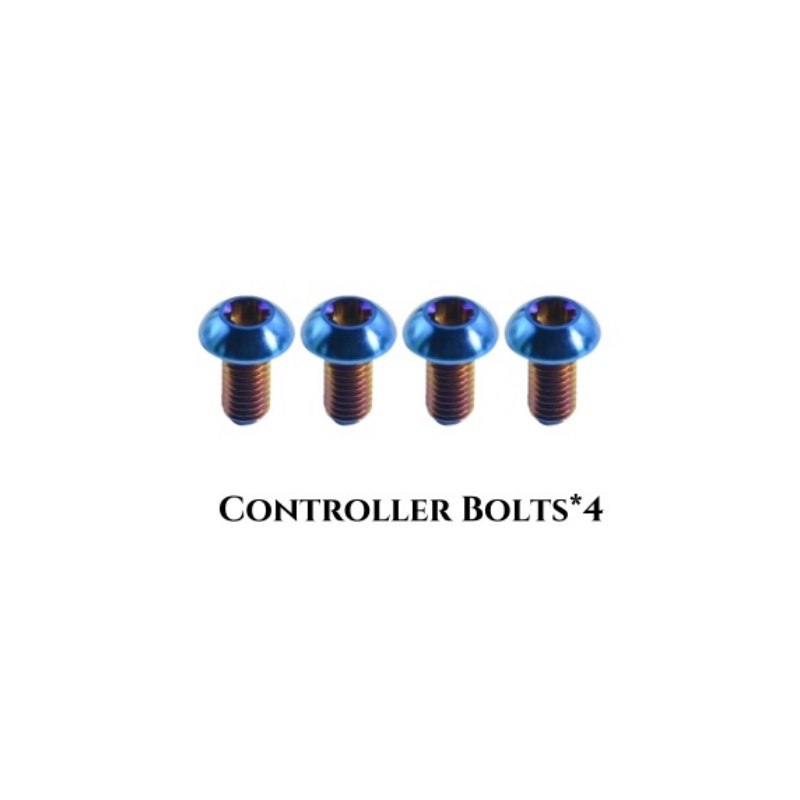
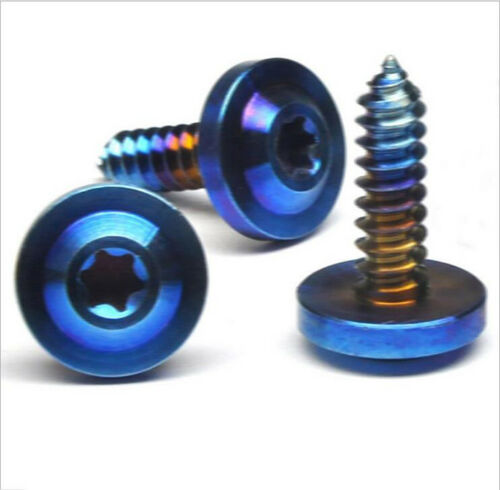
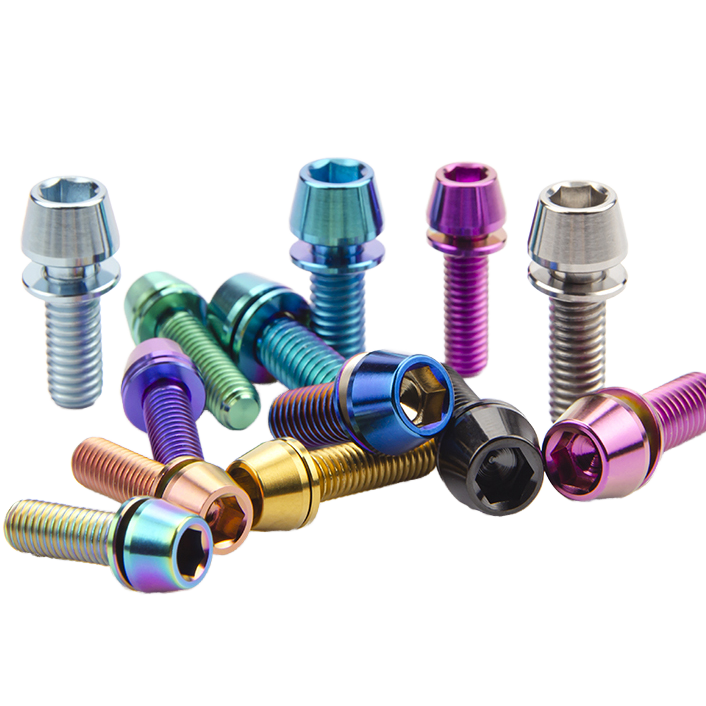
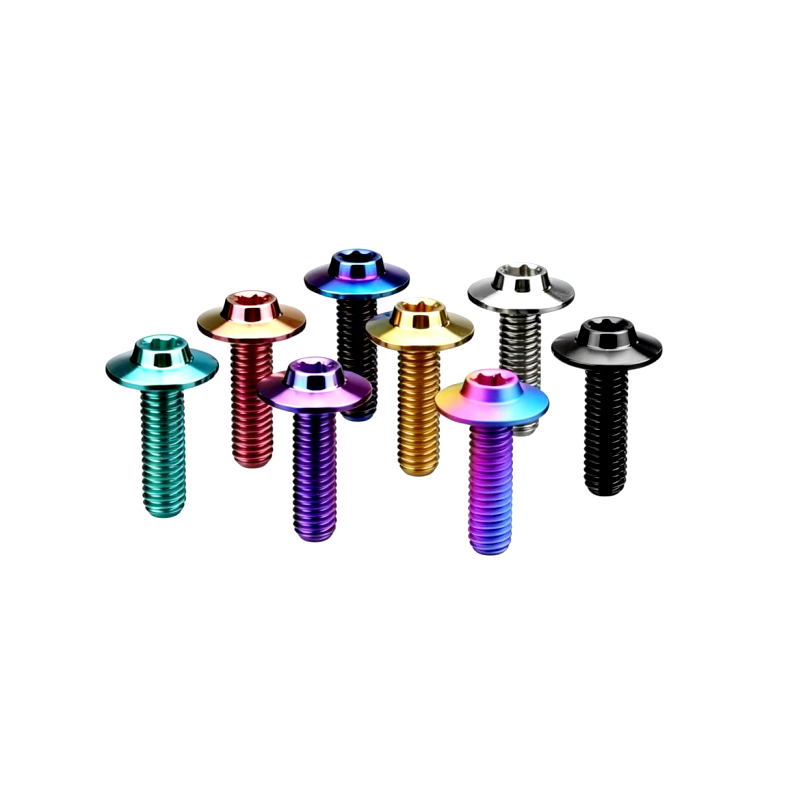
In competitive cycling and high-end cockpit manufacturing, bicycle stem bolts are the most critical safety fasteners on the entire frame assembly. A single fastener failure on a 4-bolt faceplate or a dual-bolt steerer binder leads directly to catastrophic steering failure. Here is how our OEM/ODM titanium stem bolts solve cyclic fatigue, galvanic corrosion, and micro-fretting.
Our OEM/ODM manufacturing strictly utilizes genuine Ti-6Al-4V Grade 5 (UNS R56400 / ASTM B348 / AMS 4928) rather than substandard Grade 1 or Grade 2 commercially pure (CP) titanium. While CP titanium exhibits excellent corrosion resistance, its yield strength (approx. 275–345 MPa) is dangerously insufficient for bicycle handlebar faceplate clamp preloads.
By alloying 6% Aluminum (alpha-phase stabilizer) and 4% Vanadium (beta-phase isomorphous stabilizer), Ti-6Al-4V creates a fine-grained microstructure that yields an ultimate tensile strength exceeding 950–1050 MPa and a yield strength over 880 MPa. This translates into roughly 43% weight savings over 10.9-grade carbon steel fasteners, while possessing an almost infinite fatigue threshold under typical cycling preloads.
When combined with our cold thread rolling technology, the grain flow of the alloy follows the root contour continuously rather than being interrupted by lathe turning, preventing stress risers and eliminating fatigue initiation points along the thread roots.
| Mechanical Parameter | Ti-6Al-4V (Grade 5) | Class 10.9 Steel | 7075-T6 Alloy |
|---|---|---|---|
| Density (g/cm³) | 4.43 | 7.85 | 2.81 |
| Tensile Strength (MPa) | 950 - 1050 | 1040 | 570 |
| Yield Strength (MPa) | 880 - 920 | 940 | 505 |
| Elastic Modulus (GPa) | 114 | 210 | 72 |
| Fatigue Limit (10⁷ Cycles) | 510 MPa | 420 MPa | 160 MPa |
| Galvanic Potential in Carbon | Inert / Neutral | Severe Rust Risk | Galvanic Oxidation |
| Stem Bolt Spec | Drive Standard | Head Profile | Recommended Max Torque |
|---|---|---|---|
| M5 x 16mm | Torx T25 / Hex 4mm | Tapered Socket / UFO | 5.2 – 6.0 N·m (Lubricated) |
| M5 x 18mm | Torx T25 / Hex 4mm | Integrated Washer Din 912 | 5.5 – 6.2 N·m (Lubricated) |
| M6 x 18mm | Torx T30 / Hex 5mm | Flanged / Tapered Head | 8.5 – 9.8 N·m (Lubricated) |
| M6 x 20mm | Torx T30 / Hex 5mm | Race-Spec Drilled Hex | 9.0 – 10.5 N·m (Lubricated) |
One of the chief reasons OEM bicycle brands partner with Verqo is our solution to the classic titanium tribological dilemma: galling. Titanium has a natural passivating titanium dioxide (TiO₂) film that can cold-weld to internal aluminum stem threads under dry, high-load torque conditions.
We overcome this through three simultaneous manufacturing engineering advances:
1. Controlled Precision Rolling: Ensuring surface roughness (Ra) along thread flanks is kept below 0.4 µm.
2. Vacuum PVD Hard Coatings: Depositing sub-micron layers of Titanium Nitride (TiN) or Diamond-Like Carbon (DLC) that significantly lower friction coefficients (µ drops from ~0.35 to under 0.12).
3. Spherical Floating Washer Architectures: We supply matching GR5 titanium concave washers that distribute clamping loads uniformly across carbon fiber faceplates, eliminating concentrated point loading and preserving composite fiber matrix integrity under aggressive sprint out-of-the-saddle twisting forces.
Global supply chain directors and brand product managers face shifting dynamics in alloy raw material pricing, integrated cockpit aerodynamics, and sustainability mandates. Below are the 3 major procurement shifts shaping B2B orders over the next 5 years.
Global bicycle brands are moving away from multi-tier brokerage models. In 2025 and beyond, direct engagement with vertically integrated manufacturing plants in China's "Titanium Valley" (Baoji) has become essential for supply chain resilience. Direct factory contracts secure raw sponge titanium prices, reduce lead times from 16 weeks to under 4 weeks, and guarantee material batch test reports (MTR EN 10204 3.1) directly from the mill source.
As road racing, gravel bikes, and modern e-bikes universally adopt fully hidden internal cable routing (ICR), the clearance envelope inside stem faceplates and headset compression systems has shrunk dramatically. OEM buyers are no longer sourcing generic DIN 912 socket bolts; they require bespoke low-profile UFO heads, countersunk Torx fasteners, and hollow-shank designs that fit within narrow composite cavities without interfering with hydraulic braking lines.
Western bicycle and sports equipment conglomerates (EU & North America) are heavily scrutinizing supply chain environmental footprints. The transition from chemical-heavy toxic electroplating to eco-friendly electrochemical anodizing and non-polluting Vacuum Magnetron Physical Vapor Deposition (PVD) is now a mandatory vendor qualification check. Furthermore, full documentation for RoHS, REACH SVHC, and Conflict Minerals is now required prior to port clearance.
How advanced cold-forging, multi-axis Swiss CNC turning, and precision surface nanotechnology have redefined modern bicycle fastener integrity.
Historically, titanium stem bolts were either fully CNC turned from solid bar stock (which wastes up to 70% of material and cuts through metal grain lines) or hot-forged with high thermal oxidation. Modern Tier-1 production utilizes high-speed cold-heading machines to form the bolt head and roll threads, followed by sub-micron 5-axis Swiss-lathe finishing for drive socket precision (Torx T25/Hex 4mm). This yields unbroken grain lines, higher tensile yield, and reduces cost-per-part on high-volume runs.
While traditional electrochemical anodizing creates vibrant colors (gold, blue, purple) by altering light interference on the titanium oxide layer, it provides minimal abrasion resistance. Verqo has introduced industrial magnetron sputtering PVD vacuum coating. By depositing Titanium Aluminum Nitride (TiAlN) or CrN layers at atomic levels, stem bolts achieve surface hardness values exceeding 2200–2800 HV, resisting wrench-slip roundings and abrasive weather exposure indefinitely.
Bicycle cockpits operate under high dynamic fatigue; an improperly formed thread pitch or burr can lead to inaccurate torque readings during assembly. We have integrated 360-degree glass plate automated optical inspection (AOI) sorting machines. Every single bolt in OEM mass-orders is inspected for thread runout, pitch diameter (6g metric standard), head concentricity, and socket depth at speeds up to 400 parts per minute, eliminating assembly line defects.
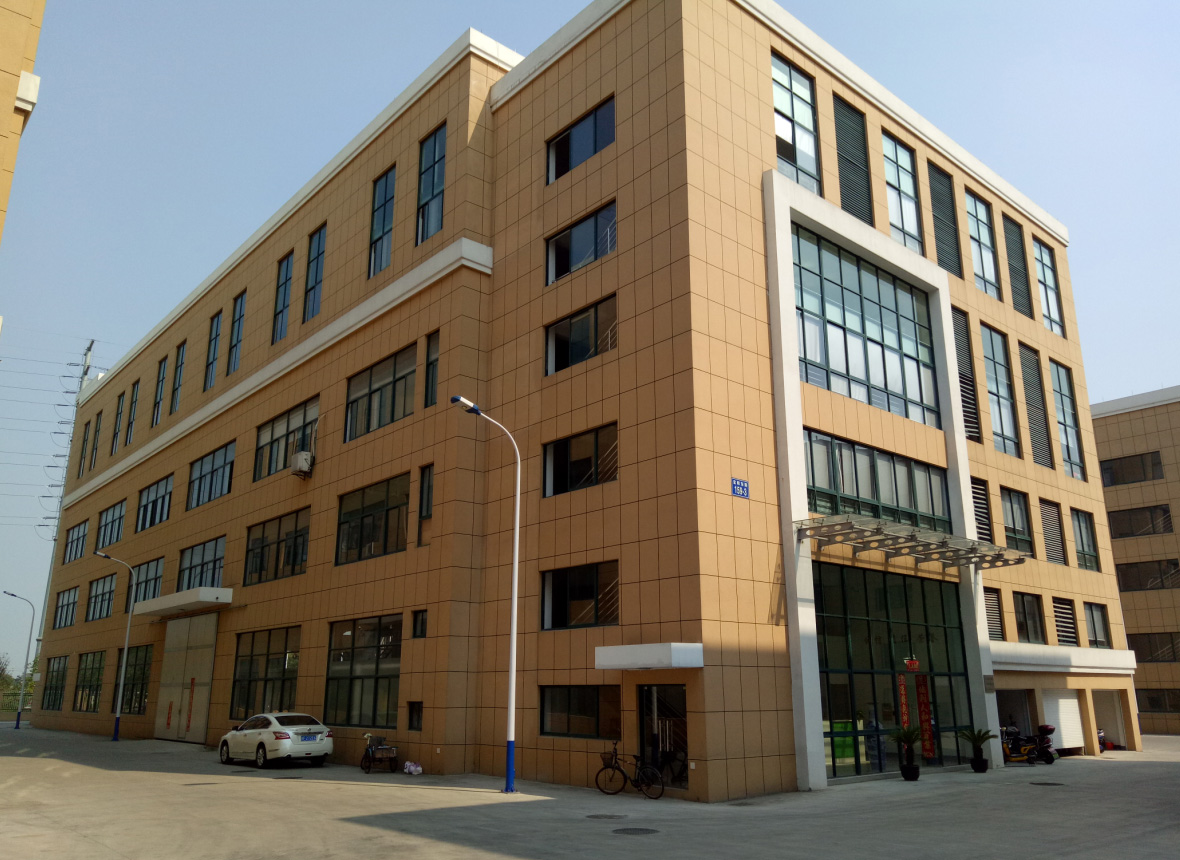
Headquartered in Baoji, Shaanxi Province — the epicentre of China's titanium supply chain — Verqo Titanium Products Co., Ltd. has specialized in precision titanium fasteners and custom CNC components since 2015.
Direct supply contracts with domestic titanium melting centers give us uninterrupted access to military- and medical-grade Ti-6Al-4V bar stock with lower raw material costs.
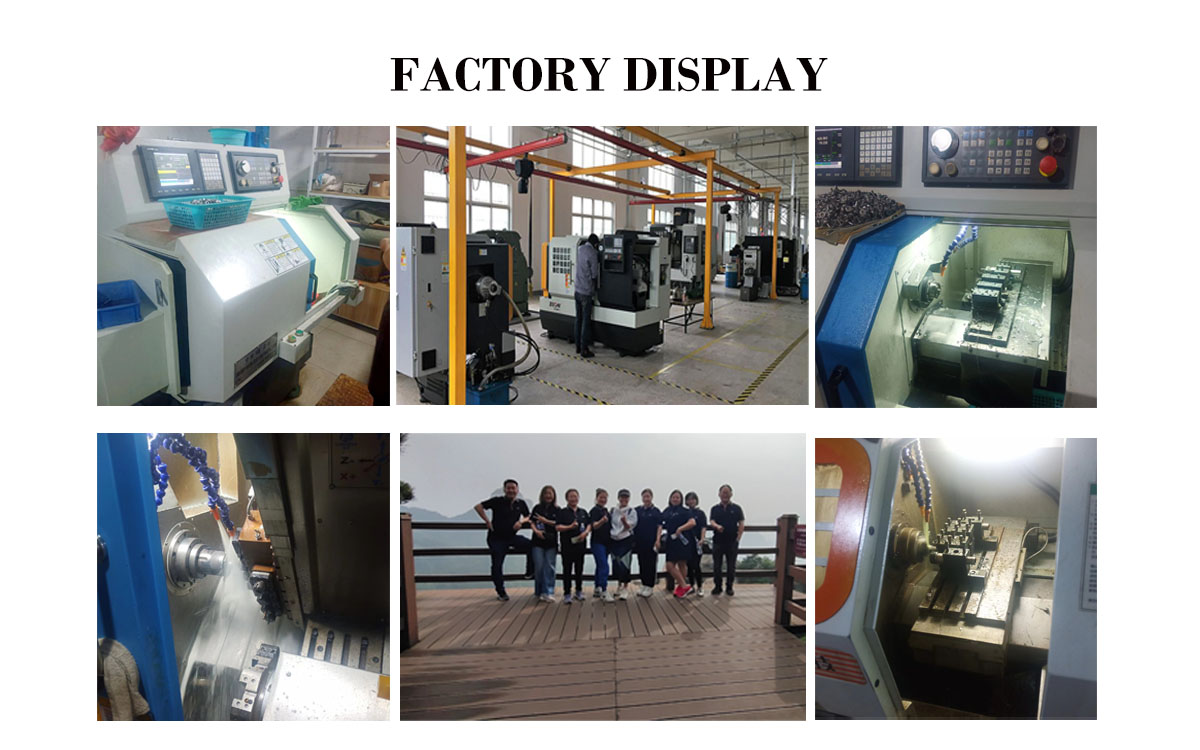
Operating across 1,001–2,000 m² of modern production space equipped with multi-axis Swiss turning centers, cold-heading lines, thread rollers, and vacuum furnaces.
Our team of 11–50 precision specialists provides direct DFM (Design for Manufacturability) analysis, 3D CAD/STEP reviews, and prototype turnarounds in under 7 business days.
We accommodate both boutique brand custom builds (MOQ starting at just 50–100 pieces) and high-volume OEM factory contracts with flexible T/T, L/C, and PayPal terms.
Essential technical, financial, and logistical details to know before submitting your RFQ for titanium stem bolts and custom cockpit hardware.
Every batch of raw bar stock entering our Baoji shop undergoes spectral chemical analysis and mechanical tensile testing. We provide EN 10204 3.1 Mill Test Certificates confirming chemical composition (Al: 5.5-6.75%, V: 3.5-4.5%, Fe: ≤0.30%, O: ≤0.20%, Ti balance) and yield strength verification with every shipment.
The global bicycle industry standard for 4-bolt stem faceplates and 2-bolt steerer clamps is primarily M5 x 0.8mm pitch with lengths of 16mm or 18mm (conforming to DIN 912 or low-profile tapered cone designs). Certain enduro, downhill, and BMX stems utilize heavy-duty M6 x 1.0mm pitch in 18mm or 20mm lengths. We stock both metric and custom UNC pitches.
For all structural, load-bearing stem and rotor bolts, we strictly produce cold rolled threads. Thread rolling deforms the alloy grains continuously across the flanks and root radii, hardening the surface and providing up to 30% higher fatigue resistance compared to single-point CNC cut threads which introduce micro-notches susceptible to fatigue cracking.
When installing titanium stem bolts into aluminum faceplates, threaded inserts, or carbon stems, we mandate applying a copper-based or molybdenum disulfide (MoS₂) anti-seize paste. This stabilizes the friction coefficient at ~0.10–0.12, ensures accurate torque wrench tensioning, and entirely eliminates thread galling under cyclic bar-lever stress.
We offer precision mirror polishing, matte bead-blasting, chemical anodizing (gold, royal blue, ultraviolet, emerald green, and fire-burnt blue), and heavy-duty PVD vacuum coatings (DLC jet black, rainbow oil-slick, and chrome gold). High-resolution laser engraving for OEM brand logos and torque indicators (e.g., "MAX 5.2 N·m") is executed in-house.
For standard off-the-shelf specs (M5x16/18, M6x18/20 raw polished or common anodized colors), our MOQ starts at only 10 to 50 pieces with 48-hour dispatch. For bespoke OEM drawings (custom head shapes, unique threading, or specialized PVD colors), our MOQ is typically 100 to 500 pieces, with tooling and sample delivery in 7–10 days and mass production in 2–3 weeks.
Submit your 2D/3D engineering drawings (DWG, STEP, IGES) or specify your required thread dimensions, head style, finish, and estimated volume. Our senior fastener engineers will reply with a comprehensive DFM assessment, formal quotation, and sample prototype schedule within 2 hours.