Precision Titanium Components & EDC Hardware Catalog
Explore our flagship Ti-6Al-4V precision-manufactured series. From high-tensile rotor hardware and aerospace coil springs to custom tactical knife accessories, our state-of-the-art CNC machining facility delivers uncompromised micro-tolerances and exceptional anti-corrosive performance.
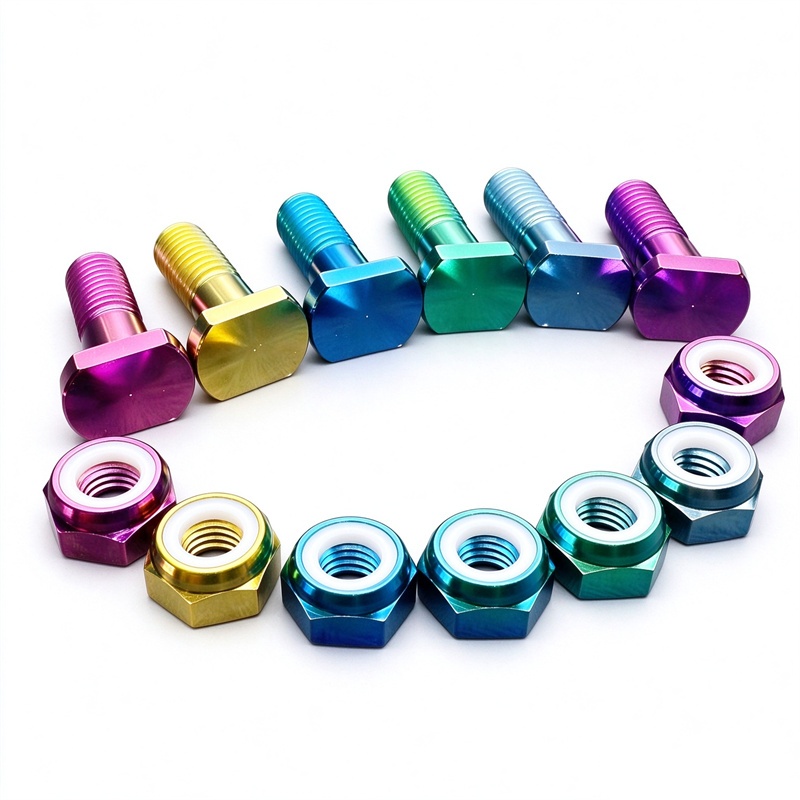
Gr5 Ti-Alloy Disc Rotor Bolt & Nut for Ducati
Ultra-lightweight titanium rotor hardware featuring high tensile strength exceeding 895 MPa, rolled metric threads, and chemical-passivated rainbow PVD.
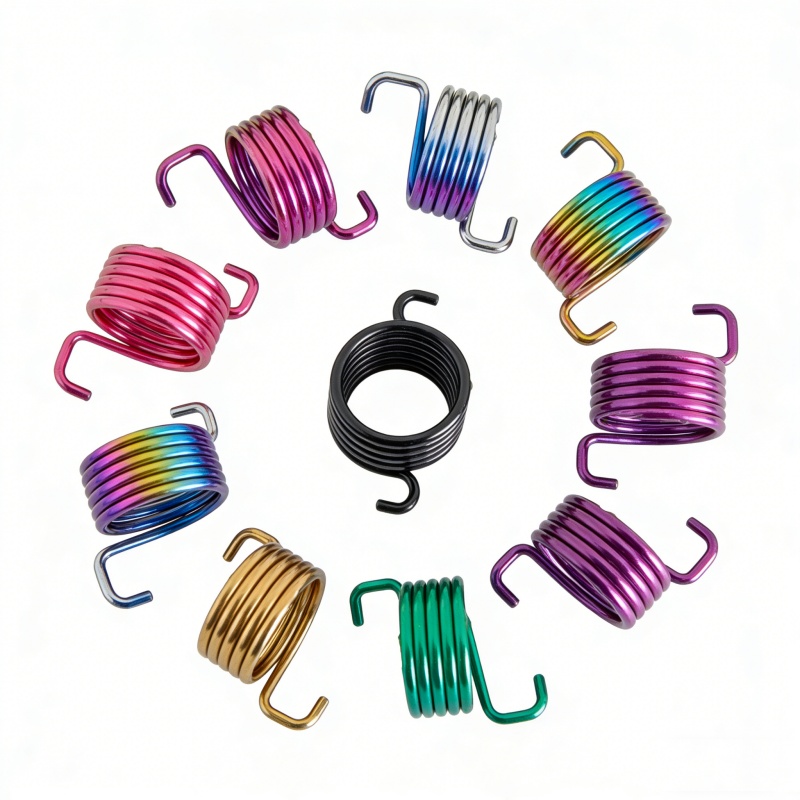
Titanium Footpeg Torsion Coil Springs (25 lb Load)
Aerospace-grade coil torsion springs designed for extreme torsional fatigue resistance, zero salt-spray corrosion, and sustained dynamic recoil performance.
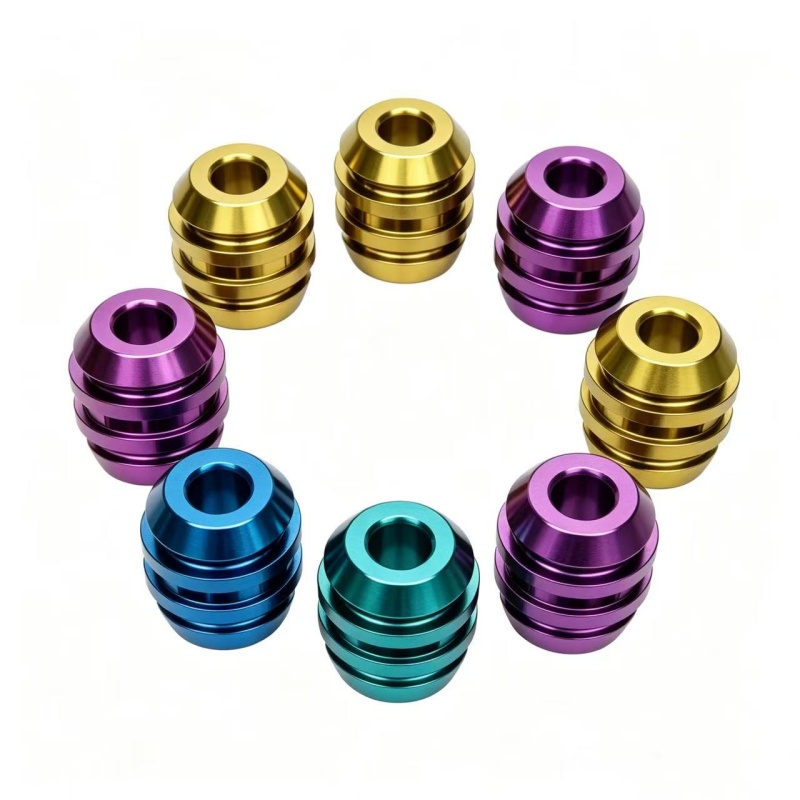
FOXTI Gr5 Titanium EDC Knife Lanyard Beads
Precision CNC-turned and milled 6mm/8mm hole tactical lanyard beads with multi-spectrum PVD vacuum coating, chamfered lanyard paths, and tactile jimping.
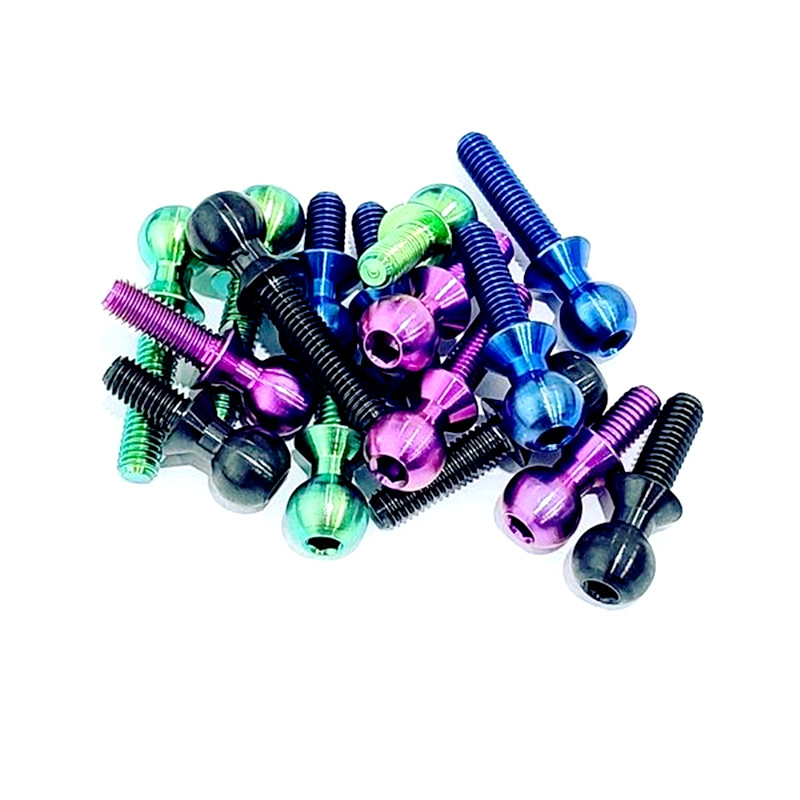
Gr5 M3-M6 RC Racing Precision Ball Studs
Micro-machined suspension ball studs for competitive RC chassis and lightweight mechanical linkages, offering class 10.9/12.9 tensile strength equivalents.
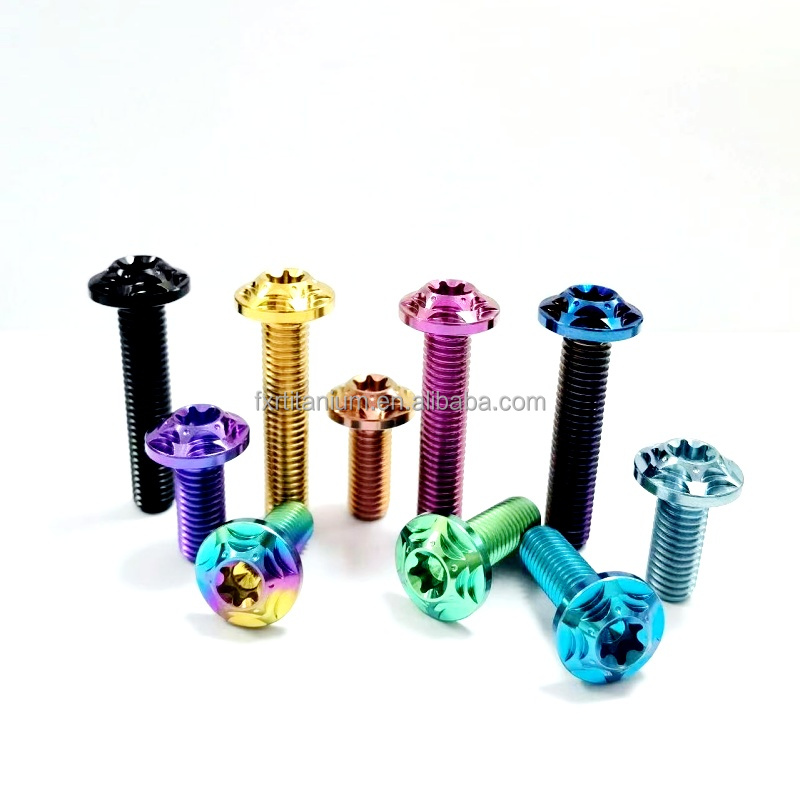
GR5 Fancy Torx CNC Umbrella Head Ti Bolts
Low-profile large umbrella flange head bolts with precision CNC broached Torx drives, reducing contact stress in carbon fiber and aluminum frame mounts.
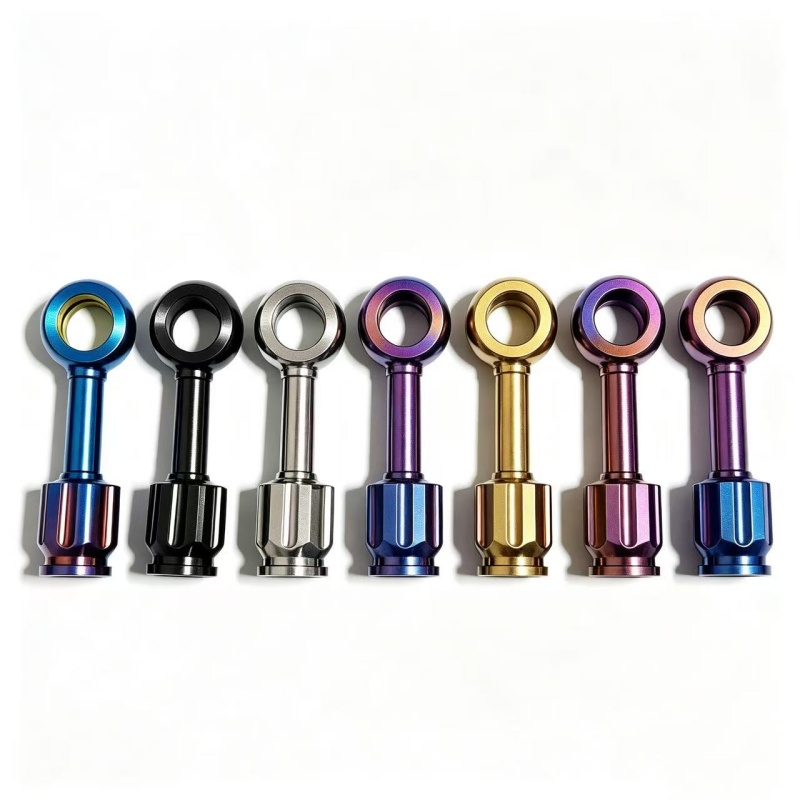
FOXTI AN3 Titanium Hydraulic Brake Line Crimp Connector
Hydraulic hose modification fittings designed to withstand over 3,000 PSI dynamic burst pressures without metal embrittlement or micro-leakage.
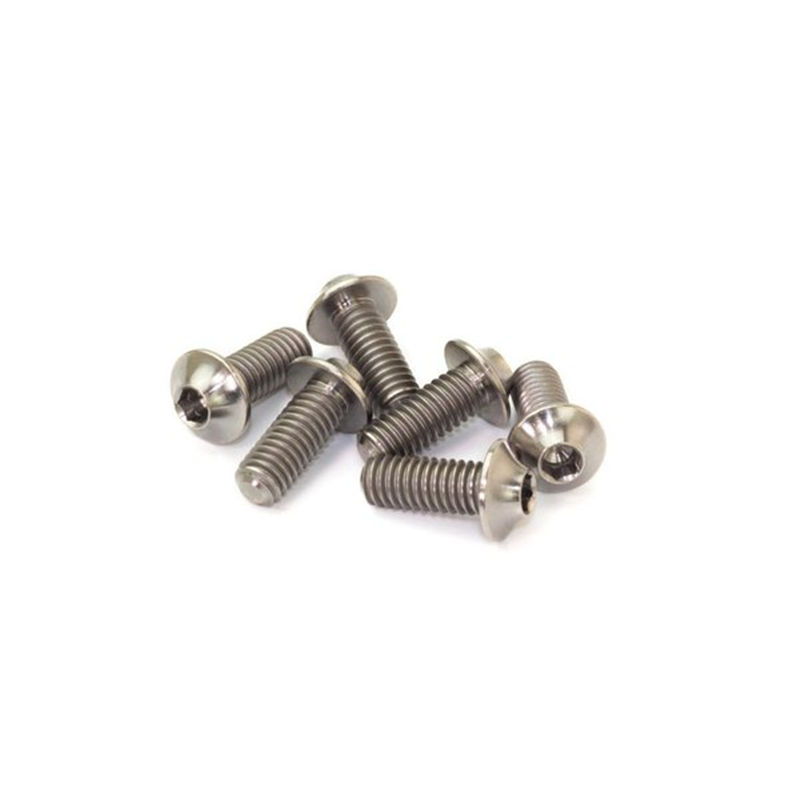
FOXTI LS496 M3 Metric UFO Cone Head Screws
Ultra-thin aerodynamic UFO profile screws for high-stress aerospace models, folding pocket knives, and EDC multi-tool chassis assemblies.
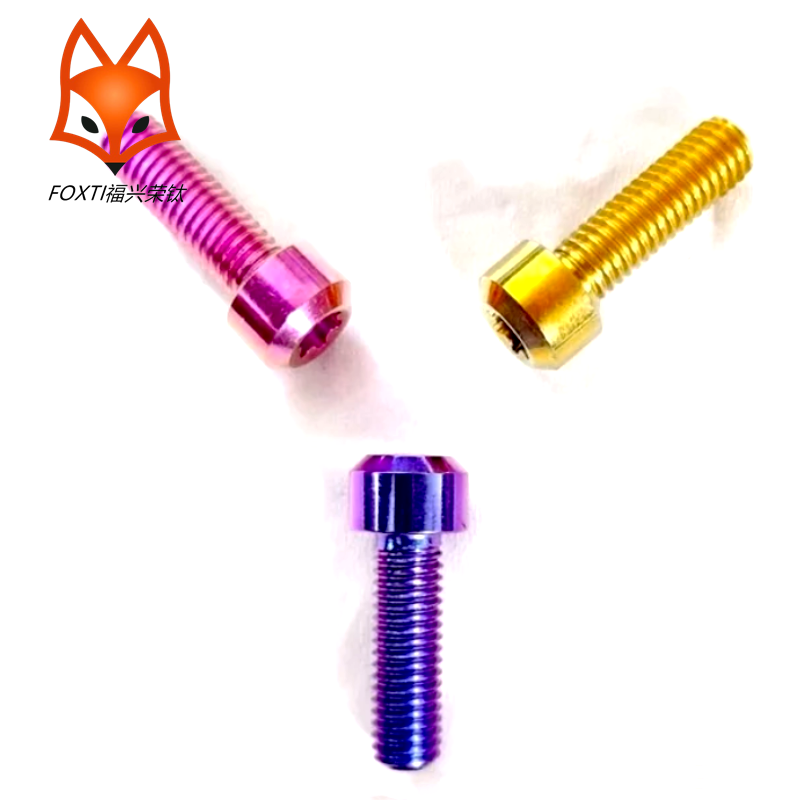
SHSC Small Socket Head GR5 Precision Modification Bolts
Engineered for tight clearance mechanical assemblies, featuring cold-forged hex sockets, tight tolerance shank diameters, and rolled external threads.
Engineering Grade 5 (Ti-6Al-4V) for High-Stress EDC & Tactical Applications
When procuring components for the demanding Everyday Carry (EDC), tactical defense, and precision outdoor sectors, material selection dictates the operational ceiling. Understand the crystalline advantages and mechanical thresholds of our Baoji-melted Grade 5 alpha-beta titanium alloy.
| Alloy Specification | Yield Strength (MPa) | Tensile Strength (MPa) | Density (g/cm³) | Vickers Hardness (HV) | Corrosion Mechanism | Machinability / Tool Wear |
|---|---|---|---|---|---|---|
| Verqo GR5 (Ti-6Al-4V) Annealed | ≥ 828 MPa | 895 – 1000 MPa | 4.43 | 330 – 360 HV | Spontaneous TiO₂ Passive Film | Requires Rigid Carbide Tooling |
| Commercial Pure Gr2 Titanium | ≥ 275 MPa | ≥ 345 MPa | 4.51 | 145 – 180 HV | High chemical resistance | Prone to material work-hardening |
| Austenitic 316L Stainless Steel | ≥ 220 MPa | ≥ 520 MPa | 7.98 | 160 – 190 HV | Susceptible to chloride pitting | Moderate cutting speeds |
| Alloy Steel Grade 10.9 Hardened | ≥ 940 MPa | ≥ 1,040 MPa | 7.85 | 320 – 380 HV | Oxidizes rapidly (requires plating) | High machinability profile |
| Aerospace 7075-T6 Aluminum | ≥ 503 MPa | ≥ 572 MPa | 2.81 | 150 – 160 HV | Subject to galvanic degradation | Fast chip clearance profile |
The Strength-to-Weight Equilibrium
Ti-6Al-4V delivers an extraordinary strength-to-density ratio of 210 kN·m/kg, compared to 125 kN·m/kg for structural steels. In EDC tools—such as pocket pry bars, bit drivers, carabiners, and tactical folding knives—this translates to a massive 43% reduction in payload mass while maintaining structural integrity against shearing, drops, and torque deflection.
Anti-Galling & Tribological Control
Titanium alloys exhibit low thermal conductivity and a relatively high coefficient of friction, which historically made threads prone to micro-friction galling. Verqo solves this challenge through micro-fine thread rolling (rather than single-point cutting) combined with specialized Physical Vapor Deposition (PVD) anti-friction coatings that slash the coefficient of friction down to 0.15.
Permanent Bio-Inert Corrosion Defense
Unlike chrome-plated or electro-galvanized carbon steels that fail after minimal exposure to coastal salt spray or human perspiration, Grade 5 titanium forms an instantaneous, regenerative TiO₂ oxide film when exposed to oxygen. It achieves complete immunity to human body sweat, seawater, and severe industrial solvents—critical for lifelong pocket gear.
Why Global Tier-1 Brands Partner with Verqo in China's Titanium Valley
Headquartered in Baoji, Shaanxi—the epicenter of China's titanium metallurgy producing over 65% of national raw material supply—Verqo bridges raw titanium ingots with ultra-high precision subtractive CNC engineering.
Baoji Supply Cluster
Direct access to primary vacuum-arc remelted (VAR) titanium bar stock. Zero intermediate trading markups, pristine chemical composition verifications, and batch traceability from ingot to final product.
Multi-Axis CNC Fleet
Equipped with Citizen Swiss-type lathes, 5-axis DMG MORI milling centers, and automated thread rolling equipment capable of handling tight dimensions from M2 micro-fasteners up to M26 heavy-duty components.
High-Efficiency Protocol
Dedicated bilingual engineering project managers guarantee RFQ response times under 2 hours. Fast-track rapid prototyping dispatches validated First Article Inspection (FAI) physical samples within 7 business days.
Flexible Scaling & MOQ
We empower both specialized boutique EDC creators and multinational distributors. Stock hardware starts at 10-20 pcs, while custom OEM tool projects scale smoothly from 50 to 100,000+ units with batch-to-batch repeatability.
Titanium EDC & Tactical Gear: Strategic Sourcing Trends (2025–2030)
The international EDC and precision tool markets are shifting from basic novelty items to mission-critical, aerospaced-derived micro-mechanisms. B2B procurement directors must align their supply chain strategies with these evolving macro dynamics.
1. Next-Gen PVD & DLC Vacuum Tribology
Conventional anodizing (which builds color via interference reflection) is increasingly supplemented by Diamond-Like Carbon (DLC) and multi-arc PVD (TiN, AlTiN, CrN). Buyers now demand scratch-resistant, self-lubricating surface hardness exceeding 2,500 HV. This ensures tactical pens, knife pivots, and pry bars withstand pocket abrasive wear against keys and coins without color degradation.
2. Micro-Mechanism & Tritium Integration
Monolithic EDC tools are evolving into intricate mechanical assemblies. Global consumers actively seek out built-in haptic ball detents, magnetic bit retention systems, ceramic bearing integration for ultra-smooth pivots, and precision EDM wire-cut channels engineered for gaseous tritium or glow-resin vials. Micro-tolerance CNC machining is now a mandatory prerequisite for modern suppliers.
3. Near-Net Metal Injection Molding (Ti-MIM)
While 5-axis subtractive milling remains the gold standard for high-end limited production, Titanium Metal Injection Molding (Ti-MIM) using fine spherical powder is gaining traction for high-volume consumer EDC tools. Progressive exporters now provide hybrid workflows: MIM for cost-effective structural blanks followed by CNC contour machining for critical mating interfaces and knurling.
State-of-the-Art Titanium Surface Treatments & Aesthetics
Enhance your product line's market appeal. We operate automated in-house electrochemical anodizing baths and advanced vacuum PVD chambers to provide uniform, high-wear custom cosmetic finishes.
Electrochemical Anodizing
Through tight direct-current voltage regulation (15V to 110V), we alter the microscopic TiO₂ dielectric film thickness without synthetic pigments or binders. Produces brilliant Gold, Royal Blue, Violet, Magenta, and Emerald hues that are chemically stable and completely skin-safe.
PVD Multi-Arc Vacuum Deposition
Targeting superior surface hardness and chemical resistance, our PVD coatings vaporize titanium and chromium targets in an ionized nitrogen atmosphere. Yields ultra-dense Midnight Black, Oil-Slick Rainbow, Champagne Gold, and tactical Matte DLC layers down to 2-4 microns.
Tactile Mechanical Finishes
From industrial bead blasting (using #120 to #220 ceramic beads) and heavy stonewash tumbling (yielding an authentic rugged matte finish that hides daily scratches) to 1,500-grit mirror buffing, we match your design specifications precisely.
From Engineering Drawing to Export Delivery in 5 Rigorous Steps
Our standardized production lifecycle eliminates international sourcing ambiguities, ensuring every custom titanium production batch satisfies strict mechanical tolerances and packaging standards.
Design & DFM Review
Submit 3D CAD files (STEP/IGES/DXF). Our engineers conduct Design for Manufacturability audits to optimize machine toolpaths and cut unit production costs.
Spectrometric Validation
Raw bar stock undergoes optical emission spectrometry testing to verify ASTM B348 chemical compliance before the first cut is made.
Precision Machining
Parts are fabricated on CNC Swiss lathes and multi-axis machining centers with automated thread rolling and secondary deburring.
PVD & Surface Treatment
Ultrasonic degreasing followed by anodization, PVD, or stonewashing. Micro-hardness, adhesion, and coating thickness are checked and verified.
CMM Inspection & Logistics
Full Coordinate Measuring Machine inspection, laser engraving of customer logos, vacuum anti-friction packaging, and expedited global air freight.
Frequently Asked Questions for Titanium Hardware & Tool Importers
Clear, technically accurate answers to the common metallurgical, commercial, and logistical questions encountered when sourcing titanium products from China.
How does Verqo verify that fasteners and tools are genuine Grade 5 (Ti-6Al-4V) instead of cheaper Grade 2?
Commercial Pure Grade 2 titanium possesses less than half the tensile strength (≥345 MPa) of Grade 5 (≥895 MPa) and is significantly cheaper to machine. Every production heat at Verqo is certified with an EN 10204 3.1 Mill Test Report detailing exact aluminum (5.5–6.75%) and vanadium (3.5–4.5%) chemical composition alongside tensile elongation metrics. We welcome third-party inspections via SGS, TÜV, or lab XRF analysis prior to order dispatch.
What is the standard tolerance range for custom CNC-machined titanium EDC tools and components?
Our CNC machining facility routinely holds linear tolerances of ±0.01 mm, with critical pivot pin dimensions, bearing press fits, and internal micro-threads achieving ±0.005 mm on high-precision Citizen Swiss-style lathes. For threaded fasteners, our metric threads conform strictly to ISO 965 6g external / 6H internal standards, and unified imperial threads conform to ANSI/ASME B1.1 Class 2A/3A requirements.
Why is thread rolling superior to single-point CNC thread cutting on titanium fasteners?
Single-point lathe thread turning cuts directly across the alloy's crystalline grain lines, introducing microscopic notch points that lower fatigue thresholds under cyclic mechanical stress. Verqo utilizes hydraulic cold-thread rolling machines to plastically deform the grain structure around the flanks and root radiuses. This process yields continuous, compressed grain lines that boost thread shear fatigue resistance by over 30% while producing smooth, anti-galling root radiuses.
What are your Minimum Order Quantities (MOQs) for custom tactical tools and branded hardware?
For off-the-shelf standard sizes (e.g., DIN912 titanium socket heads, standard Torx rotor bolts, M3 UFO screws), MOQ starts at just 10 to 20 pieces. For custom OEM/ODM EDC pocket tools, tactical beads, and proprietary vehicle parts requiring custom CAM tooling setups, production MOQs typically range between 50 and 100 units. Full-scale mass production orders easily scale into hundreds of thousands of pieces with volume-tiered pricing.
Will electrochemical anodized colors fade over time with continuous daily pocket carry?
Titanium anodization is not a surface paint or chemical dye; it is an optical interference layer formed by an expanded transparent TiO₂ oxide barrier. Normal atmospheric exposure, sunlight, UV radiation, and water will never cause this film to fade. However, aggressive mechanical abrasion from keys or abrasive pocket dust can slowly wear down the micron-thin oxide layer. For heavy-wear contact surfaces, we recommend PVD coatings or stonewashed surfaces that naturally hide contact patina.
What export Incoterms and international payment options do you support?
We regularly execute shipments under EXW, FOB (Shanghai, Ningbo, Shenzhen, Qingdao), CFR, CIF, and DDP (Delivered Duty Paid) terms directly to your distribution center. Payment terms include standard B2B wire transfers (T/T), confirmed irrevocable Letters of Credit (L/C) at sight for large enterprise contracts, and PayPal for rapid sample prototyping orders.
Accelerate Your Titanium Product Pipeline Today
Whether you are engineering a proprietary titanium pocket pry-tool, expanding an aftermarket motorcycle titanium fastener line, or scaling an international tactical gear brand, Verqo provides the metallurgical authority and precision CNC manufacturing capacity you need.