Featured Titanium Hardware & Wheel Stud Components
Manufactured from aerospace-certified Ti-6Al-4V bar stock with rolled M6–M14 threads, tight CNC tolerances (±0.01 mm), and specialized PVD anti-galling finishes engineered for performance hubs.
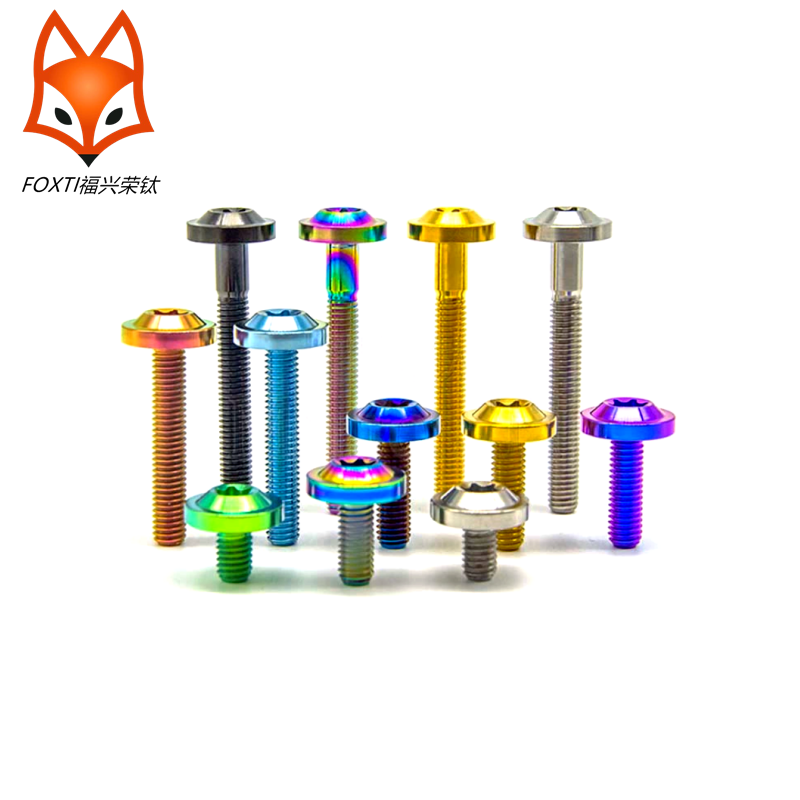
Grade 5 Titanium Alloy Disc Torx Head Anodized PVD Bolt Set M6/M8/M10
FOXTI Gr5 Titanium Alloy Custom Colorful PVD Coated Corrosion Resistant Hardware
Factory Processing Class 10.9 12.9 Shock Absorber Titanium Bolts
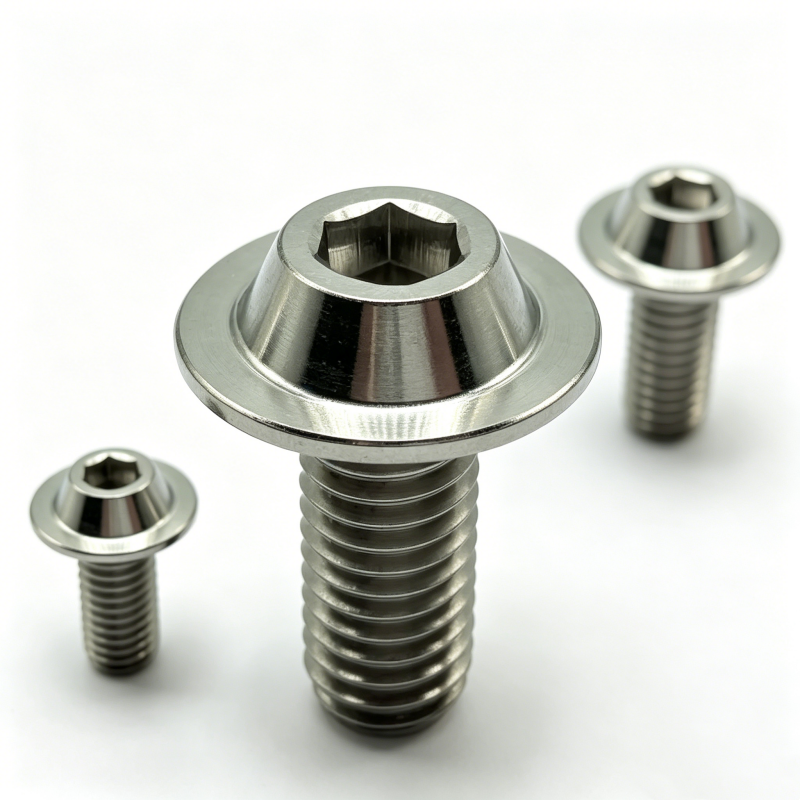
Factory Wholesale GR5 Titanium Screws M4–M10 Hex Socket UFO Head
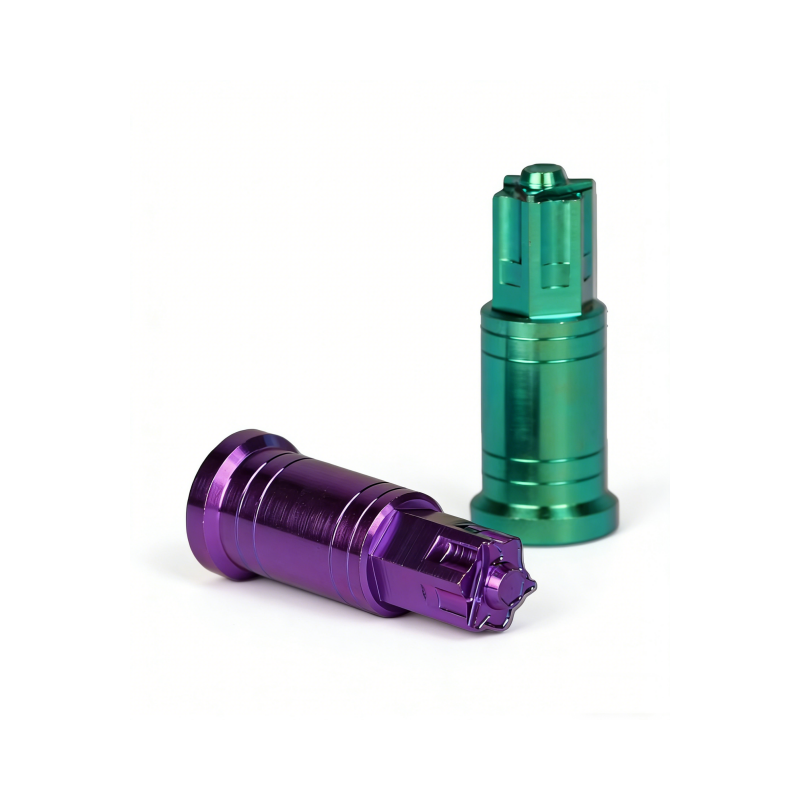
Factory Customized Knurled Extended Titanium Wheel Stud Nut Grade 10.9/12.9
Class 10.9/12.9 Titanium Alloy Bolts Vacuum Coated Ti-6Al-4V
Button Socket Head Titanium Bolts Class 10.9 High-Tensile Assembly
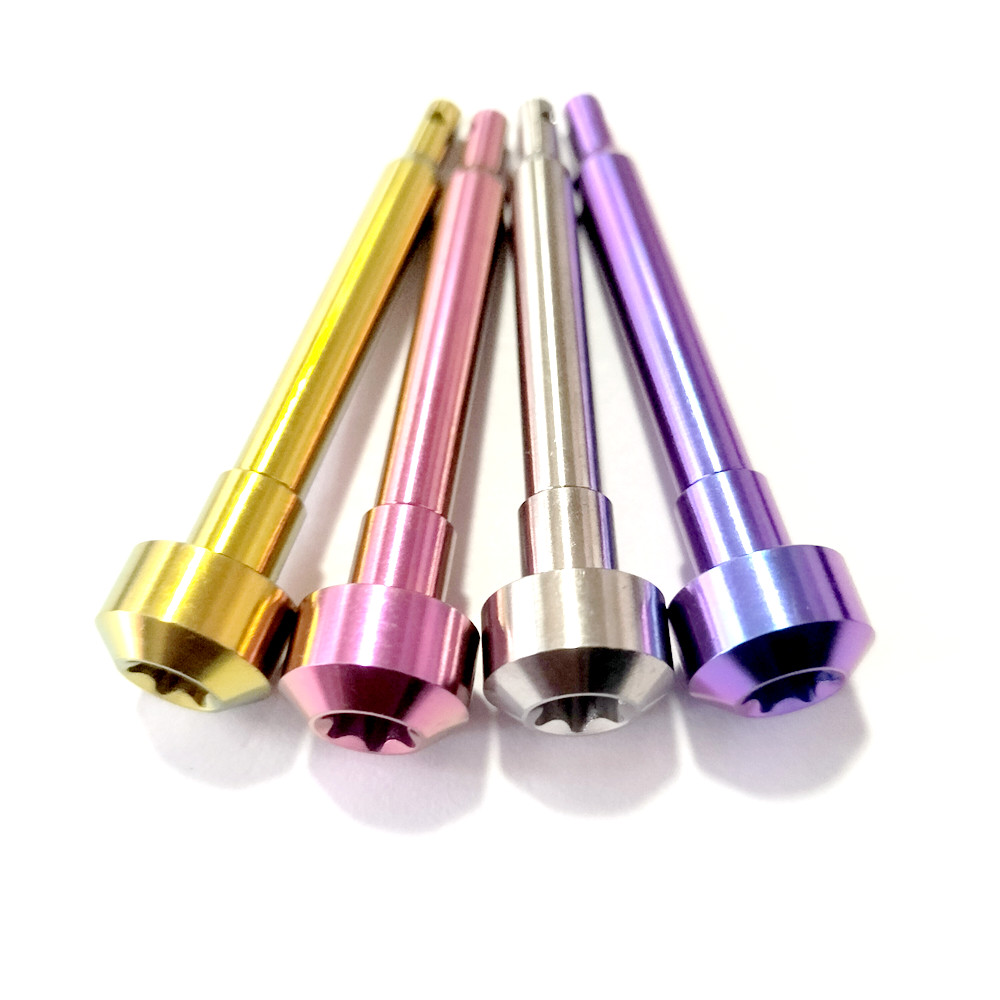
Grade 5 Socket Head M8×20 Motor Race Hardware Titanium Fasteners
1. Industrial Positioning: Titanium Fasteners for the Žilina Automotive Axis
The city of Žilina, nestled along the Váh River valley in northwestern Slovakia, represents the beating mechanical heart of Central Europe's automotive cluster. Anchored by major manufacturing plants such as the massive Kia Slovakia assembly facility in nearby Teplička nad Váhom and Gbeľany, and operating in tight cross-border logistical harmony with Hyundai Motor Manufacturing Czech in Nošovice (less than 80 kilometers to the north), the Žilina region is recognized internationally as an epicenter of automotive powertrain, chassis assembly, and high-precision component design.
Within this dense ecosystem of Tier-1 and Tier-2 component suppliers, specialized motorsport garages, tuning workshops, and engineering laboratories at the University of Žilina (UNIZA), the demand for rotary mass reduction and unsprung chassis optimization has reached an all-time peak. Titanium wheel studs, lug bolts, and hub fastening systems are no longer restricted to multi-million-euro Le Mans prototypes; they have emerged as the standard upgrade pathway for track-focused sports cars, rally vehicles navigating the demanding terrain of the Malá Fatra mountains, and next-generation battery electric vehicle (BEV) prototypes engineered throughout the Trenčín-Žilina-Orava economic corridor.
Rotational Mass & Unsprung Inertia
Every kilogram saved at the wheel hub represents an exponential reduction in gyroscopic resistance. Replacing heavy class 10.9 steel lug studs with Ti-6Al-4V titanium studs reduces wheel hub unsprung weight by approximately 43%, delivering sharper suspension damping reaction across rough Slovak regional roads and higher cornering responsiveness.
Winter Salt & De-Icing Chemical Immunity
Continental winters in Žilina and the Tatra mountain corridors demand extreme road salting and calcium chloride treatments. While zinc-plated carbon steel studs suffer hydrogen embrittlement and catastrophic rust-seizing, Grade 5 titanium forms an instantaneous, self-healing TiO₂ passivation film immune to galvanic degradation.
High-Thermal Braking Integrity
Performance vehicles tackling downhill hill-climbs around Strečno and Martin generate severe disc heat exceeding 650°C. Grade 5 titanium maintains superior tensile yield and thermal resistance compared to standard alloy steels, eliminating heat-soak thread stretching and hub-nut back-off during competitive motorsport stints.
2. Technical Whitepaper: Ti-6Al-4V Grade 5 vs. Standard Fastening Alloys
When evaluating automotive wheel fasteners for high-stress clamping, engineering buyers often mistakenly equate generic "titanium" with strength. In structural applications, commercially pure (CP) titanium grades (such as Grade 1 or Grade 2) lack sufficient tensile and yield properties, making them unsuitable for lug hardware. Our factory strictly utilizes vacuum-arc remelted (VAR) Ti-6Al-4V Grade 5 (UNS R56400 / Werkstoff 3.7165), precision cold-headed or rolled-thread machined under strict aerospace and DIN/ISO metallurgical standards.
| Mechanical / Chemical Parameter | Ti-6Al-4V Grade 5 (Verqo Spec) | Alloy Steel Grade 10.9 (OEM Standard) | Alloy Steel Grade 12.9 (Race Bolt) | CP Grade 2 Titanium (Commercial) |
|---|---|---|---|---|
| Density (g/cm³) | 4.43 g/cm³ (-43% vs Steel) | 7.85 g/cm³ | 7.85 g/cm³ | 4.51 g/cm³ |
| Ultimate Tensile Strength (MPa) | 950 – 1,050 MPa | 1,040 MPa | 1,220 MPa | 345 MPa (Insufficient) |
| Yield Strength 0.2% Offset (MPa) | 880 – 940 MPa | 940 MPa | 1,100 MPa | 275 MPa |
| Modulus of Elasticity (GPa) | 114 GPa (High shock absorption) | 210 GPa | 210 GPa | 105 GPa |
| Thread Manufacturing Method | Precision CNC Thread Rolling | Rolled | Rolled | Cut / Thread Die |
| Chloride & Salt Spray Resistance | > 1,500 Hours (Zero Rust) | Requires Zinc/Dacromet Plating | Subject to Hydrogen Embrittlement | High, but low shear limit |
| Thermal Conductivity (W/m·K) | 6.7 (Thermal barrier to hub) | 43.0 | 42.0 | 16.4 |
The Importance of Rolled Threads: A common failure point in subpar aftermarket wheel studs is thread cut tearing. When threads are machined with standard turning tools, micro-notches disrupt the natural grain boundary flow of the titanium billet, creating severe fatigue hot-spots under cyclic lateral load. Our manufacturing facility utilizes high-tonnage hydraulic thread-rolling dies, compressing the atomic structure into uninterrupted continuous grain paths. This process produces wheel studs with a fatigue resistance over 300% greater than lathe-cut alternatives, providing flawless safety margins along the high-speed curves of Slovakia's D1 and D3 motorways.
3. Emerging Market Trends Across the Žilina & Slovak Automotive Landscape
As the automotive landscape across Slovakia rapidly adapts to European Green Deal directives and the industrial transition to zero-emission battery electric platforms, technical requirements for fastening hardware have undergone a structural paradigm shift. In Žilina, where technical talent and high-speed CNC manufacturing co-exist, three decisive procurement drivers have emerged:
1. Electric Vehicle Weight Mitigation
With electric vehicle chassis carrying battery packs that weigh between 450 kg and 700 kg, vehicle design engineers must hunt for fractional gram savings across rotating components. Shaving 1.5 to 2.2 kilograms of unsprung rotational mass directly from wheel hub studs allows suspension engineers to optimize damper rebound, extend tyre longevity, and recover watt-hours per kilometer.
2. Anti-Galling Physical Vapor Deposition (PVD)
Traditional raw titanium hardware exhibits friction welding (galling) when torqued repeatedly without paste. Slovak tuning shops and rally race teams increasingly specify multi-layer PVD (Physical Vapor Deposition) DLC (Diamond-Like Carbon), TiN Gold, and burnt-blue nano-coatings. These atomic-level coatings drop thread friction coefficients to µ=0.10–0.12, ensuring repeatable clamping torques without stripping.
3. Direct-from-Source OEM Supply Reliability
Rather than relying on third-party European distributors with heavy markups and delayed lead times, automotive aftermarket brand owners and assembly contractors across Žilina and Bratislava are partnering directly with integrated factories rooted in China's Titanium Valley, securing 100% material traceability, custom mill test certificates (EN 10204 3.1), and flexible OEM custom batches.
4. Enterprise Capabilities: Rooted in Baoji, Engineered for the Global Market
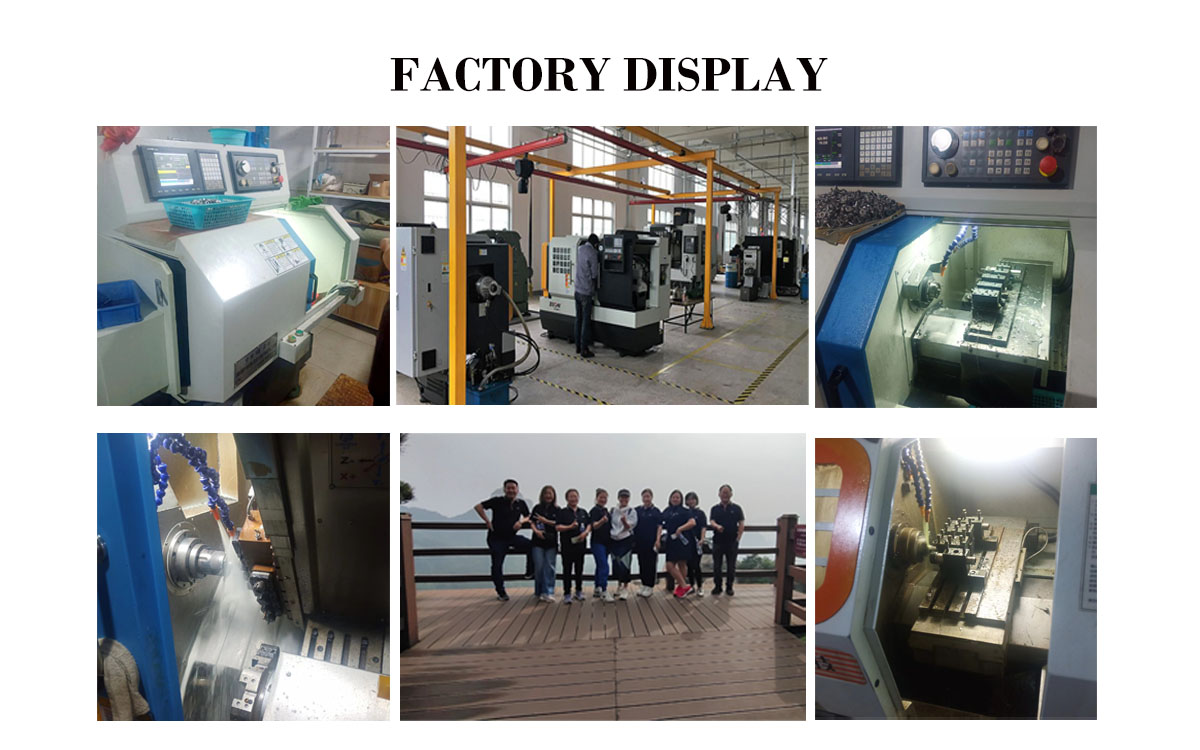
Verqo Titanium Products Co., Ltd. operates from Baoji, Shaanxi Province—internationally celebrated as China's "Titanium Valley" and home to over 80% of the nation's titanium refining capacity. Since 2015, we have bridged the gap between raw aerospace ingot melting and precision high-volume automotive hardware fabrication. Operating over 2,000 square meters of state-of-the-art CNC machine workshops, multi-axis Swiss machining centers, and cold-rolling thread formers, we deliver an end-to-end quality ecosystem verified to ISO 9001 standards.
100% Certified Ti-6Al-4V
Every heat batch is supplied with chemical spectroscopic analysis and mechanical tensile test reports complying with DIN 50049 / EN 10204 3.1 standards.
Rapid Technical Turnaround
Average response time under 2 hours, 98.62% quotation response rate, and direct CAD/CAM engineering collaboration for bespoke thread profiles.
Full Dimensional Scope
Complete tooling coverage from miniature M2 screws up to heavy-duty M26 structural bolts. Pitch variations include M12×1.25, M12×1.5, M14×1.25, and M14×1.5.
Flexible Slovak Logistics
Reliable DDP and DAP shipping channels direct to Žilina, Bratislava, Košice, or Vienna freight hubs, supporting both small prototyping runs and high-volume containerized OEM contracts.
5. Frequently Asked Questions by Slovak Industrial & Automotive Sourcing Teams
Drawing from years of B2B transactions with European distributors, track engineering workshops, and industrial component purchasers, we have compiled key technical clarifications for purchasing titanium wheel studs in the Žilina marketplace:
Grade 5 (Ti-6Al-4V) exhibits an ultimate tensile strength of 950–1,050 MPa and a yield strength exceeding 880 MPa, closely matching the structural clamp performance of Class 10.9 steel (1,040 MPa tensile). However, titanium is approximately 43% lighter (4.43 g/cm³ compared to 7.85 g/cm³) and possesses an elastic modulus of ~114 GPa, allowing it to absorb dynamic impact vibrations without micro-fracturing or fatiguing.
We regularly produce M12×1.25 (common on Italian and Japanese platforms), M12×1.5 (BMW, older VAG), M14×1.25 (modern BMW / Mini), and M14×1.5 (Audi, Volkswagen, Porsche, Skoda, Kia, and Hyundai platforms manufactured in Slovakia and the Czech Republic). Extended shank lengths from 45 mm up to 85 mm are machined to accommodate wheel spacers.
Titanium forms a tenacious oxide film that can cause galling if torqued dry at high speeds against aluminum or steel. We solve this by applying vacuum PVD surface coatings (DLC or Titanium Nitride) to lower the friction coefficient, and we supply each wholesale order with technical anti-seize paste guidelines (such as copper-free molybdenum disulfide or specialized ceramic lubricants) ensuring stable torque retention.
Unlike carbon steel studs which rust, pit, and develop severe corrosion seizing after one or two winter seasons under sodium chloride and calcium chloride highway sprays, Ti-6Al-4V is completely impervious to salt spray corrosion. In 1,500-hour ASTM B117 salt fog testing, Grade 5 titanium exhibits zero pitting, zero weight loss, and zero surface degradation.
For standard stock dimensions (such as standard M14×1.5 bullet-nose conversion studs), our MOQ starts as low as 20 to 50 pieces for prototype testing. For completely custom OEM configurations (including custom knurl diameters, custom hex-drive heads, or proprietary locking patterns), production runs start around 100 to 200 pieces.
We routinely ship to EU destinations under standard Incoterms (DAP, DDP, FOB, CIF). Consignments are accompanied by commercial invoices with exact HS tariff codes (e.g., 8108.90 for finished titanium articles), EN 10204 3.1 material test certificates, and full dimensional inspection sheets. Air freight to Žilina or Vienna averages 5–8 business days, while sea freight takes approximately 28–35 days.