Featured Aerospace-Grade Titanium Fastener Series
Direct from our Baoji manufacturing complex to the Bavarian industrial corridor (Munich, Ingolstadt, Dingolfing, Augsburg), providing high-integrity mechanical components engineered for extreme mechanical demands.
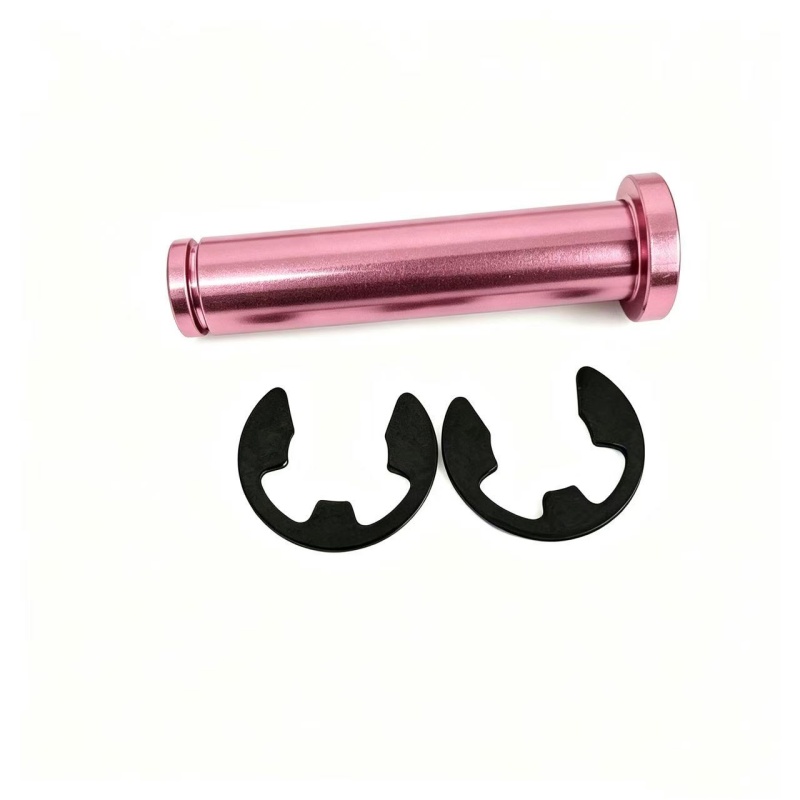
Factory Customized Grade5 Colorful M10*40mm Titanium Foot Peg Pin Bolt
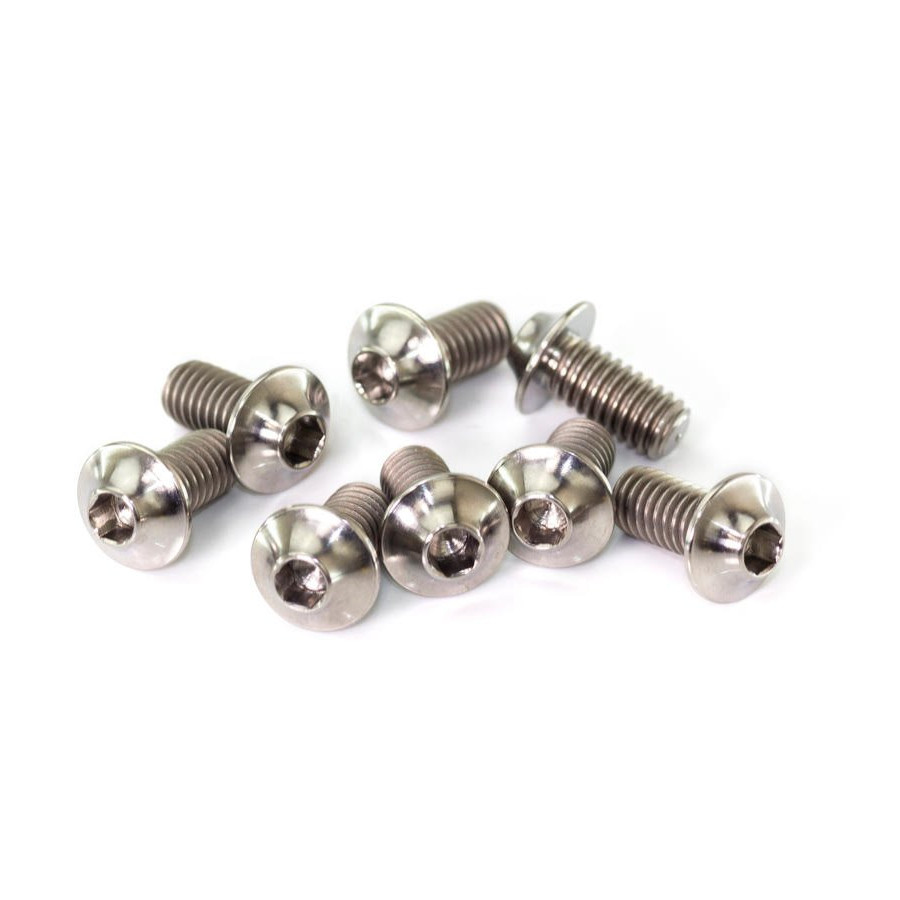
GR5 M3x4/6/8/10/12/15mm UFO Cone Head Metric Screws
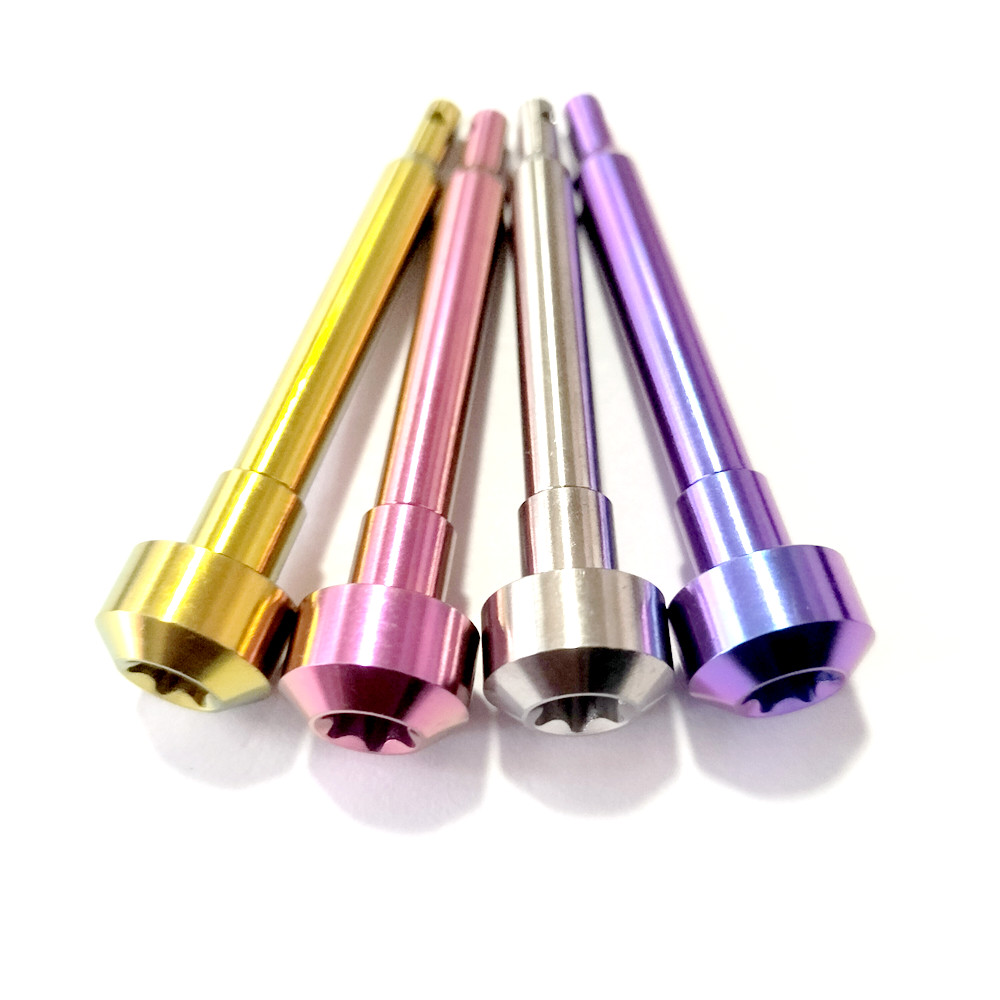
Titanium Alloy Grade 5 Socket Head M8x20 Motor Race Screws PVD
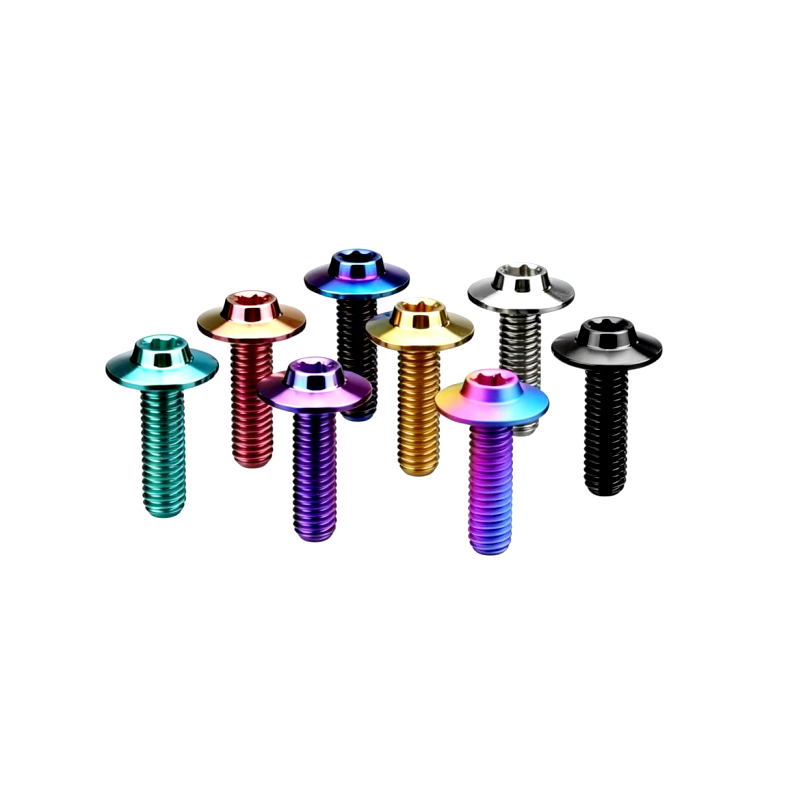
Grade 5 Colorful M6 Umbrella Torx Head Lightweight Bolts
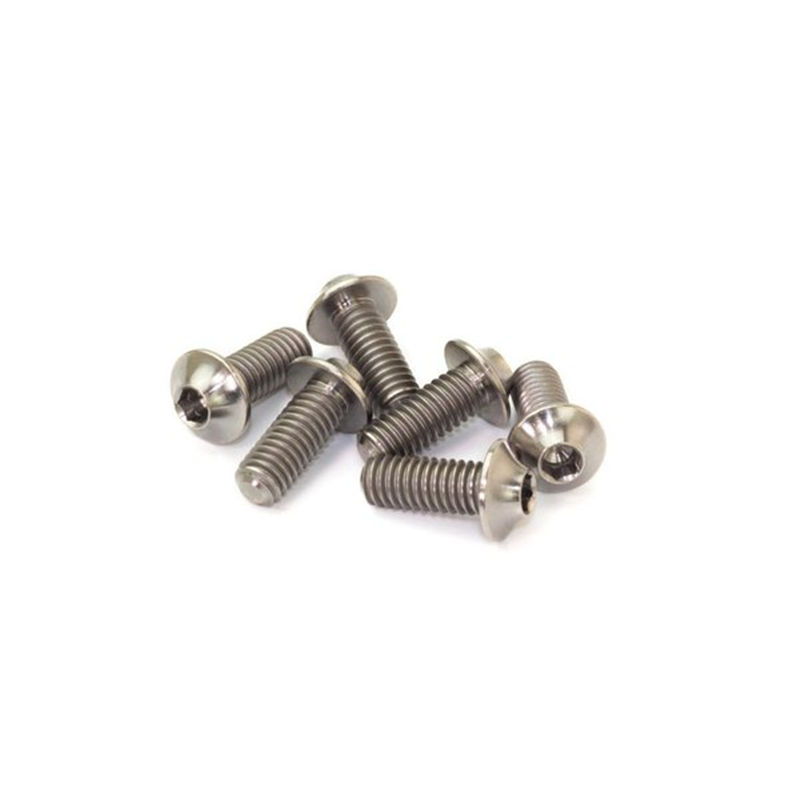
FOXTI LS496 M3 UFO Cone Head Titanium Alloy High-Strength Screws
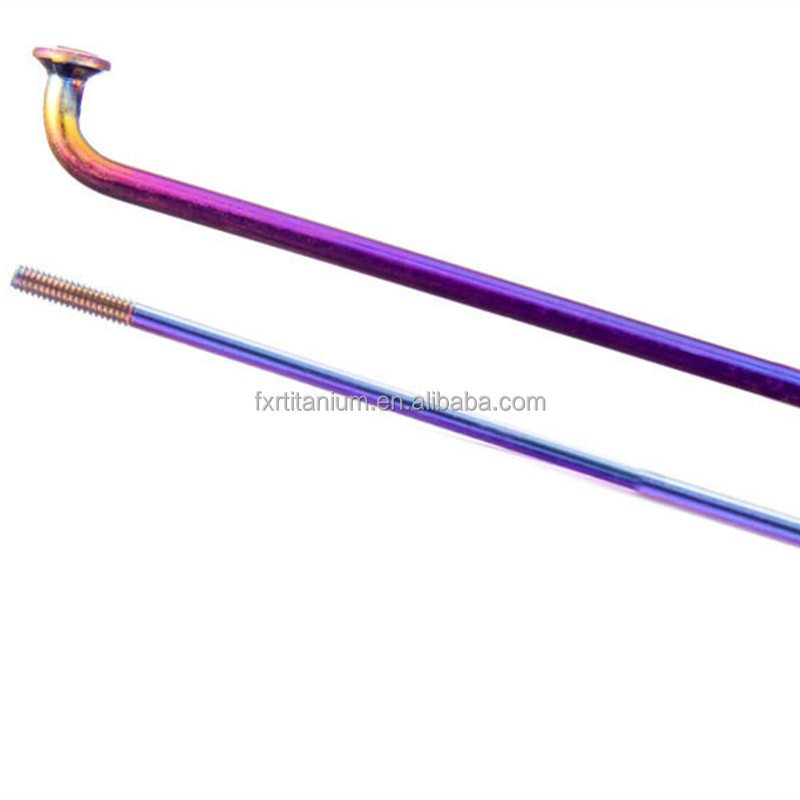
High Quality Gr5 Straight Pull Titanium Bike Wheel Spokes
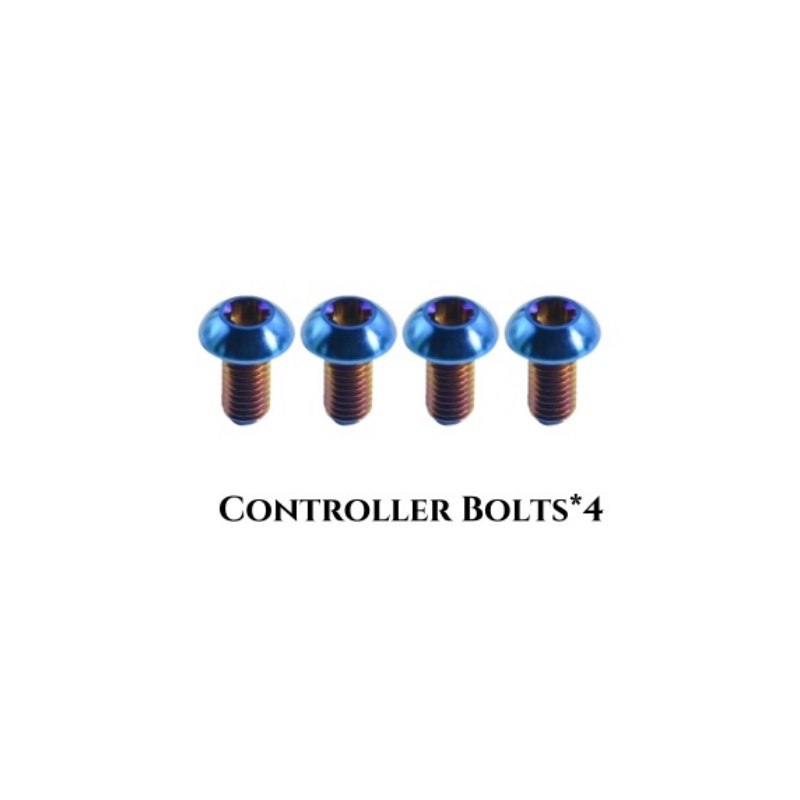
Class 10.9/12.9 Titanium Alloy Controller Bolts Vacuum Coated
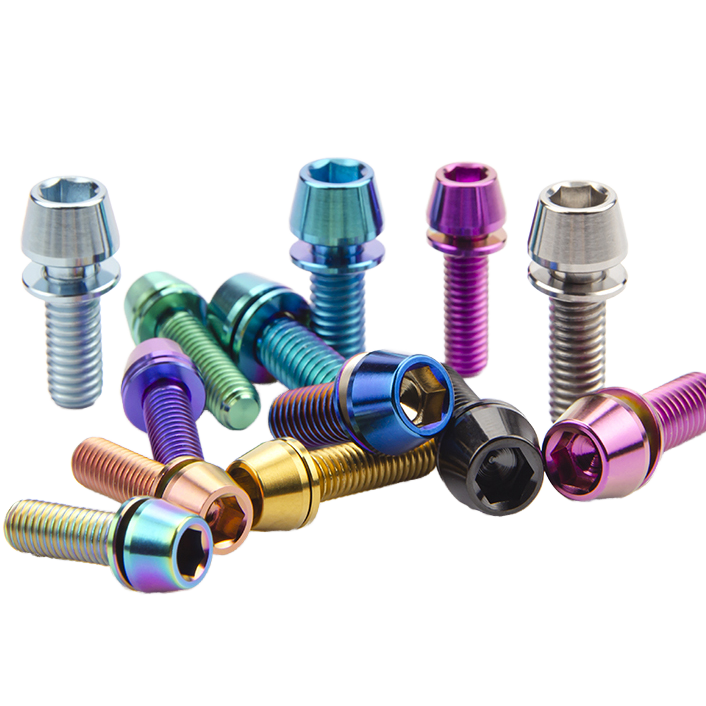
M5/M6 Class 10 Taper Head Anodized Titanium Bolt Screw with Washer
Engineering Tapered Titanium Fasteners for Munich's Advanced Technology Sectors
The industrial landscape of Munich and Upper Bavaria (Oberbayern) represents one of the world's most concentrated ecosystems of automotive engineering excellence, aerospace innovation, and high-performance precision manufacturing. From the R&D centers of major automotive OEMs headquartered in Munich to Tier-1 system suppliers in Garching, Ismaning, and the aerospace clusters in Ottobrunn and Manching, procurement managers operate under strict metallurgical and geometric specifications. As the premier China-based factory and exporter specializing in Ti-6Al-4V (Grade 5, Werkstoff 3.7165) hardware, our production infrastructure in Baoji ("China Titanium Valley") bridges cost-effective mass production with DIN/ISO certified mechanical engineering standards.
Tapered Titanium Bolts (Konische Titanschrauben) represent a vital geometric evolution beyond traditional cylindrical socket head cap screws (DIN 912 / ISO 4762). By integrating a 15° to 30° machined taper from the socket head perimeter toward the flange or shank shoulder, mechanical engineers achieve three distinct structural advantages: substantial rotational mass reduction, superior conical stress redistribution under cyclic shear loads, and minimal aerodynamic and mechanical clearance profiles. For Munich's performance-driven developers, choosing a high-tier Chinese factory with direct cold-forging and multi-axis CNC turn-mill centers eliminates the severe 300% to 500% markups applied by local European stockists while securing comprehensive EN 10204 Type 3.1 chemical and mechanical batch traceability.
Comparative Mechanical Properties: Ti-6Al-4V vs. Traditional German Engineering Alloys
A data-driven engineering evaluation for Munich structural design engineers verifying yield limits, rotational inertia savings, and environmental degradation parameters.
| Property Parameter | Ti-6Al-4V (Grade 5 / W.Nr. 3.7165) | 42CrMo4 (Alloy Steel 10.9 / 1.7225) | A4-70 (AISI 316 / 1.4404 Stainless) | Al 7075-T6 (Duralumin Aerospace) |
|---|---|---|---|---|
| Density (ρ, g/cm³) | 4.43 (43.5% lighter than steel) | 7.85 | 7.95 | 2.81 |
| Tensile Strength (Rm, MPa) | 895 – 1,050 | 1,000 – 1,200 | 700 – 800 | 540 – 570 |
| Yield Strength (Rp0.2, MPa) | ≥ 828 | 900 – 940 | 450 | 480 |
| Specific Strength (Rm/ρ) | 202 – 237 kNm/kg | 127 – 152 kNm/kg | 88 – 100 kNm/kg | 192 – 203 kNm/kg |
| Modulus of Elasticity (E, GPa) | 110 – 114 (Dampens Shock) | 210 | 193 | 72 |
| Corrosion Resistance (VDA 233-102) | Immune to Chloride & Road Salts | Requires Zn-Ni / Dacromet Coating | High (Susceptible to crevice pitting) | Moderate (Intergranular risk) |
| Thread Processing Method | Precision Cold Rolled (DIN 13-6g) | Rolled / Machined | Rolled / Cut | Machined / Rolled |
Note: All values reflect standard vacuum-annealed bar-stock certified per ASTM B348 / AMS 4928 standards utilized in our manufacturing facility.
High-Value Industrial Application Scenarios Across Greater Munich
Automotive R&D & Nürburgring Track Testing
Prototype skunkworks around Munich utilize our tapered Grade 5 titanium bolts for hub carrier assemblies, brake disc rotor pins, and unsprung suspension linkage mounts. Reducing rotating, unsprung mass directly improves damper response frequencies and vehicle steering kinematics over demanding lap profiles.
Alpine Enduro & High-End E-MTB Racing
Bavaria borders the Alps, housing premium boutique bicycle manufacturers and World Cup downhill teams. Our tapered head bolts, featuring cold-rolled Torx T25 drives, resist severe chain tension shock and eliminate galvanic pitting during harsh winter commutes exposed to aggressive Bavarian roadway de-icing brine (Streusalz).
Precision Robotics & Munich Automated Logistics
Automated fulfillment centers and industrial multi-axis articulated robots developed in Augsburg and Munich leverage our low-profile M3 to M6 UFO tapered cone bolts. Their non-magnetic, low-inertia signature prevents electromagnetic interference in proximity sensors and high-speed servo actuators.
Shifting Fastener Supply Chains: The Munich-China Direct Industrial Channel
The manufacturing ecosystem in Southern Germany is undergoing a profound structural evolution characterized by two driving pressures: aggressive lightweighting targets accelerated by electric vehicle (BEV) architectures, and the urgent necessity to optimize Tier-1 supply chain procurement expenditure. German engineers who historically specified DIN 912 Class 10.9 steel are hitting strict vehicle curb weight thresholds dictated by large battery packs. Switching structural battery enclosure bolts, inverter housing fasteners, and motor casing hardware to Grade 5 Titanium achieves immediate double-digit weight reductions without requiring dimensional changes to tapped hole geometries.
Concurrently, German technical purchasing protocols (Technischer Einkauf) are bypassing traditional Hamburg or Frankfurt trading intermediaries. These legacy distributors typically introduce protracted 16-week delivery horizons and 400% inventory markup overheads without adding engineering value. By establishing direct contracts with our facility in Baoji, Shaanxi, Munich-based manufacturing firms access dedicated CNC production cells, batch-specific optical sorting, customized head geometry stamping, and air-freight logistics directly connecting Xi'an (XIY) to Munich Airport (Franz Josef Strauss - MUC) in under 7 business days.
Precision Chinese Engineering Backed by Strict German Quality Standards
Headquartered in Baoji's world-renowned titanium industrial belt, our manufacturing facilities integrate metallurgy, micro-machining, and robotic surface engineering.
Certified Vacuum Melting & Bar Stock
Every fastener originates from premium virgin titanium sponge double- or triple-melted in vacuum arc remelting (VAR) furnaces. We ensure zero interstitial gas embrittlement with strict chemical compliance certified under ASTM B348, AMS 4928, and ISO 5832-3.
Cold Forging & Thread Rolling
Unlike cut threads that interrupt the grain structure of titanium, our M2 to M26 threads are precision cold-rolled using carbide dies. This process forms continuous longitudinal grain alignment, yielding a 30% increase in fatigue threshold and superior resistance to cyclic notch stresses.
Advanced PVD & Anodic Surface Cells
From Physical Vapor Deposition (PVD) titanium nitride (Gold), titanium carbonitride (DLC Black), to customized multi-spectrum interference anodizing (Rainbow, Burnt Blue, Violet), our coatings provide Vickers micro-hardness ratings reaching HV 2,200+, preventing friction gauling.
High-Speed Swiss CNC Lathe Fleet
Equipped with 5-axis Citizen and Star CNC sliding-head Swiss machines, we execute complex tapered cone profiles, internal Torx/Hex sockets, safety-wire cross drill holes, and weight-relief center bores in a single clamping setup, assuring runout within ≤ 0.005 mm.
100% Automated Optical Sorting
To support high-speed robotic assembly lines operated by German industrial partners, our facility implements multi-camera laser optical inspection sorting. Bolts are verified at 800 parts per minute for thread pitch, head concentricity, and total length, ensuring near-zero PPM defect rates.
Direct EU Customs Clearance & Rapid Logistics
We provide full export documentation under HS Code 8108.90, including EUR.1 / Certificate of Origin, clean commercial invoices, and automated customs clearance protocols delivering DDP shipments directly to corporate gates in Munich, Dachau, and Starnberg.
Munich Engineering Procurement Questions & Detailed Technical Answers
1. What material test certificates accompany shipments to German industrial facilities?
Every production batch shipped to Munich is delivered with a comprehensive EN 10204 Type 3.1 Inspection Certificate issued by an independent ISO/IEC 17025 accredited laboratory. This documentation details complete spectrometer chemical heat analysis (Fe, C, N, H, O, Al, V, Ti balance) and mechanical testing results (Tensile Strength Rm, Yield Strength Rp0.2, Elongation at Fracture A, and Reduction of Area Z), guaranteeing full structural validation against DIN and ASTM requirements.
2. How do your engineers mitigate thread galling (Fressneigung) during torque assembly?
Titanium exhibits a natural tendency toward micro-frictional adhesion (galling) when torqued dry against mating titanium, aluminum, or stainless threads. We resolve this by offering factory-applied dry-film anti-friction coatings (MoS2 or graphite) and specialized PVD treatments. Furthermore, we provide our Munich clients with precise VDI 2230 tightening torque calculation sheets, recommending high-grade nickel or copper-based anti-seize pastes with friction coefficients calibrated to μ = 0.10 – 0.12.
3. What are the lead times and shipping options for manufacturing clients in Upper Bavaria?
For standard stocked dimensions (e.g., DIN 912 tapered M5, M6, M8 in 15mm to 40mm lengths), warehouse dispatch occurs within 24 to 48 hours. Custom CNC or forged production according to client 2D/3D CAD drawings (STEP/DWG) typically requires 15 to 22 business days for manufacturing and PVD finishing. Fast-track air freight delivers from our facility directly to Munich Airport (MUC) via DHL Express or FedEx Priority within 4 to 6 business days, complete with automated German customs clearance.
4. Can you manufacture custom tapered head geometries according to proprietary factory drawings?
Yes. Over 60% of our production for European clients involves bespoke OEM/ODM manufacturing. Whether you require DIN 912 modified conical profiles, deep Torx T-Drive internal broaching, reduced-shank necking for weight reduction, or safety-wire flange drill-holes for racing regulation compliance, our engineering department reviews your STEP/IGES files and provides DFM (Design for Manufacturability) analysis within 2 hours.
5. What are your Minimum Order Quantities (MOQ) and sample prototyping protocols?
We maintain an agile, flexible manufacturing posture designed to support Munich engineering consultancies and R&D laboratories during their pilot phases. Standard catalog fasteners have an MOQ of only 10 to 20 pieces. For custom CNC machined components, initial prototype test batches start at 50 to 100 units. Full-scale series production contracts can scale smoothly into tens of thousands of units with phased batch releases.
6. What thread tolerance classes do you hold for mission-critical assemblies?
Our cold-rolled threads adhere strictly to ISO 965-2 Class 6g external thread tolerances as standard, ensuring interchangeable fit with DIN 13 standard internal metric tapped holes. For specialized aerospace or motorsport powertrain projects requiring ultra-tight back-lash tolerance, our precision CNC thread rolling cells can produce Class 4h6h specifications upon customer request.
Accelerate Your Engineering Project with Certified Titanium Fasteners
Connect directly with our senior fastener engineers. Request our complete 2025 technical catalog, CAD dimensional models, and obtain an itemized DDP quote delivered directly to your Munich facility within 2 hours.
Get Catalog